Target Keywords: small appliance 8D report; small appliance CAPA process; small appliance failure analysis; small appliance reliability growth; small appliance quality dashboard; small appliance supplier quality agreement; small appliance batch release criteria
Direct answer: A buyer should use a supplier quality agreement to turn defects, field signals, inspection findings, and verification evidence into explicit release decisions. Require a configuration-specific 8D record for material issues, a closed-loop CAPA workflow, a modest dashboard of trendable measures, and pre-agreed batch-release gates. Release should be based on the final build, destination market, traceability, evidence quality, and unresolved risk—not on a supplier’s assurance that a correction is complete.
A polished pilot run can conceal the governance problem that appears after the first complaint, a component substitution, or a repeat failure. The question is not whether a supplier can produce an 8D document on request. It is whether the buyer and supplier have agreed what starts an investigation, who contains affected stock, which evidence proves a correction, and who may authorize shipment when information is incomplete.
This guide is about ongoing quality-agreement and batch-release governance. It deliberately does not repeat the separate work of approving a development sample; buyers can use the golden-sample-to-mass-production protocol for that earlier milestone. The controls below begin with the production configuration and continue through lot disposition, corrective action, and learning across later lots.
1. Define the decision boundary before writing the agreement
A small appliance supplier quality agreement is a commercial operating document, not a substitute for the purchase order, technical file, laboratory assessment, or applicable law. Its purpose is to make routine decisions reproducible when parties face ambiguity: a display intermittently fails, a charger changes revision, an inspection sample has a functional defect, or retailer returns begin to cluster.
Start with a product-and-market boundary sheet. Identify the exact model and revision; voltage, plug, and charger variants; destination countries; supplied accessories; packaging; intended user and foreseeable use; serial, lot, or date-code format; and the brand entity that will make market decisions. Do not describe a family of “similar” appliances as one controlled product. A change that appears cosmetic can affect instructions, electromagnetic compatibility, materials, electrical safety, or the evidence associated with the final configuration.
IEC 60335-1 addresses general safety requirements for household and similar appliances; product-specific parts and national differences may also matter [4]. It is not automatic approval for every appliance or market. For EU products, GPSR requires an internal risk analysis and technical documentation before placing products on the market [3].
| Agreement question | Buyer should settle | Useful controlled record | Avoid |
|---|---|---|---|
| What is the product? | Approved BOM, drawing, firmware, artwork, packaging, variant matrix | Revision register and signed configuration baseline | Calling a catalogue image the specification |
| What counts as a lot? | Production period, order, traceability range, rework treatment | Lot definition and unique lot ID | Mixing units with different material or firmware histories |
| Who decides? | Supplier quality, buyer quality, engineering, regulatory owner, logistics owner | RACI and escalation contacts | “Quality team” without a named decision right |
| What proves conformance? | Inspection, functional checks, documents, records, approved deviations | Release checklist with evidence links | Treating a test report as proof of every future build |
| What happens if it fails? | Hold, segregation, rework approval, notification, 8D/CAPA, disposition | Nonconformance and containment workflow | Shipping first and investigating later |
State that applicability is assessed for the final configuration and destination market, with supporting evidence and qualified review where necessary. An earlier sample or another market’s evidence need not cover an altered build.
2. Translate requirements into measurable release gates
Turn the approved configuration into a release-control plan: feature, method, sampling or verification approach, owner, record, decision, and response to failure. Decide which controls need every-unit or every-lot attention rather than a pre-shipment sample alone.
Gates combine documentary checks, process records, product checks, and risk assessment. ISO 2859-1:2026 defines AQL-indexed sampling for inspection by attributes, but the plan must fit the product, defect classification, lot structure, and risk; it does not prove every unit defect-free [2].
| Gate | Evidence to review | Decision owner | Example release outcome |
|---|---|---|---|
| Configuration readiness | Current BOM, drawings, artwork, firmware, approved change status | Buyer engineering/quality | Do not start or do not release until version is reconciled |
| Incoming and in-process control | Key-component records, process checks, operator records, rework log | Supplier quality | Escalate if a critical component or control is unverified |
| Finished-goods verification | Functional, cosmetic, labeling, packaging, and safety-related checks against the plan | Supplier plus buyer/independent inspector as agreed | Accept, hold, or inspect further under the agreed rule |
| Documentation readiness | Certificates or declarations where applicable, test evidence, traceability, manuals, shipping documents | Brand regulatory/quality owner | Hold market-specific shipment if evidence is missing or mismatched |
| Open-risk review | Deviations, 8D/CAPA state, repeat-failure signal, containment status | Named release authority | Release only with documented rationale, or quarantine/stop shipment |
Write the actual small appliance batch release criteria in the agreement. They might say that critical nonconformities require a hold; that a major trend triggers a buyer review even if a sample acceptance number is met; that unapproved component or firmware changes block release; and that a documented concession has an expiry and scope. The exact criteria are commercial and risk-based choices, not universal thresholds to copy from a checklist.
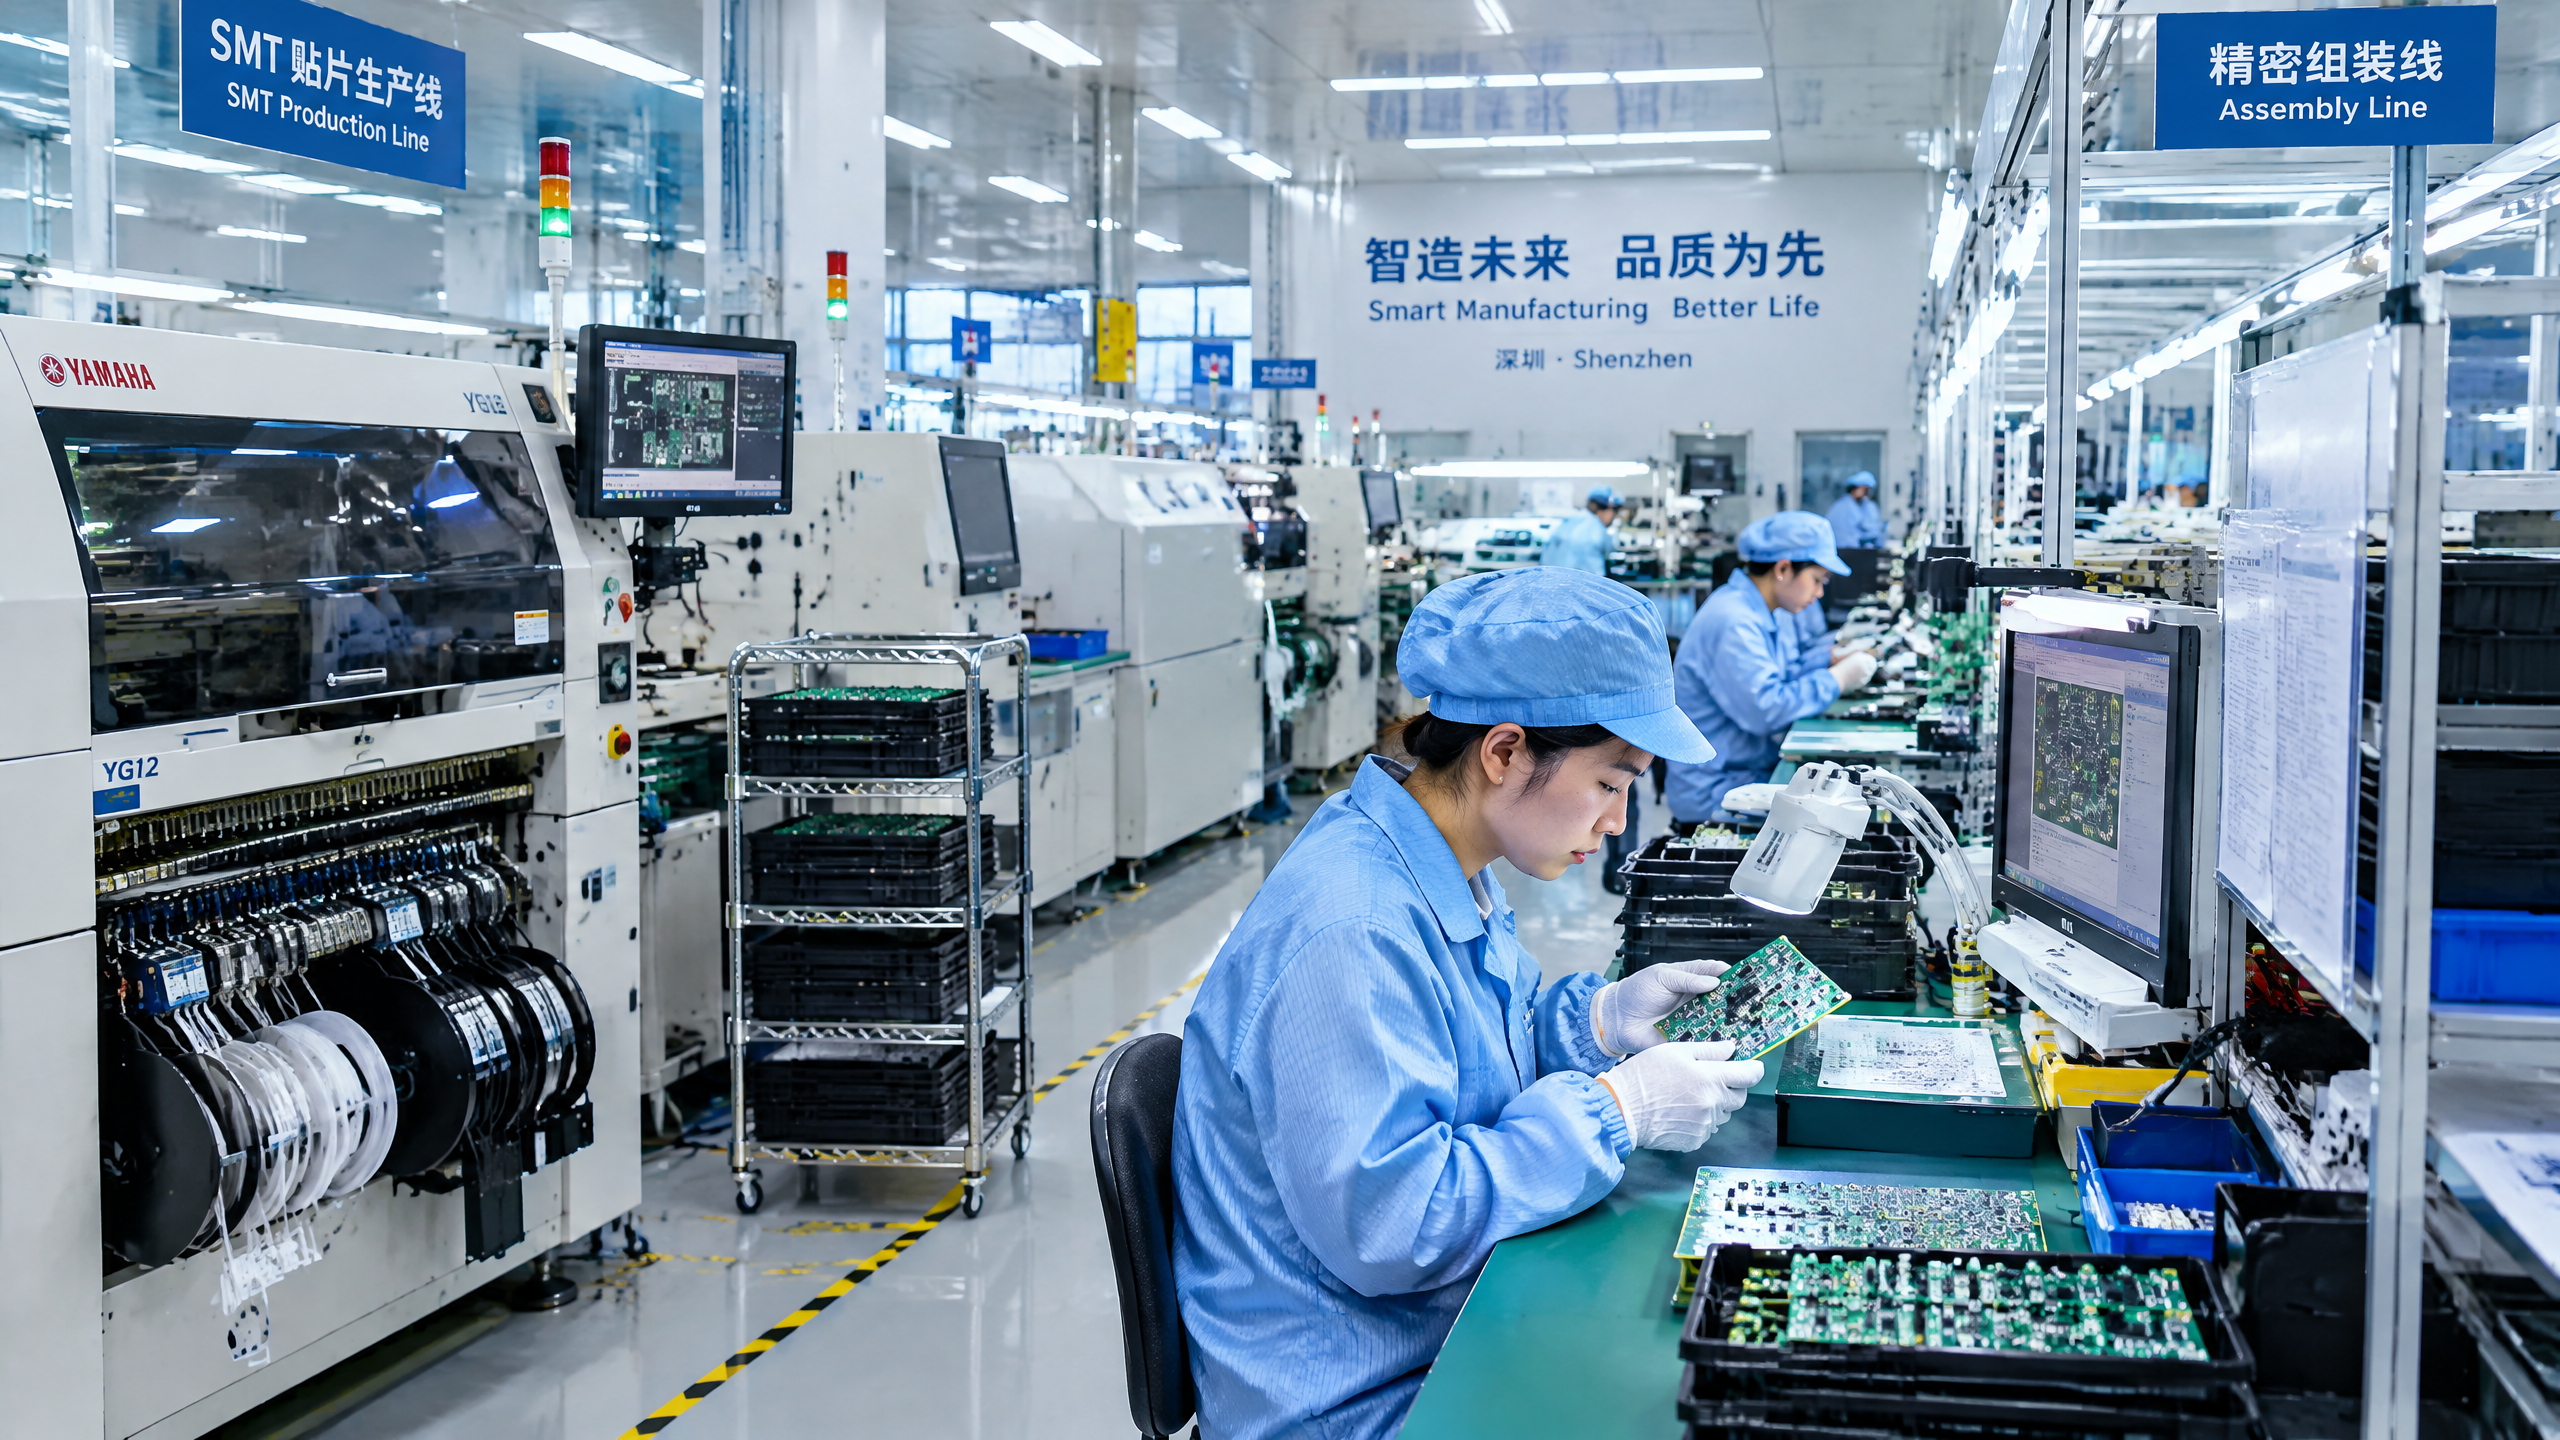
For a view of the production setting and control topics that sit behind those gates, review UZYVO’s factory capabilities. The buyer still needs to verify the proposed controls against its own product, destination, and agreement.
3. Make the 8D report an evidence trail, not a formality
A small appliance 8D report is most valuable when it gives the batch-release team a time-bound, auditable answer to four questions: What happened? Which units are exposed? What stopped the exposure now? What evidence will show that recurrence is less likely? “8D” is a structured problem-solving convention, not itself a product certification, legal conclusion, or substitute for independently evaluating a safety concern.
Use the disciplines as a controlled narrative: team, observable problem, verified containment, root and escape causes, corrective action, validation, recurrence prevention, and closure. Attach evidence—such as traceability queries, measurements, process records, test method, and revision history—rather than merely summarizing it.
| 8D element | Release-relevant question | Minimum useful evidence | Weak practice to challenge |
|---|---|---|---|
| Problem description | Which configuration, lot, symptom, rate, and market are involved? | Model/revision, lot IDs, observation method, dates | “Poor quality found” |
| Containment | Which stock is stopped, identified, rechecked, or recovered? | Quantity reconciliation, hold locations, segregation photos/records | “Operator reminded to be careful” |
| Root and escape cause | Why was the defect created and why did controls miss it? | Hypothesis testing, process path, control-record review | Naming an operator without testing the process |
| Corrective action | What changes in the design, process, supplier control, or check? | Revised work instruction/control plan, owner, effective date | Adding 100% inspection indefinitely without cause analysis |
| Effectiveness | What proves the change works across an appropriate period or lots? | Defined criterion, follow-up records, trend comparison | Closing because a replacement part was installed |
Set triggers in advance. A safety concern, suspected substitution, traceability gap, repeat defect, document mismatch, or customer escape may warrant urgent containment; an isolated cosmetic observation may enter a trend log. Define notification route and timing without inventing unachievable promises.
Do not accept “root cause: bad material” without material identity, supplier lot, incoming-control result, and a reason the material passed into production. Likewise, “operator error” is incomplete if the work instruction, fixture, training record, work pace, or detection method contributed. The release authority needs causal evidence proportional to the risk, not an eloquent slide deck.
4. Build a CAPA process that distinguishes correction from prevention
A small appliance CAPA process should connect nonconformance handling to a controlled decision on whether product can move. Correction fixes a discovered unit or immediate condition. Corrective action addresses the cause of a nonconformity to prevent recurrence. Preventive thinking also means using trends, change reviews, and risk analysis before a defect becomes a shipment escape. Calling every repair a CAPA masks whether the system has learned anything.
ISO 9001:2026 covers process operation, performance evaluation, and improvement; certification can add confidence but is not mandatory [1]. Request process-specific evidence rather than treating a certificate as closure for a product or lot.
Structure the record so each action has an owner, due date, affected configuration, risk rationale, validation method, and status. Tie it to the unique lot and release decision. A useful closed-loop record shows whether the action was implemented, whether its result was evaluated, and what happens if the criterion is not met.
| State | Meaning | Release posture | Required next move |
|---|---|---|---|
| Open / triage | Signal logged; scope not yet confirmed | Do not infer acceptance from lack of information | Obtain configuration, lot, and exposure facts |
| Contained | Immediate exposure controls are in place | Shipment may remain held or be conditionally reviewed | Reconcile all affected inventory and evidence |
| Action implemented | Process or design change deployed | Not automatically effective | Validate against the stated criterion |
| Effectiveness verified | Evidence supports the intended result within defined scope | Eligible for closure if residual risk is accepted | Update controls, training, and dashboard |
| Reopened / escalated | New evidence contradicts the closure | Reassess impacted lots and claims | Restore hold or expand investigation as needed |
Preserve change control. If an action changes a source, resin grade, protective device, power supply, firmware, or process, assess whether prior evidence remains applicable. For EU electrical and electronic equipment, RoHS requires attention to series-production conformity and relevant changes [5]. Obtain qualified review before conformity claims.
5. Run failure analysis as a bounded technical investigation
Small appliance failure analysis should explain the observed failure mode and its scope; it should not turn one returned unit into an unsupported general claim. Start by preserving the condition of the sample, collecting chain-of-custody information where relevant, confirming configuration and date code, and comparing the reported use with the approved instructions. Record what is known, unknown, and assumed.
Use a staged method: safely characterize the symptom; compare it with a known configuration; review visual and non-destructive observations; check traceability; and involve suitable specialists when needed. Preserve information before destructive examination. Distinguish observation, mechanism hypothesis, and evidence-supported cause.
| Investigation area | Questions to ask | Evidence that can support a decision |
|---|---|---|
| Identity and history | Is this the approved variant? Which lot, process date, component lots, rework, and destination? | Photos of markings, records, BOM/revision, traceability query |
| Symptom and use | What did the user observe, under which conditions, and how was it verified? | Complaint narrative, controlled observation record, safe reproduction plan |
| Exposure | What else shares the same configuration, component, process window, or shipment? | Lot genealogy and inventory reconciliation |
| Cause and escape | What created the condition, and why did controls not prevent or detect it? | Process records, test/measurement review, hypothesis results |
| Remedy | What immediate and systemic actions reduce the defined risk? | Containment proof, revised controls, action validation plan |
Avoid unsupported forensic language. “No fault found” only means the defined examination did not establish a fault; it does not prove safety, misuse, or irrelevance. A passed bench check may not recreate use. Escalate a potential safety concern or existing-product risk under the agreement and seek market-specific advice.
EU product-safety rules illustrate why traceability and documentation must be usable. The GPSR states that technical documentation should reflect an internal risk analysis, the product description, and, where appropriate, risk mitigation and relevant test outcomes [3]. That is a discipline for evidence and review, not permission to apply a conclusion from one model to another.
6. Treat reliability growth as learning, not a performance promise
Small appliance reliability growth is the managed reduction of known failure modes across controlled iterations. It is not a promise that a product will never fail, and it should never be presented as a numerical reliability claim unless the test design, sample basis, conditions, confidence treatment, configuration, and claim approval actually support one.
Build a failure-mode register from design review, pilot observations, production checks, service returns, and CAPA/8D records. Rank items by safety relevance, exposure, detectability, and uncertainty; then select a suitable verification activity. Define method and acceptance criteria for the exact product and intended use—not a competitor’s brochure.
| Reliability-growth input | What it can reveal | Governance output |
|---|---|---|
| Pilot/build issues | Assembly sensitivity or immature instructions | Updated work instructions, fixture review, next-build verification |
| Incoming component changes | New failure mechanisms or evidence gaps | Change-impact review and requalification decision |
| Finished-goods checks | Detectable functional or cosmetic escapes | Control-plan adjustment and lot disposition |
| Service/return patterns | Possible recurring customer experience issue | Exposure assessment, investigation trigger, customer-service coding |
| 8D/CAPA effectiveness data | Whether actions remain effective across later lots | Closure, reopening, or elevated release controls |
Use clear terminology. A verification activity may support a decision within its stated scope; it does not establish lifetime, abuse resistance, certification, or market conformity beyond that scope. For household appliance safety, identify the applicable standard parts, national deviations, and evaluation route for the destination rather than announcing that “IEC tested” means universally compliant. IEC/IECEE itself advises verifying national-difference status with the relevant member body or national certification body [4].
Reliability learning should feed design and sourcing, not only inspection. A repeated subassembly issue may call for a revised specification, assembly control, supplier qualification, or diagnostic instructions; the right action depends on confirmed cause and final configuration.
7. Design a dashboard that leads to decisions
A small appliance quality dashboard must help a named person decide what to release, investigate, or improve. It should not be a dense scorecard that rewards green status. Use a stable definition for every measure: numerator, denominator, time period, configuration, market, data owner, source system, exclusions, and review cadence. Without those fields, apparent changes can be caused by a new inspection rule or missing return data rather than real improvement.
Keep the dashboard compact and drillable. Separate leading indicators—open critical CAPAs, overdue containment, unapproved changes, missing traceability—from lagging inspection defects or coded returns. Show counts with meaningful rates and do not equate products, lots, or markets with different exposure periods.
| Dashboard view | Possible decision question | Data-quality caution |
|---|---|---|
| Lot-release readiness | Are required records complete for this lot and variant? | Do not mark complete when a document covers a different revision |
| Defect-mode trend | Is a specific failure or escape recurring? | Preserve the defect definition across periods |
| CAPA aging and effectiveness | Which actions are overdue or lack verification? | Closure date is not effectiveness evidence |
| Change-control status | Has any unapproved or unassessed change reached production? | Link to BOM and supplier-revision identity |
| Field/return signal | Does a coded symptom warrant scope assessment? | Normalize carefully for sell-through, market, and reporting delay |
| Supplier-control health | Are key checks, training, or measurement records missing? | A completed form does not establish an effective process |
Review cadence should fit risk. Include buyer and supplier quality, engineering, market owner, operations, and service as appropriate. Every flag must point to action: request evidence, contain, open an 8D, revise a control, assess lots, or document residual-risk acceptance.
Do not use an aggregate supplier “quality score” as the sole release criterion. It can conceal a critical configuration mismatch beneath good results elsewhere. The most important dashboard feature is traceability from the red indicator to the affected unit, lot, action owner, and decision record.
8. Set escalation, deviation, and release authority
Set the hierarchy before a pressure event. Let the supplier stop, identify, and segregate suspect product; name a brand authority for deviations, residual commercial risk, or holds. Keep regulatory conclusions with qualified owners; a factory signature is not a destination-market determination.
Consider a deviation only when scope and evidence are adequate. Name affected configuration and lots, requirement and departure, risk and disposition, quantity/location, expiry, and approvals. It is not a silent replacement for configuration control.
| Event | Immediate agreement response | Release question |
|---|---|---|
| Critical safety-related observation or credible complaint | Stop/shield affected stock, notify named contacts, preserve evidence, assess scope | Can any related product move before risk and scope are evaluated? |
| Unapproved component, supplier, process, or firmware change | Place relevant lots on hold and reconcile affected build records | Does existing evidence still apply to the exact new configuration? |
| Major inspection nonconformance | Segregate, verify extent, open investigation as agreed | Does further inspection or rework have an approved, validated basis? |
| Repeat failure after CAPA closure | Reopen CAPA/8D, assess prior effective-date lots | Was effectiveness testing adequate, or was the cause incomplete? |
| Missing documentation or traceability | Hold the market-specific release and retrieve/verify records | Is there adequate evidence to identify and support the lot? |
For certain U.S. general-use products subject to CPSC rules, a General Certificate of Conformity may be required and is based on testing or a reasonable testing program [7]. Applicability depends on the product and rule; this guide is not a legal conclusion.
For EU routes covered by specified harmonisation legislation, Regulation (EU) 2019/1020 describes duties of an EU-established economic operator, including verifying documentation where required, making documentation available to market-surveillance authorities, and cooperating on corrective action [6]. Those obligations make a practical case for accessible configuration and lot records, but applicability must be checked against the final product and legislation.
Mid-article CTA: Need an agreement-to-release workflow aligned to a specific appliance configuration and destination? Email UZYVO’s B2B team with the model, target markets, current controls, and the decision you need to make.
9. Use visual communication without overstating proof
Visual aids can align teams but must not be presented as a factory record, laboratory result, certification, or proof of a control. Label diagrams as process aids and keep images generic unless their context is verified.
Contextual AI image recommendations
| Insertion point and purpose | English caption | ALT text | English AI image prompt |
|---|---|---|---|
| After Module 2; clarify how configuration, evidence, and release gates connect | “Configuration-specific evidence flows into a documented batch-release decision.” | “Diagram showing controlled appliance configuration, quality records, review gates, and release decision.” | “Clean editorial B2B infographic, horizontal flow: approved appliance configuration, production records, inspection evidence, open-risk review, then release or hold; neutral navy and warm gray palette, no logos, no performance metrics, readable English labels, white background.” |
| After Module 4; explain CAPA status without implying a real plant’s result | “CAPA moves from containment to effectiveness verification before closure.” | “Circular quality-management diagram showing containment, root-cause analysis, corrective action, validation, and control-plan update.” | “Professional technical illustration for a small-appliance buyer guide, circular CAPA workflow with containment, evidence review, cause analysis, action implementation, effectiveness verification, and updated controls; no brand names, no certification marks, no numerical claims.” |
| After Module 7; help teams design a decision-oriented dashboard | “A useful dashboard links an alert to its lot, evidence, owner, and next action.” | “Conceptual quality dashboard with lot status, open actions, change control, and traceability links.” | “Realistic but clearly conceptual B2B quality dashboard on a laptop beside an unbranded countertop appliance and traceability tags; show generic charts and status fields, no readable proprietary data, no claims of actual factory performance, clean industrial office setting.” |
Retain the prompt, label the asset illustrative, have the technical owner check terminology, and never insert unsubstantiated compliance symbols or test values.
10. Use these buyer questions to test the agreement
A buyer should test the agreement in a tabletop exercise: a return arrives from a destination market, the product’s date code points to two shipments, a component supplier recently changed tooling, and the scheduled vessel cut-off is near. Ask each function to produce the record it owns and decide whether product moves. The exercise reveals missing authority, inaccessible data, and informal exceptions before they occur under commercial pressure.
Buyer checklist
- Is the product baseline dated, revision-controlled, and linked to each variant and market?
- Does every lot have a defined identity and a traceable relationship to key components, production records, and shipment?
- Are defect categories, inspection methods, acceptance rules, and escalation triggers documented rather than presumed?
- Does the 8D template require containment scope, root and escape cause, validation, effectiveness evidence, and named ownership?
- Can the CAPA record distinguish a correction from a systemic action and show when a closed action must reopen?
- Does the reliability plan name failure modes, methods, conditions, configuration, acceptance criteria, and limits of interpretation?
- Does the dashboard identify a data owner and action for every red or overdue status?
- Are changes to components, firmware, process, labeling, packaging, or instructions assessed before release?
- Are market documents and claims reviewed for the final configuration and destination—not inherited blindly from another product?
- Are deviations limited by lot, quantity, rationale, approval, and expiry?
Buyer FAQs
Does an ISO 9001 certificate mean the supplier’s batches can be released without additional evidence? No. ISO 9001 is a quality-management-system standard and certification may give additional confidence in the system, but it does not establish the conformance of a particular appliance configuration, lot, destination-market file, or open CAPA [1]. Review the agreement’s gate evidence and the actual records.
When should a buyer require a small appliance 8D report instead of an ordinary defect notice? Set the trigger in advance. An 8D is generally useful for significant, recurring, safety-relevant, customer-escaping, or unexplained issues where containment, causal analysis, and effectiveness verification are necessary. A minor isolated issue may only need a logged correction, unless trend or risk changes its significance. The categorisation should follow the agreement and qualified risk assessment.
Can AQL acceptance sampling release a lot with no further review? No. ISO 2859-1 is an acceptance-sampling system for inspection by attributes; it helps define a sampling decision, not a guarantee that every unit is defect-free or that configuration, documents, safety evidence, and open risks are acceptable [2]. Use it as one input in the release gates.
What closes a CAPA? Closure should require more than completing an action. The record should show the defined cause, implementation evidence, an agreed effectiveness check, results within the stated scope, updated controls where needed, and authorized acceptance of any residual risk. New contradictory evidence should reopen the issue.
Who may approve shipment when a document is incomplete? The agreement should name a release authority and an escalation path. Incomplete documentation may be a reason to hold the market-specific release; no generic answer can replace an assessment of the final product, evidence, destination market, and applicable obligations. The commercial desire to ship is not evidence that the gap is acceptable.
11. Conclude with a controlled release discipline
A defensible batch-release decision is a chain: an identified configuration, a traceable lot, planned controls, accessible evidence, a visible account of unresolved issues, and someone with authority to decide. The supplier quality agreement makes that chain repeatable. It should specify how a small appliance 8D report supplies containment and causal evidence, how CAPA changes the system rather than merely repairs a unit, how reliability learning is bounded by its method and configuration, and how the dashboard directs action.
Avoid making the agreement a pile of templates. Start with the risks that could change release: configuration drift, poor traceability, unverified corrective action, missing market evidence, or a recurring failure mode. Define the record, owner, threshold or decision logic, and escalation for each. Then test the arrangement against a realistic scenario and revise it before the next lot. This produces a clearer commercial conversation than vague promises of “zero defects” or blanket approval.
The final decision must remain specific to the product configuration, destination market, supporting evidence, and qualified review where necessary. Good governance does not guarantee an outcome; it ensures that uncertainty is visible, contained, and decided by the right people before it becomes a customer problem.
Closing CTA: To discuss a configuration-specific supplier quality agreement, dashboard, or batch-release evidence map for your private-label appliance program, contact UZYVO by email.
References
- International Organization for Standardization (ISO), [ISO 9001:2026—Quality management systems](
- International Organization for Standardization (ISO), [ISO 2859-1:2026—Sampling procedures for inspection by attributes](
- European Union, [Regulation (EU) 2023/988 on general product safety (GPSR)](
- IECEE, [IEC 60335-1:2020—Household and similar electrical appliances: Safety, Part 1](
- European Union, [Directive 2011/65/EU on the restriction of hazardous substances in electrical and electronic equipment (RoHS)](
- European Union, [Regulation (EU) 2019/1020 on market surveillance and compliance of products](
- U.S. Consumer Product Safety Commission, [General Certificate of Conformity](
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com