Target Keywords: small appliance in process inspection; small appliance final random inspection; small appliance functional test plan; small appliance reliability test plan; small appliance burn in test; small appliance endurance testing; small appliance life cycle testing
Direct answer: A credible validation plan connects the final appliance configuration, intended use and destination-market obligations to a controlled sequence of incoming, in-process, functional, final-inspection and reliability activities. It names the unit and revision under test, method, equipment, sample rationale, acceptance criterion, evidence owner and action after a failure. It does not treat a passed sample, a generic factory checklist or a voluntary certificate as proof that every production lot or market configuration is compliant.
A buyer needs more than a “QC report.” The task is to decide what is controlled in assembly, verified on completed units, sampled before shipment and challenged over time.
This guide addresses that architecture rather than golden-sample approval. The golden sample-to-mass-production protocol covers sample approval and production changes. Here, focus begins with the released configuration: test-plan construction, evidence and reliability learning. Applicability depends on the final bill of materials, tooling, software, mains supply, accessories, claims, packaging and destination market. Qualified review should confirm applicable requirements.
1. Start with a validation charter, not a generic inspection sheet
A validation charter is the short governing document that prevents a supplier’s routine checklist from becoming the whole quality strategy. It identifies the exact SKU or variant, drawing and firmware revisions, rated electrical input, destination market, intended operating modes, accessories, packaging version and the buyer’s critical-to-quality characteristics. It should also identify the people who can approve a changed test method, component or acceptance criterion.
Begin with the buyer-facing promise, then translate it into observable risks. A variable-speed blender may need controls, interlocks, seal integrity, motor operation and loaded-use behavior considered. A heating product may need its temperature-control behavior, accessible-area and cord-routing risks considered. This is a planning exercise, not a declaration that a particular product passes any safety requirement. The applicable product-specific standard, test conditions and final construction determine what is required.
For many household electrical appliances, IEC 60335-1 is the general safety standard within the IECEE system; relevant particular parts and national differences may also matter.[1] In the EU, the Low Voltage Directive covers electrical equipment within stated voltage limits and includes household appliances, while the applicable route must be assessed for the actual product.[2] An electronically controlled product may also call for consideration of electromagnetic compatibility: the EU EMC Directive addresses both emissions and immunity when equipment is used as intended.[3]
| Charter field | Buyer question | Useful evidence |
|---|---|---|
| Configuration baseline | What precisely is being tested and sold? | Controlled BOM, drawings, firmware identifier, photos and label artwork |
| Market/use profile | Where and how will this variant be placed on the market? | Destination list, mains assumptions, user instructions and claim list |
| Risk priority | Which failures could affect safety, function, presentation or shipment release? | Risk register with rationale and owner |
| Test governance | Who releases methods and resolves a failure? | Revision-controlled plan and escalation matrix |
| Evidence package | What must exist before the lot decision? | Report index, raw-data location, nonconformance record and disposition |
Do not copy another brand’s limits merely because the appliance category looks similar. A different heater, power cord, plastics grade, controller setting, accessory or supply voltage can change the relevant assessment. The charter is the place to make those dependencies visible before the line begins.
2. Map each risk to the correct test stage
Testing works best as a layered system. Incoming checks look for material or component variation before it enters the line. In-process controls prevent a known defect from traveling into the next operation. Final functional checks establish whether a completed unit performs the defined released functions. Pre-shipment sampling assesses a finished lot against an agreed method. Reliability work deliberately exercises time, cycles, load or environmental conditions to learn whether the design and process remain robust.
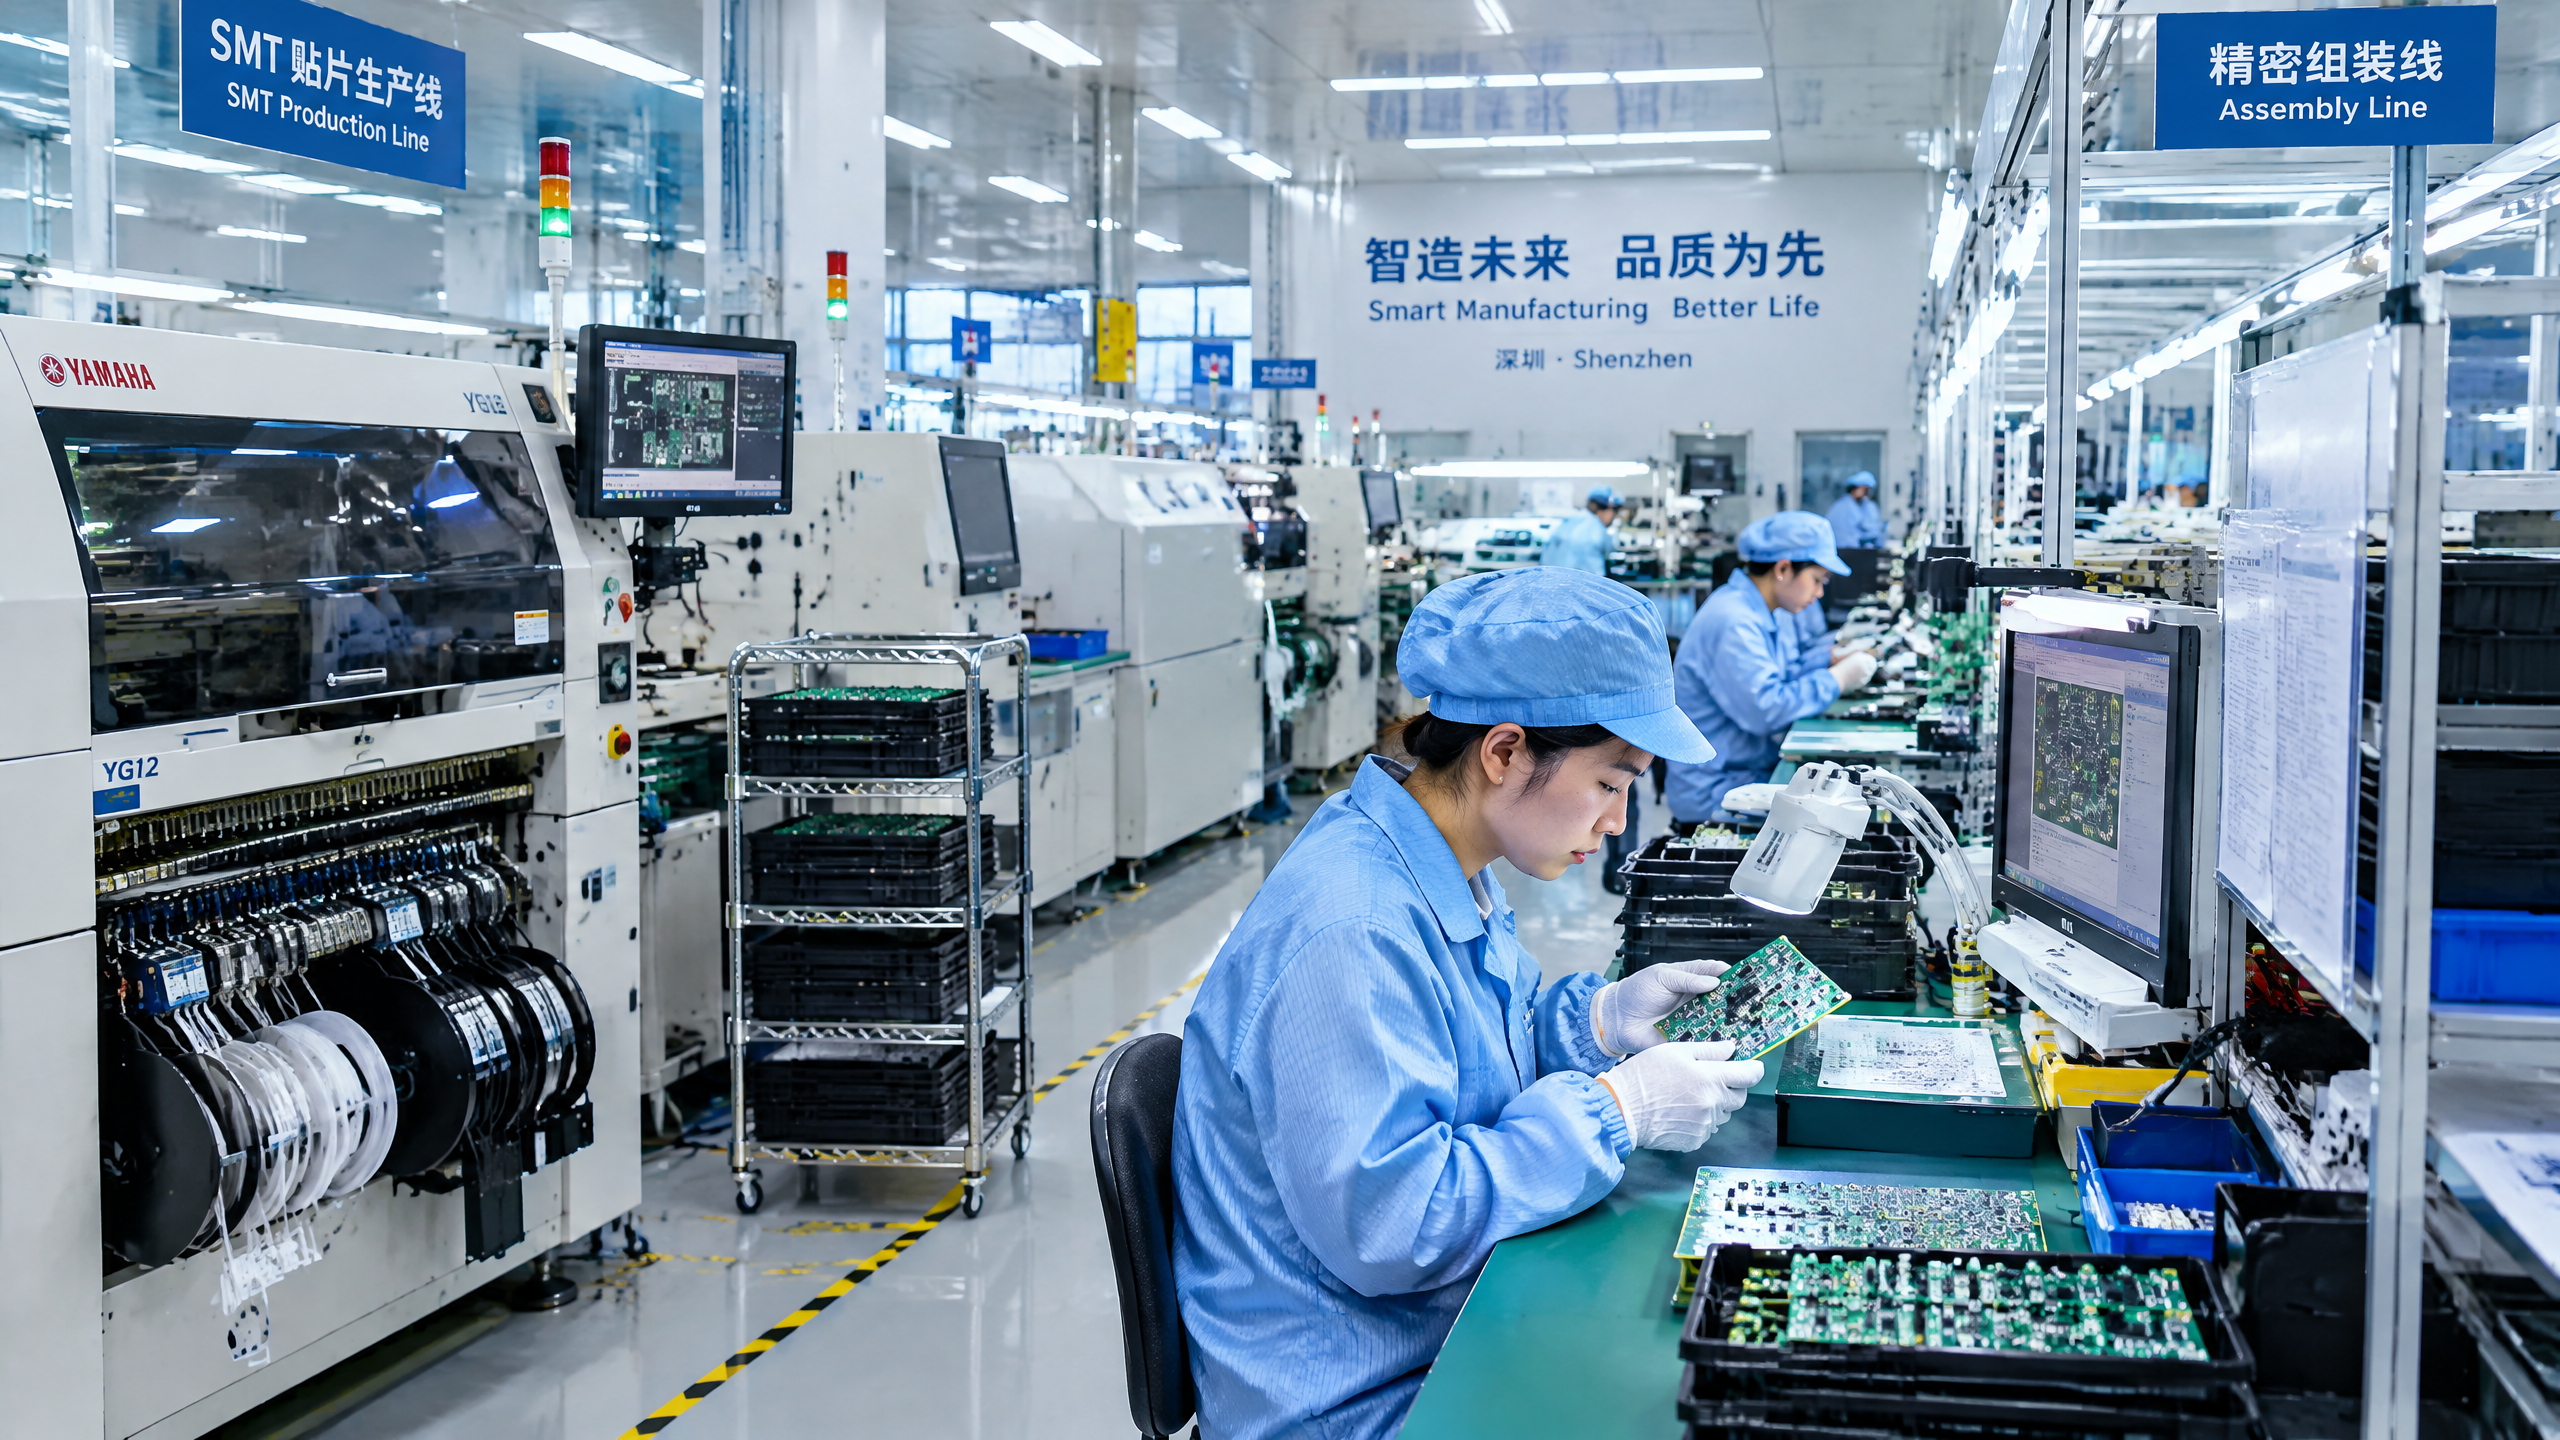
A small appliance in process inspection therefore should not be a single inspection station with a broad label. Divide it by process step and defect mechanism. For example, a wiring operation can have a routing/termination confirmation, a heater assembly can have the specified presence and orientation verification, and a control-board operation can have version and connector checks. The plan should state whether the check is 100%, sampled, automated, operator-performed or independently audited—and why that choice fits the risk.
| Stage | Primary question | Examples of controlled observations | What it cannot establish alone |
|---|---|---|---|
| Incoming | Is the received material the released item and condition? | Part identity, supplier lot, dimensions or appearance as specified | Long-term behavior of the assembled appliance |
| In process | Was a risk-sensitive operation completed correctly? | Fastener presence, wire routing, gasket placement, firmware identity | Overall market conformity or final user experience |
| Completed-unit function | Does this unit execute its released state sequence? | Controls, indicators, modes, shutoff logic, abnormal response as specified | Durability across many cycles |
| Finished-lot sampling | Does the lot meet the agreed defect classification and sample plan? | Cosmetic, labeling, packaging and selected functional observations | A guarantee that uninspected units have no defects |
| Reliability activity | Does the selected build expose weaknesses under defined use/cycling? | Cycles, operating intervals, load profile and failure logging | A legal approval or universal lifespan claim |
This map stops a common mistake: using an end-of-line result to excuse absent process control. A unit that powers on may still contain an incorrectly routed wire, incomplete fastener application or unrecorded software change. Equally, a visually clean product may fail a function only under a defined condition. The plan needs both prevention and detection.
3. Design the in-process control plan around failure mechanisms
The operational core of a small appliance functional test plan is not just the final test bench. It is the process control plan that links a work instruction to a defect risk, an observable condition and a response. Ask the manufacturer to walk the proposed line in process order and identify where an error can be prevented, detected or contained. That walkthrough should include rework loops, temporary storage and operator handoffs, not just nominal assembly.
For each control point, define the “unit of control.” It might be an individual appliance, a subassembly, a shift, a machine setup or a component lot. Then define the traceable reference: a barcode, work order, component lot, software version or test record. Traceability does not have to mean a complex digital system, but it must be sufficient to identify the affected population if a trend or failure is found.
Typical checkpoints may include:
- Released-material identity: confirmation that the actual cord set, thermal device, motor, PCB or plastic resin is the approved item, rather than a visually similar substitute.
- Error-proofed assembly: a fixture, sensor, torque/angle record or other control only where it is genuinely suitable for the operation; never assume an automated signal is meaningful without verifying its setup and response.
- Safety-relevant build features: documented checks for elements whose placement or attachment contributes to the assessed construction, using the applicable technical file and method.
- Software/parameter control: a meaningful firmware identifier, authorized release source and record of the version loaded; a control-value change can make earlier evidence inapplicable.
- Containment after a fault: clear segregation, retest rules, repair authorization and traceability for all units exposed to a suspect station or component lot.
Test equipment is part of the process. The record should name the fixture, instrument or programmed tester; its software/method version; setup verification; maintenance/calibration status; and the result associated with the product identifier. NIST explains metrological traceability as a documented unbroken calibration chain that includes measurement uncertainty, and notes that calibration alone does not guarantee fitness for a particular purpose.[5] In practical buyer terms, request evidence that the measurement system is suitable for the decision—not only a sticker on an instrument.
4. Separate safety assessment from production screening
Buyers often see insulation, protective-earth continuity, leakage-related or dielectric checks listed on a production form. These can be important production controls when selected and performed under an appropriate method, but they are not interchangeable with the full evaluation of the final product configuration by the applicable requirements. The test points, sequence, voltage, duration, conditions and limits should come from the identified standard, laboratory or qualified technical owner—not from a copied spreadsheet.
Build a “safety evidence interface” into the plan. It should identify the final construction details that the competent evaluator needs: ratings label, mains cord and plug, wiring diagrams, control board, motor/heater, insulation system, protective devices, enclosure materials, accessible parts, instructions and all product variants. If a component changes, ask whether the earlier report, test sequence or technical conclusion still applies; do not presume equivalence from a component’s appearance or a vendor statement.
For EU placement, LVD conformity assessment is the manufacturer’s responsibility; the Commission cautions that unregulated voluntary certificates are not a recognized means to prove compliance in market-surveillance or customs checks.[2] That is a reason to make evidence legible, not a reason to demand decorative certificates. Review the destination-specific route with the responsible party before production release. In markets where the actual product is outside the LVD voltage range, other safety obligations may instead be relevant.
The same discipline applies to radio or electronic features. If a change affects emissions or immunity behavior, re-evaluate the configuration scope rather than assuming that a prior result follows the brand name. The EU EMC framework seeks to control emissions and immunity, while the exact evidence route depends on the equipment and market.[3]
5. Define a completed-unit functional matrix
A completed-unit functional matrix turns “works properly” into repeatable observations. It lists the required inputs, expected outputs, starting conditions, fixtures or loads, sequence, permitted behavior and record. Keep it focused on the released user-visible functions and protections; never use it to invent a performance promise the product has not been designed and evaluated to support.
For a kettle, the matrix may cover control response, indicator behavior and the defined shutoff sequence. For a hand vacuum, it may cover power selection, charge indication, attachment recognition if applicable and the specified response to a commanded condition. For a food-preparation product, it may cover controls, timer, safety interlock and the specified cycle. The actual conditions must follow the product specification and risk review, not a generic category template.
| Matrix element | Decision the buyer needs | Good practice |
|---|---|---|
| Preconditions | Was the unit in the intended starting state? | State supply, installed accessory, programmed setting and any defined load |
| Test action | What did the operator or fixture do? | Use a controlled sequence with clear operator prompts |
| Expected behavior | What counts as the released behavior? | Refer to a revision-controlled requirement, not “normal operation” |
| Data/result | What must be retained? | Record pass/fail plus measurements or screenshots where meaningful |
| Failure route | What happens next? | Stop/segregate, diagnose, assess affected scope and document disposition |
A functional station is particularly vulnerable to false confidence if an operator can bypass a condition, choose a different program or retest until a pass without record. Ask for access control, tester change control, challenge samples or another suitable verification approach. Also ask which output signals are merely internal diagnostics and which result actually supports the release decision.
Where test results are measured, set an appropriate resolution and uncertainty expectation. A number with many decimal places is not evidence of control if the method cannot support the required decision. ISO 9001 frames quality management around, among other elements, documented information, monitoring, measurement and performance evaluation; certification to it is voluntary and does not itself prove product conformity.[6]
6. Build final random inspection into a lot-release decision
A small appliance final random inspection is a buyer acceptance activity on the finished lot, not a substitute for the factory’s own process controls. It commonly verifies accessible condition, assembly, marking, documentation, packaging and agreed functional observations on randomly selected finished units. Define the lot, timing, random-selection approach, inspection level, defect classifications, reinspection protocol and authority to release, hold or ship under concession before the purchase order is executed.
ISO 2859-1:2026 defines acceptance-sampling plans for inspection by attributes, including AQL-indexed single, double and multiple schemes, and it includes switching rules.[4] It is not a universal instruction to select a particular AQL or sample size. Those choices are commercial and risk decisions that should be documented by the buyer and supplier. A passed sample says that the lot met that pre-agreed sampling decision; it is not a statement that every unit is free of defects or that the product has regulatory approval.
| Final-inspection area | Examples to define in advance | Evidence to retain |
|---|---|---|
| Identity and quantity | SKU, color, plug, accessories, carton count | Lot and carton selection record |
| Workmanship and finish | Approved cosmetic limits, gaps, marks, contamination | Photos of material defects and disposition |
| Labels/instructions | Correct revision, ratings, warnings and destination language where applicable | Artwork reference and sample images |
| Function/pack-out | Agreed functional subset, contents, protective packing | Test log and pack-out checklist |
| Defect decision | Critical/major/minor definitions and accept/reject numbers | Inspection report, NCR and shipment decision |
Require the inspector to record deviations rather than quietly exchanging units. If a defect is found, the meaningful response is to establish the affected scope: is it one unit, a carton, a shift, a component lot, a station setting or an earlier production window? Shipment release should be based on the factual evidence and commercial agreement, with any safety concern escalated to competent technical and legal reviewers.
7. Use burn-in purposefully rather than as a ritual
A small appliance burn in test is a controlled period of operating selected units before a decision point, usually to surface early-life or assembly-related issues. It is not automatically required for every appliance, and a long runtime with no defined purpose can consume capacity without increasing useful evidence. The plan should state which risk the burn-in is intended to challenge, which build is selected, the operating program, monitoring, start/stop conditions, record and failure analysis route.
For example, the buyer may want a proposed burn-in activity to look at early control instability, intermittent connections or assembly sensitivity in a selected appliance. That hypothesis needs technical review. It does not establish an advertised service life, and it must not be described as a safety certification. Where heat, moving parts, battery charging or unattended operation are involved, the test setup itself needs a documented risk assessment, supervision arrangement and emergency response appropriate to the activity.
Mid-article CTA — planning a practical test matrix? Share the appliance category, destination markets, configuration documents and intended claims with UZYVO’s OEM/ODM team, or email info@uzyvo.com. The useful output is a configuration-specific discussion of evidence, controls and open decisions—not a promise of approval.
Use a gate after any burn-in activity: review failures, symptom patterns, component lots, tester data and whether a change is needed. A corrective action should identify containment, root-cause method, owner, due date and effectiveness check. “No failure observed” may be recorded as an observation within stated conditions; it should not become a broad reliability claim.
8. Structure endurance and life-cycle work for learning
A small appliance reliability test plan converts anticipated field stresses into a transparent, controlled learning program. It normally asks: which use cases are important; what constitutes a cycle; which environmental or load conditions are relevant; when will units be inspected; what constitutes a failure; and how will results lead to design or process decisions? It should distinguish engineering evaluation, supplier monitoring and evidence required for a specific market route.
Small appliance endurance testing may use repeated actuation, operating cycles, starts/stops, selected loads or other category-relevant stresses. The number and profile cannot responsibly be borrowed from a different appliance. A test on an unloaded motor, for example, may not represent the thermal or mechanical conditions of the final use case. Define the fixture, load, duty cycle, pauses, supervision, unit identity and inspection intervals before testing starts.
The phrase small appliance life cycle testing can be misunderstood. In this guide it means investigating repeated product use or operating cycles; it does not mean life-cycle assessment of environmental impacts, nor does it establish a guaranteed lifetime. Be explicit in reports: list the tested configuration, conditions, interruptions, sample count, observations, failures, analysis limits and the decision reached. Avoid extrapolating from a short run to a consumer-use duration unless an appropriately qualified method and evidence support that conclusion.
| Reliability question | Plan detail to document | Disciplined interpretation |
|---|---|---|
| What is stressed? | Function, mode, load, cycle definition and dwell | A defined test condition, not every conceivable use |
| What is sampled? | Unit IDs, build date, lots and configuration | Evidence for those documented units/configuration |
| What is a failure? | Functional loss, physical change or measurement limit with rationale | A trigger for investigation, not automatic root cause |
| What follows a failure? | Stop rule, teardown authority, containment and retest rules | Controlled learning before a production decision |
| What may be claimed? | Internal decision statement with evidence boundary | Never a generalized lifespan or market-approval claim without support |
A useful reliability report preserves anomalies. A reset, unexpected noise, connector change, warning indication or intermittent event can be important even if the unit later resumes function. Trend those observations across unit IDs and components; do not erase them to create a cleaner report.
9. Govern evidence, changes and independent review
The buyer should be able to trace from a shipment decision back to the relevant configuration and evidence. Establish a validation dossier index before the first build: specification revision, risk register, control plan, work instructions, tester validation/setup records, calibration/maintenance evidence, unit and lot records, completed reports, deviations, corrective actions and market-access documents. Define where records are stored, who can revise them and how an obsolete method is prevented from being used.
Change control is the bridge between reliability learning and routine production. Any proposed substitution, tooling repair, firmware update, process transfer, test-limit change, package revision or destination-market expansion should be assessed for its impact on the charter. The outcome may be “no additional validation justified,” partial revalidation, a new assessment or escalation to a laboratory/regulatory specialist—but it should be a recorded decision with a rationale. The supplier’s ISO 9001 certification, if held, can indicate a management-system framework; it does not remove the buyer’s need to understand this specific product and change.[6]
For a broader view of production systems and technical capabilities, review UZYVO factory capabilities. During supplier selection, confirm whether the proposed factory can provide the records, controlled fixtures, engineering access and corrective-action discipline the plan assumes. Never accept a verbal claim that a test occurs without first seeing the controlled method, current equipment state and anonymized result format where appropriate.
Contextual AI image recommendations
| Insertion point and purpose | English caption | ALT text | English AI image prompt |
|---|---|---|---|
| After Module 2; show the progression from component control to finished-lot review | “A validation plan links each production stage to a defined quality decision.” | “Quality engineer reviewing a small-appliance process control board beside an assembly line” | “Photorealistic B2B industrial scene, quality engineer in neutral PPE reviewing a revision-controlled process control board beside a modern small kitchen-appliance assembly line, no logos, no visible proprietary data, documentary lighting, horizontal composition” |
| After Module 5; clarify the functional-matrix concept | “A functional test should record the unit, preconditions, action and observed result.” | “Bench fixture testing controls on an unbranded countertop appliance with a digital record screen” | “Photorealistic electronics quality laboratory, unbranded countertop small appliance on a safe bench test fixture, engineer recording functional test steps on a screen, no pass certification marks, no logos, clean technical lighting, horizontal composition” |
| After Module 8; portray controlled reliability investigation rather than a claimed result | “Repeated-use evaluation is useful only when conditions and observations are documented.” | “Engineers observing multiple unbranded small appliances on controlled endurance test benches” | “Photorealistic reliability engineering lab with several unbranded small home appliances on supervised endurance test benches, visible unit ID tags but no readable proprietary information, engineers documenting observations, no flames, no safety claims, horizontal composition” |
10. Ask suppliers and inspectors the questions that expose weak plans
A buyer does not need to dictate every work instruction, but should ask questions that reveal whether a proposed plan is executable. The strongest answers point to a current revision, accountable person, controlled method and specific record—not a vague assurance that “everything is tested.” Use the following checklist in the RFQ, technical review and pre-production meeting.
- Which exact configuration, firmware and packaging revision is covered by each proposed test?
- Which risks are controlled at incoming, in-process, completed-unit and finished-lot stages, and why?
- Which controls are 100%, which are sampled and what triggers a change in sampling or containment?
- How is test equipment identified, verified, maintained and linked to its method version?
- What prevents an operator from bypassing a failed functional station or repeatedly retesting until a pass?
- How are rework, repair and retest authorized and recorded?
- Who may substitute a component or change a test limit, and how is the validation impact assessed?
- What raw data, photos and nonconformance records can the buyer review before release?
- What happens when a final-inspection defect indicates an upstream process or component-lot issue?
- Which destination-market requirements require qualified external review before shipment or placing the product on the market?
Buyer FAQs
Does an in-process check replace final inspection? No. In-process controls aim to prevent or detect errors near the operation that creates them. Final inspection addresses the completed, packed lot against a defined acceptance plan. Neither replaces the other, and neither by itself proves legal conformity or future reliability.
Can we set one endurance test for every appliance in our range? Not responsibly. Similar-looking products can have different motors, heaters, electronics, loads, use patterns and market requirements. Reuse a planning framework, but define cycle, conditions, sample rationale and criteria for the final configuration.
Does ISO 2859-1 tell us the right AQL for our product? It provides an acceptance-sampling system for inspection by attributes; it does not make the commercial choice of defect classes, inspection level or AQL for the buyer.[4] Those choices should be agreed with a documented risk rationale.
Does a passed factory test mean the product is certified for every export market? No. Production-test evidence, laboratory evaluation, product documentation and market-access obligations serve different purposes. The applicable obligations depend on the final product and destination. The EU Commission specifically notes that voluntary certificates are not a recognized means to prove compliance under EU harmonisation legislation unless specific legislation provides otherwise.[2]
11. Conclusion: release a controlled evidence package, not a promise
A sound validation plan makes every decision auditable. It begins with a fixed configuration and market context, uses in-process controls to contain known manufacturing risks, defines completed-unit function, applies a justified final-random-inspection plan and uses burn-in or endurance work to investigate defined questions. It also records the boundaries: what was tested, by whom, under which conditions, on which units and what a result does—and does not—mean.
Before awarding or releasing production, ask the supplier to present one connected evidence path: charter to control plan; control plan to test method; test method to product/lot record; deviation to containment and corrective action; and shipment decision to the actual final configuration. If that path breaks, add the missing control or evidence rather than filling the gap with a broad assurance.
Closing CTA — build the plan around your real product. For a structured discussion of factory controls, test evidence and sourcing readiness for your appliance program, visit UZYVO’s FAQ or email info@uzyvo.com. Bring the current specification, destination-market list and expected claims so the conversation can stay configuration-specific.
References
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com