Target Keywords: small appliance quality control; small appliance inspection; small appliance testing; pre shipment inspection small appliances; small appliance factory quality system; small appliance incoming inspection; small appliance third party inspection brief
Direct answer: Build the inspection plan as one governed system, not as a final-day pass/fail event. Start with the approved product configuration and destination-market requirements; translate them into controlled specifications, incoming-component checks, in-process gates, documented functional verification, change control, and an independent inspection brief where useful. The final shipment decision should reconcile evidence from these controls with the exact lot and final configuration. A factory system, an external inspection, and a laboratory report each answer different questions; none should be treated as a substitute for the others.
Introduction. Small-home-appliance buyers often approve a sample, place an order, then ask an inspector to find problems shortly before shipment. That can reveal visible defects, but not reliably establish which components entered the lot, whether design changed, or whether evidence matches the intended market. A stronger approach treats small appliance quality control as buyer-owned governance connecting commercial requirements to factory controls and records.
This guide covers that integration: how to assess and use a factory quality system, write an actionable independent-inspection brief, and make release decisions without confusing sampling with product validation. It does not prescribe an AQL defect table or sampling level. For that separate question, see UZYVO’s small-appliance AQL inspection plan guide.
1. Start with the decision the quality system must support
Before asking for an inspection proposal, define the buyer decisions and evidence for each. An inspection plan should support more than “ship or do not ship”: pilot-build progression, changed-component acceptance, lot traceability, and whether records support the intended market route.
A useful distinction is:
| Control layer | Buyer’s practical question | Evidence that can inform it | What it does not prove by itself |
|---|---|---|---|
| Product definition | Are we building the approved configuration? | Controlled specification, drawings, BOM, artwork, approved sample record | That a production lot was built correctly |
| Factory process | Does the supplier have repeatable controls for this product? | Process map, work instructions, training, calibration and nonconformance records | That every unit or lot conforms |
| Lot verification | Does this identified lot show the agreed characteristics? | Inspection report, test records, lot identifiers, photos | Every safety or performance outcome in all use conditions |
| Market evidence | Is there adequate evidence for the relevant configuration and destination market? | Applicable test reports, technical file, declarations and labels | Approval in every market |
ISO describes quality management in terms of customer focus, process approach, evidence-based decision making, improvement, and relationship management [1]. These principles help buyers request an understandable process, defined responsibilities, usable evidence, and learning from deviations, even without a particular supplier certification.
Set the scope at the SKU/configuration level. Record the product family name, model identifier, rated voltage/frequency, plug and cord arrangement, materials that affect the product, colors or finishes, accessories, packaging version, destination market, sales channel, and claim set. A change in any of these can change what should be checked. The required controls depend on the final configuration, the market in which it will be placed, the supporting evidence, and qualified review where necessary.
2. Convert the commercial brief into a controlled quality baseline
The buyer’s first deliverable should be a controlled baseline, not a generic “quality standard.” Assemble an index to current product requirements and their version owner; it should expose ambiguity before production.
Create a requirement-to-control matrix: requirement; source revision; risk; stage; method or fixture; acceptance criterion; record; owner; and escalation path. For example, it may link a rated-voltage marking requirement to artwork approval, label verification, and a record; or distinguish battery-pack identity, charger identity, and finished-product behavior. These are illustrations, not universal test prescriptions.
A disciplined baseline normally includes:
- the approved sample or golden-sample reference, with dated photos where cosmetics matter;
- the BOM and a list of critical components, suppliers, and acceptable alternates;
- drawings, artwork, label text, manual, carton, and insert revisions;
- functional and appearance requirements written so an operator can evaluate them;
- packaging configuration and handling constraints; and
- a change-control rule stating who may approve deviations before use.
This is where small appliance testing becomes more useful. Do not write “test function” as a requirement. State the product state, input conditions, duration where relevant, observable output, instrumentation or fixture if needed, record, and response to failure. Separate routine line checks from design-validation or market-access evidence. The former helps the factory control a process; the latter may require a different method, facility, sample, standard, or reviewer.
Ask the factory to acknowledge the current revision set before build, then maintain a revision log. A verbal assurance that it will use “the latest files” is not a traceability mechanism. If the buyer does not control the baseline, a later inspection cannot reconstruct with confidence which variant it assessed.
3. Assess the factory system as a working control loop
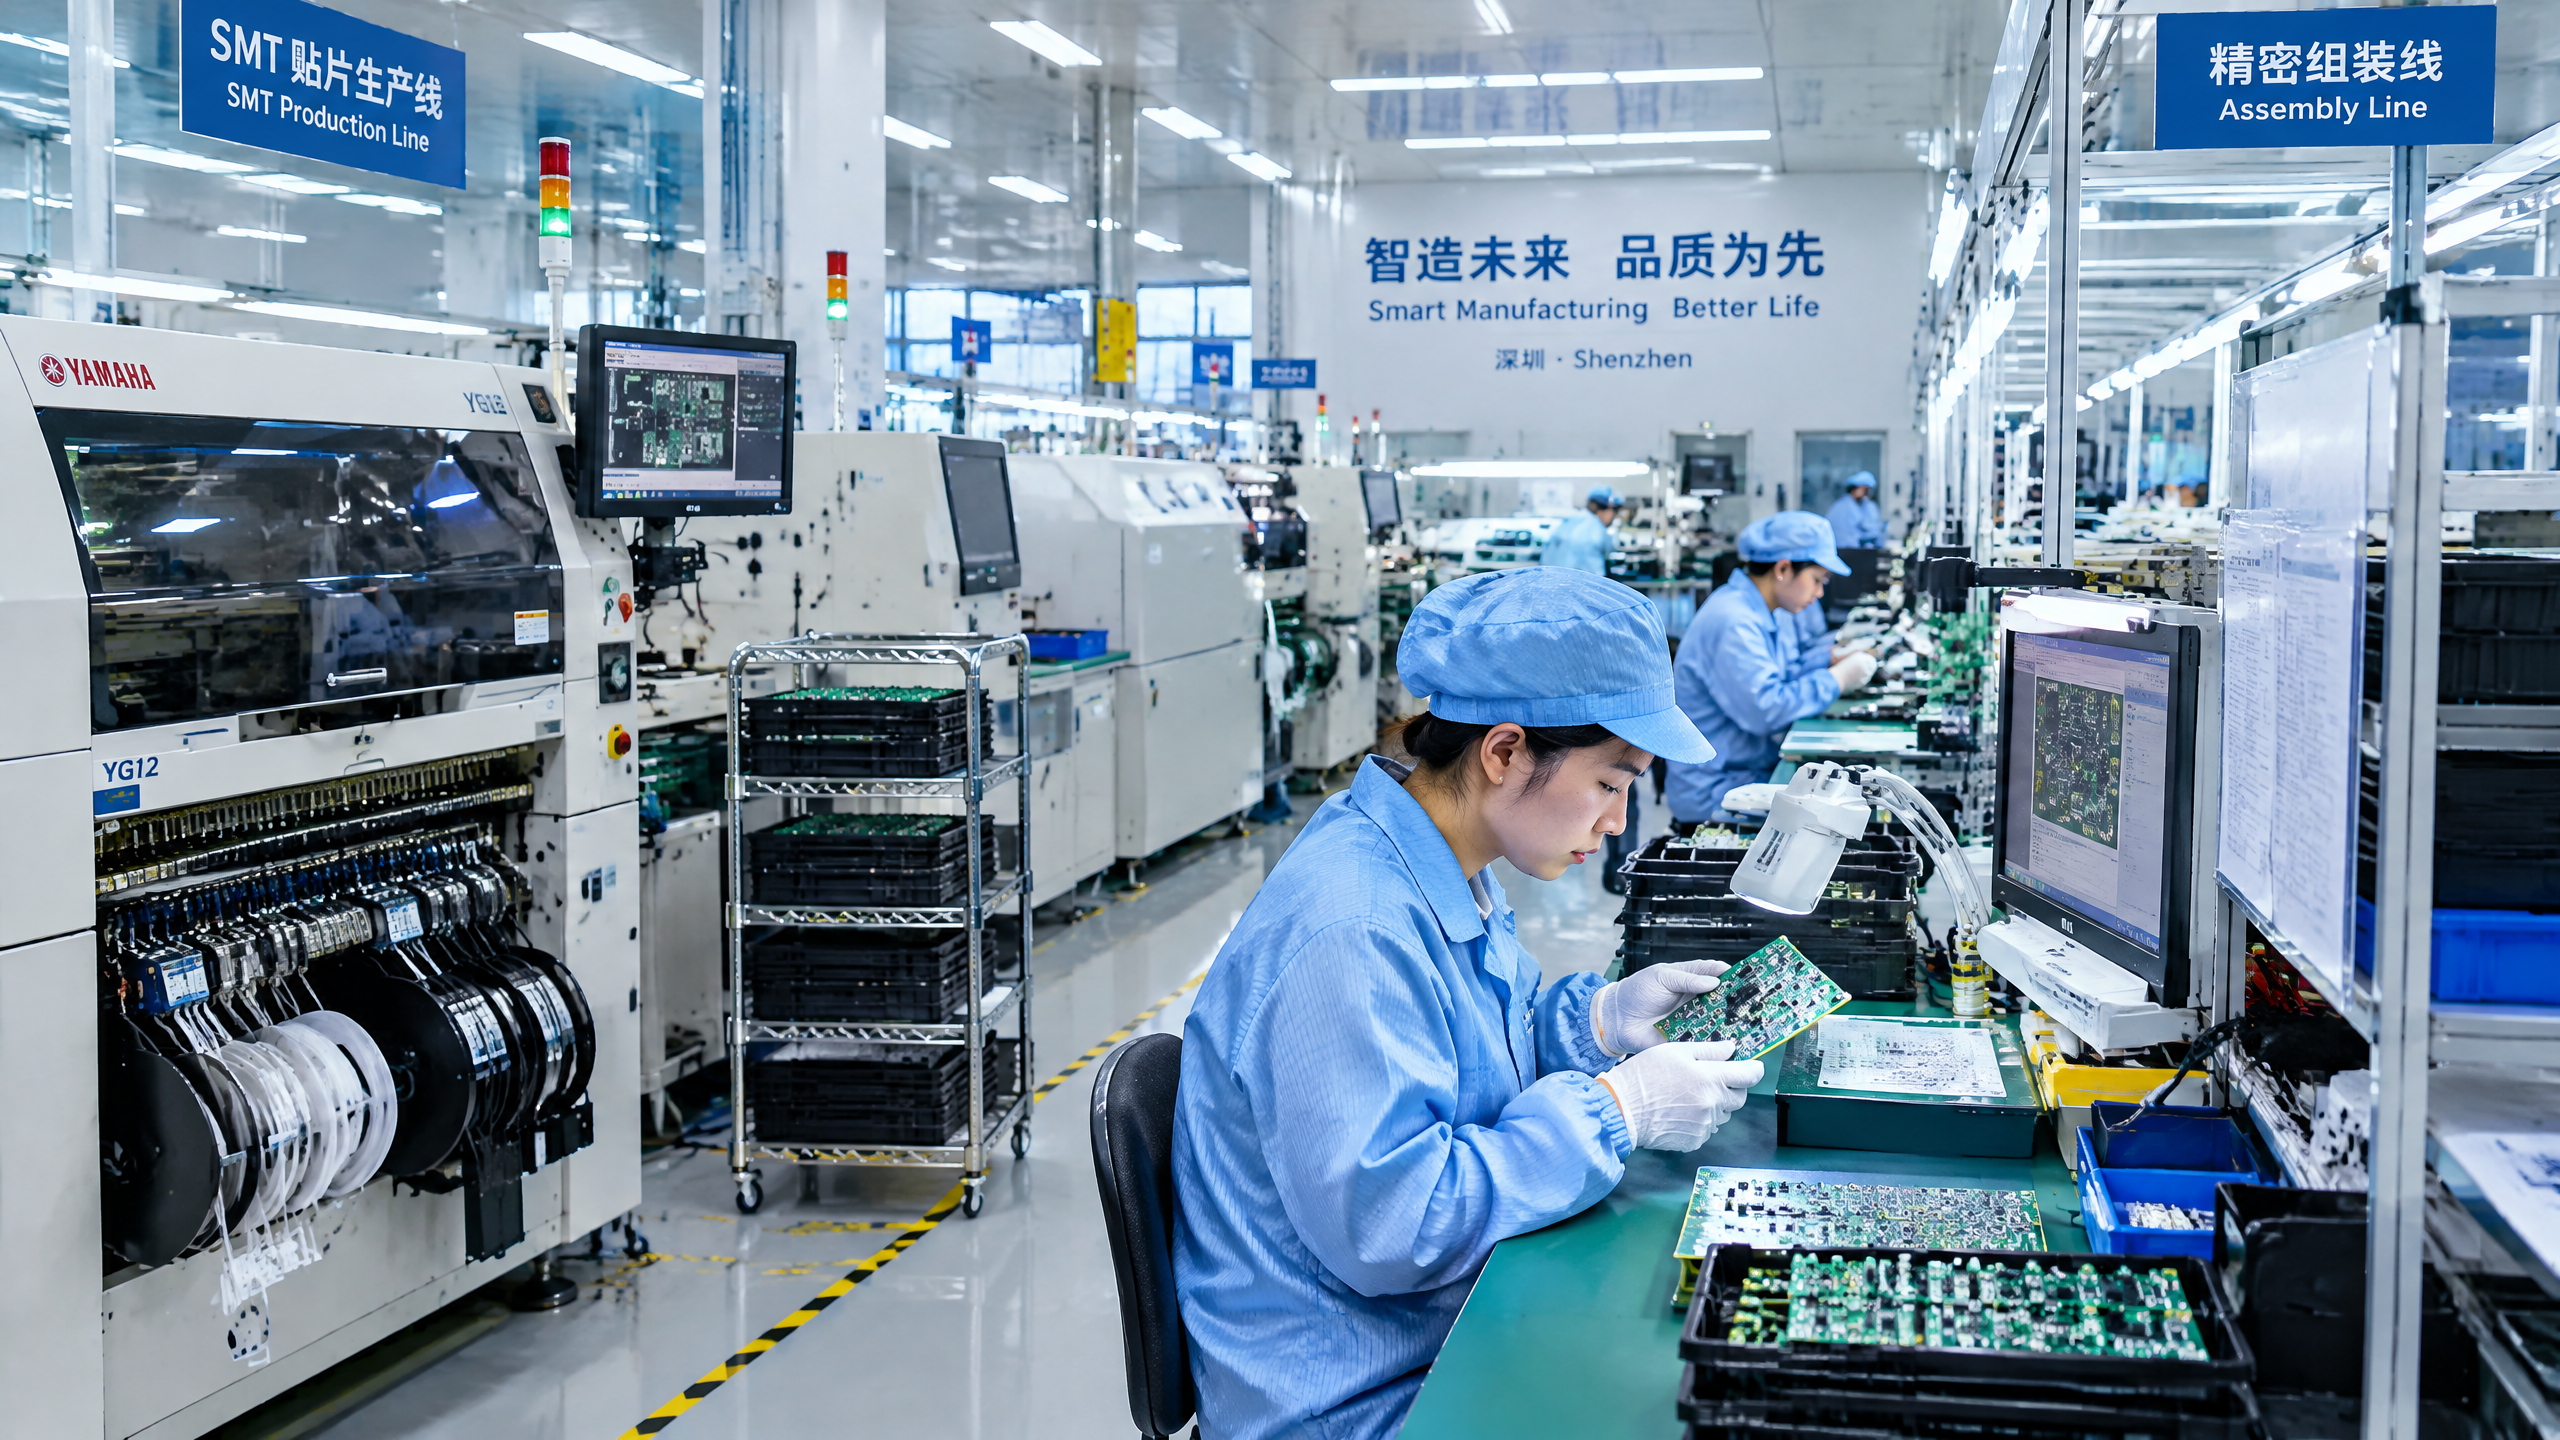
A small appliance factory quality system should be evaluated as a working loop: inputs are received and identified; work is performed to current instructions; deviations are contained; data are reviewed; and corrective actions are checked for effectiveness. A certificate, if offered, can be one piece of supplier evidence, but it should not end the buyer’s review or be presented as product conformity evidence.
Begin with a document review and, where proportionate, a factory visit or remote walkthrough. Ask the supplier to demonstrate—not merely describe—the flow for the particular product. Follow one actual component or subassembly from receipt through issue to the line, testing, packing, and finished-goods identification. The objective is not to “grade” a factory from a brochure; it is to discover whether its controls can be connected to the buyer’s configuration.
| System topic | Evidence or demonstration to request | Buyer decision it informs |
|---|---|---|
| Responsibility | Named quality, engineering, production, and release owners; escalation route | Who can stop, disposition, or approve work |
| Document control | Revision status at workstation; withdrawal of obsolete instructions | Whether approved requirements can reach the line |
| Measurement control | Equipment list, status identification, and records appropriate to the method | Whether recorded measurements are interpretable |
| Nonconformance | Segregation, disposition record, root-cause and corrective-action workflow | Whether defects are contained rather than reintroduced |
| Traceability | Lot/batch links from critical input to finished carton or unit where feasible | Whether a finding can be bounded to affected goods |
| Supplier control | Critical-component approval and change notification process | Whether material variation has a review path |
For suppliers considering broader OEM/ODM cooperation, UZYVO’s OEM/ODM overview can help frame the commercial and development workflow. The quality review should nevertheless remain product- and configuration-specific. ISO’s QMS principles emphasize process approach and evidence-based decisions [1]; a buyer can use those ideas to request records that are meaningful without assuming the same procedures fit every factory.
4. Make incoming inspection risk-based and traceable
Small appliance incoming inspection is the bridge between an approved component and its use in a finished product. It should not mean opening a fixed percentage of every box regardless of risk. Instead, identify inputs whose variation could affect safety, function, identity, cosmetic consistency, packaging, or regulatory evidence, then define a reasonable receipt, verification, quarantine, and release path for those inputs.
For each critical input, agree the identifier the factory should preserve: supplier part number, material grade where relevant, lot or date code, report reference, incoming disposition, and link to the finished lot. Examples may include a heating element, thermal protector, motor, PCB, power cord, battery pack, food-contact component, label, or charger. Whether an item is “critical” must be decided from the product’s actual design and intended market, not copied from another appliance.
The control plan should say what happens when an input is wrong or uncertain: segregate it, prevent issue to the line, open a deviation record, determine the affected work orders, and obtain buyer or engineering disposition where the change touches an approved requirement. It should also require current approved-supplier or alternate-part status. A supplier test document may be relevant evidence, but the buyer should confirm that the document, part revision, lot, and final use align.
For U.S. consumer products subject to applicable CPSC rules, CPSC explains that a General Certificate of Conformity must be supported by product testing or a reasonable testing program, and that component-part testing may be relied upon only with due care and adequate supplier information [2]. That is a useful reminder, not a universal release rule: incoming records support confidence in controlled inputs, but they do not automatically establish compliance of the final assembled appliance.
5. Place controls at the points where defects can still be contained
A mature small appliance inspection approach does not reserve all observations for the finished-goods warehouse. Map the actual build sequence and assign gates where an error can be detected, contained, and investigated before it becomes a shipped product. The appropriate gates vary by appliance architecture, automation, assembly method, and risk.
Typical stages can include first-article confirmation at startup; subassembly verification; checks before irreversible closing or sealing; controlled functional checks; final assembly and appearance review; packing verification; and finished-lot identification. The purpose is not to impose a universal checklist. It is to give the factory and buyer a shared answer to four questions at each gate: what is checked, against which controlled document, by whom and with what method, and what record remains.
For critical functional checks, define the test method sufficiently that a later reader can understand the result. Identify the product configuration, fixture or instrument, input conditions, operator or station, result type, date/time or lot link, and failure disposition. Avoid relying on a display reading alone when the relevant condition or acceptance basis is undefined. If a test station software version, fixture, or limit changes, it should enter the same change-control pathway as another production-relevant change.
The buyer should request trend review at intervals appropriate to production risk: recurring defect category, station or line, relevant component lot, containment action, root-cause hypothesis, corrective action, and effectiveness check. This is not a promise that a factory will eliminate all defects. It is a way to decide whether the system detects deterioration early enough for a commercial response.
Keep safety-related evidence and routine workmanship evidence distinct. A cosmetic observation may justify rework or a shipment discussion. A question that could affect product safety, a regulated claim, or configuration identity may require engineering and compliance review, extra evidence, or a hold. Final judgments should be made against the product, applicable requirements, supporting evidence, and destination market—not an inspector’s informal conclusion alone.
6. Govern changes before they reach the production lot
Component substitutions, revised tooling, new material sources, updated artwork, alternative test fixtures, and process moves can all disrupt the evidence behind an approved product. The system should therefore include a written change-notification trigger, a review group, and a clear “no use until disposition” rule for defined changes.
At minimum, a change request should describe the old and proposed item or process, affected models and lots, reason, risk assessment, documents affected, evidence supplied, implementation date, stock disposition, and approval record. The buyer should require advance notice at a level proportional to the impact. A spelling correction on a non-regulated carton may have a different review path from a modified power component; neither should disappear into email without a record.
CPSC’s guidance notes that a material change to product design, manufacturing process, or component source that could affect compliance should prompt appropriate retesting, and emphasizes that ongoing control of incoming materials and production processes can support a reasonable testing program [2]. This U.S.-specific guidance should not be generalized into legal advice for all markets. It does, however, show why a change log cannot be separated from the buyer’s test and release logic.
A practical governance cadence is a pre-production review of the baseline; a production review of open deviations and records; a pre-shipment reconciliation of lot, documents, and inspection scope; and a post-shipment review of repeat findings. Assign a named buyer owner for acceptance of commercial deviations, a technical owner for configuration changes, and a supplier owner for containment. Silence is not approval.
Need a configuration-led quality workflow? Share your product scope, destination markets, and current document set with UZYVO’s team. The discussion can focus on the controls and evidence appropriate to the final configuration rather than a one-size-fits-all checklist.
7. Brief third parties precisely—and understand their limits
A small appliance third party inspection brief should be a controlled request for evidence, not a vague instruction to “inspect to international standards.” State the inspection type, factory address and contact, SKU/configuration and revision, order quantity, expected production status, lot identifiers, documents to use, required photo list, tests the inspector is authorized to witness or perform, report timing, and escalation contacts. Also identify what is expressly outside scope.
This produces better outcomes for pre shipment inspection small appliances because the inspector can compare the correct product, packaging, and marking against an agreed baseline. It also reduces the risk that a site team shows a sample, carton, or instruction revision different from the production lot.
| Activity | Best question it can answer | Important limitation |
|---|---|---|
| Factory-system review | Are specified controls and records demonstrable at the time reviewed? | It does not certify every future lot or product |
| In-process visit | Are agreed controls operating during the observed build? | It captures conditions within a limited visit scope |
| Pre-shipment lot inspection | Does the identified accessible lot meet the defined visual, quantity, configuration, and functional-check scope? | It is not full product validation or market authorization |
| Laboratory evaluation | Does a submitted sample meet the stated method under stated conditions? | Sample and method coverage must match the final configuration and applicable need |
A brief must distinguish observation from release authority. An independent inspector can document conditions, counts, photographs, records reviewed, and deviations against the agreed scope. The buyer retains the commercial shipment decision, and the responsible economic operator or qualified advisor should address any legal or conformity obligations applicable to the destination market.
For electrical equipment, IECEE describes the CB Scheme as a system for mutual acceptance of safety test reports and certificates among participating certification bodies and countries [5]. It can be relevant evidence in a defined conformity route, but it is not a substitute for configuration control, production-lot traceability, or destination-market review. State certificate/report references in the brief only after confirming that model, components, ratings, and national differences are appropriately mapped.
8. Reconcile lot inspection data with the release decision
Inspection data must be read in context. ISO 2859-1:2026 defines acceptance-sampling systems for inspection by attributes, including AQL-indexed single, double, and multiple sampling schemes [6]. It is a statistical sampling framework, not a declaration that a sampled lot is fully conforming, a factory system is effective, or a product meets all market requirements. Sampling design belongs in the commercial quality agreement and should be set by the buyer’s risk appetite and the relevant lot/product circumstances.
Rather than repeat a sampling plan here, build a release packet that connects the inspection report to the rest of the control system:
- purchase order, SKU, quantity, factory, and final lot or shipment identifiers;
- approved revision index and confirmation of any approved deviations;
- critical-component and production-control records agreed for the lot;
- inspection report, scope, sample basis, observations, photos, and any recheck result;
- functional-test and packaging evidence within the agreed scope;
- market-documentation status and configuration mapping, where applicable; and
- a written release, hold, rework, or concession decision with decision owner.
Do not make a numerical result the only decision input. A lot might meet its agreed sample acceptance rule while still revealing an unapproved configuration change or missing documentation. Conversely, a minor observed issue might require a defined rework and reinspection rather than an unsupported declaration that the entire shipment is good or bad. The report should preserve facts: what was observed, where, against which revision, on what date, and what evidence was available.
When a defect recurs, use it as a signal to inspect the system: Was the requirement ambiguous? Did incoming control identify the relevant variation? Was the workstation using the current instruction? Was the test method stable? Was a corrective action verified? This connects lot results to continuous improvement rather than simply negotiating the next shipment.
9. Link quality records to market-access documentation
Quality records and market documentation often sit in separate folders, even though both depend on product identity and change control. The buyer should make the links explicit. A technical file, test report, declaration, marking artwork, manual, and production BOM are most useful when their model, rating, component, revision, and destination-market references can be reconciled.
For products subject to EU harmonised rules, the European Commission explains that affixing CE marking is the manufacturer’s declaration that the product meets applicable legal requirements; it is not an approval by the EU or another authority [3]. EU guidance says technical documentation should demonstrate compliance, include the design/manufacture/operation information and risk analysis required by applicable rules, and be available to market-surveillance authorities as required [4]. Exact applicability depends on the product and law; buyers should obtain qualified review for their configuration and target market.
For U.S. general-use products subject to CPSC rules, a manufacturer or importer must issue a GCC based on testing of the product or a reasonable testing program; overseas products place the GCC issuance responsibility on the importer [2]. CPSC also says the responsible party must ensure continued compliance and consider retesting when a material change could affect it [2]. Do not convert these points into a generic rule for every appliance or jurisdiction. Instead, maintain a market matrix that identifies the destination, responsible party, applicable requirements to be assessed, evidence owner, record location, and re-evaluation triggers.
The system should prevent a common mismatch: a laboratory report for one sample or rating being attached to a visually similar production variant without a documented technical basis. If the factory proposes a substitute or a new configuration, pause the assumption of coverage. Compare the final configuration to the evidence, determine whether further review or testing is appropriate, and record the outcome.
Contextual AI image recommendations
| Insertion point and purpose | Caption | ALT text | AI image prompt |
|---|---|---|---|
| After Module 3; show evidence flowing through a factory system | “A buyer’s quality baseline should connect documents, component traceability, process controls, and release records.” | “Illustrated small-appliance quality workflow from approved specification through factory records” | “Editorial B2B infographic, clean technical style, a small countertop appliance production workflow linking approved specification, incoming components, assembly controls, test station, nonconformance record and shipment release; neutral blue and graphite palette; no brand names, no numbers, no certification marks” |
| After Module 6; clarify disciplined change control | “A controlled change request makes component and process variation visible before implementation.” | “Quality team reviewing a controlled component-change request beside appliance parts” | “Realistic documentary factory meeting, diverse quality engineer and buyer reviewing revision-controlled component change documents beside unbranded small appliance parts, organized desk, factory background, natural lighting, no logos, no readable proprietary data” |
| After Module 8; show a factual inspection handoff | “Independent inspection evidence should be reconciled with the identified lot and approved configuration.” | “Inspector documenting an unbranded small-appliance shipment with cartons and checklist” | “Professional third-party inspector in an export warehouse photographing unbranded small appliance cartons and checking a neutral clipboard against a product sample, visible lot-label placeholders but no readable numbers, factual documentary photography, no logos” |
10. Implement the buyer system and resolve common questions
Implementation should be staged so the buyer does not create paperwork with no operating owner. Use the first order to establish the baseline and records, then improve the control plan with actual findings. For a broader supplier-capability discussion, see UZYVO’s factory capabilities; for operational questions around sampling, production, and sourcing, visit the buyer FAQ.
| Buyer checkpoint | Accountable role | Practical output before the next gate |
|---|---|---|
| Freeze configuration and documents | Product/technical owner | Revision index, approved sample reference, BOM and artwork status |
| Confirm factory controls | Sourcing and quality owner | Process map, named owners, key records and escalation contacts |
| Identify critical inputs and changes | Technical owner with supplier | Critical-input list, alternative-part rules, change-request template |
| Authorize independent work | Quality owner | Scoped brief, inspection date window, product/lot identification and photo requirements |
| Reconcile and decide | Commercial release owner with technical input | Release packet, written decision, deviations and follow-up actions |
| Review recurrence | Quality and supplier management | Trend log, corrective-action ownership and effectiveness-review date |
FAQ 1: Is a factory quality-system certificate enough for a buyer to skip inspection?
No. A system certificate, when valid and relevant, may inform confidence in a supplier’s management processes, but it does not identify the final product configuration, confirm the specific production lot, or replace agreed verification. Decide the scope of any inspection from product risk, supplier history, contract terms, and the destination-market evidence needed. Review the certificate scope, current status, and the operating records for the product rather than treating the certificate as a blanket product approval.
FAQ 2: Can pre-shipment inspection replace small appliance testing?
Usually, they have different purposes. A pre-shipment visit can assess the specified accessible lot and perform or witness agreed checks, while testing may be a controlled production check, a laboratory method, or evidence for a particular requirement. The suitable method, sample, conditions, and reviewer depend on the final appliance, intended claim, and destination market. Define both scopes before the order; do not describe an inspector’s observation as proof of matters the brief did not evaluate.
FAQ 3: What should trigger a new review after the sample is approved?
Trigger review for a change that could alter product identity, function, safety-related design, applicable evidence, labeling, user information, packaging, or a promised claim. Examples can include a different component source, firmware or fixture revision, rated-input change, cord or plug change, material substitution, or modified artwork. The technical significance must be evaluated against the actual configuration and market requirements; the supplier should not self-approve a buyer-controlled change simply because it appears equivalent.
FAQ 4: What makes a small appliance third party inspection brief useful?
It is useful when it unambiguously names the SKU and revision, accessible lot, order quantity, comparison documents, observable checks, photo requirements, reporting format, escalation route, and exclusions. It should also state whether the inspector is witnessing a factory test, performing a defined check, reviewing records, or only observing presentation. A precise brief improves evidence quality; it does not turn the inspector into the buyer’s legal or conformity authority.
11. Conclusion: make release a documented governance decision
The buyer’s goal is not the longest checklist or the most dramatic final inspection. It is a transparent chain from approved configuration to controlled inputs, production records, change decisions, lot evidence, and market documentation. That chain makes small appliance quality control more actionable: it reveals where a problem entered, who owns containment, and whether the shipment decision rests on the right evidence.
Build the system around the final product configuration and destination market. Use factory records to understand process control, independent inspection to gather the agreed lot evidence, and qualified technical or compliance review where applicable requirements call for it. Keep sampling, product testing, certificates, and market documentation in their proper roles. None alone guarantees the quality, safety, legality, or commercial outcome of a shipment.
Ready to structure a buyer-led inspection and quality workflow? Email info@uzyvo.com with the appliance category, configuration, destination market, and sourcing stage. UZYVO can help scope the documentation and control questions that should be resolved before production and release.
References
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com