1. Concise answer
A small appliance factory audit checklist should establish whether a supplier can repeatedly make the *approved* product, not simply whether its premises look orderly. Before a private-label order, verify four things: the factory controls safety- and compliance-critical inputs; its process produces consistent units; its records trace a finished product to material, test, and production data; and its evidence matches the exact SKU and destination market.
For countertop appliances, personal-care devices, cleaning appliances, fans, kitchen electrics, and related products, use this sequence:
- define the SKU, intended markets, specifications, and buyer release criteria;
- map the actual process, including outsourced operations;
- follow a product lot from receipt of material through packed carton;
- sample dated records that prove controls operate over time;
- reconcile the technical file and test evidence to the precise configuration; and
- convert gaps into written corrective actions and a supplier-approval decision.
An audit is supplier due diligence and manufacturing-risk assessment. It does not replace product certification, inspection, legal advice, or market-specific conformity assessment. In the European Economic Area (EEA), CE marking is the manufacturer’s declaration that a product meets applicable requirements; it is not a general EU authority safety approval and must not be used outside its legal scope.[1] In the United States, an importer can have separate testing, certification, and recordkeeping responsibilities.[6]
The desired conclusion is therefore not just “factory passed.” It is a documented answer to: *Can this supplier make our defined SKU under controlled conditions, protect approved design inputs, and provide credible evidence when a retailer, authority, or customer asks?*
Audit principle: observe the process, interview the owner, sample dated records, and trace every claim to the product configuration. A promise is not evidence; a report for another model is not evidence.
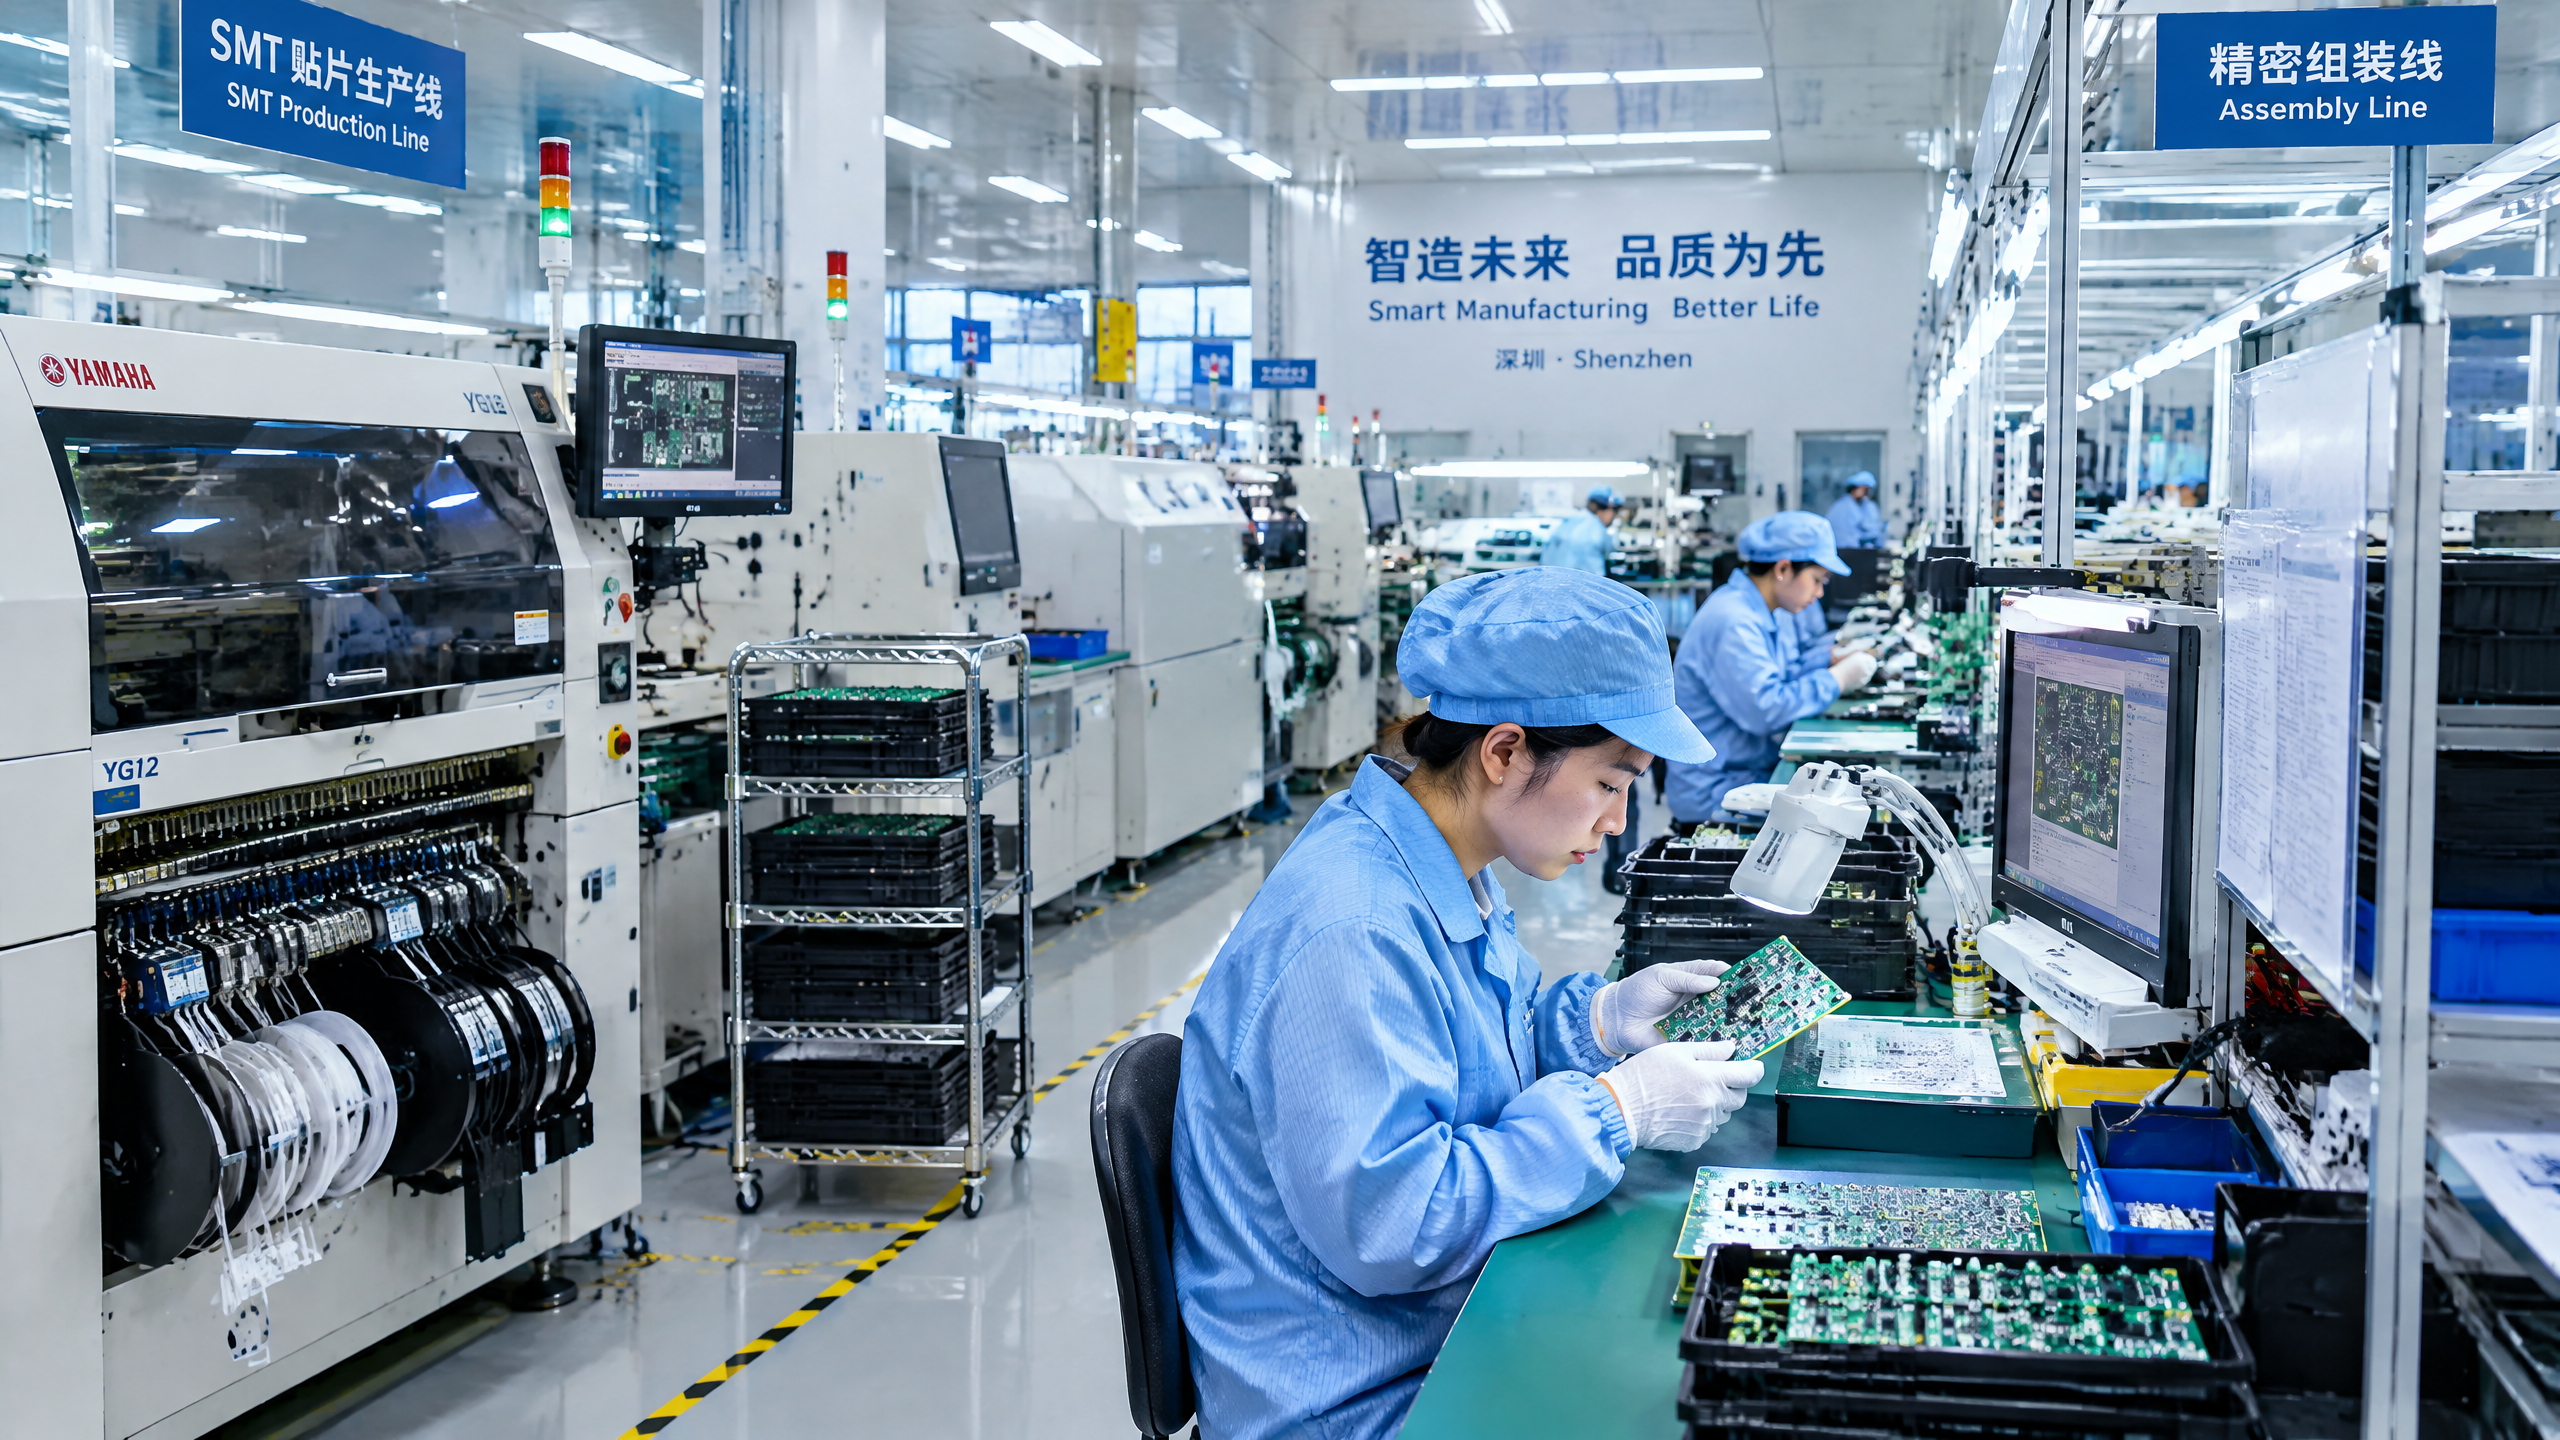
AI image suggestion 1 — Audit opening scene
- Purpose: Establish the article’s on-site buyer perspective.
- Placement: After the audit principle above.
- Caption: A buyer audit should follow real production and records, not only presentation samples.
- Alt text: Private-label buyer and quality engineer reviewing a small appliance assembly line and inspection records.
- English generation prompt: *Documentary-style commercial photograph of a private-label buyer and quality engineer auditing a modern small-home-appliance assembly line, checking a kettle-sized appliance and batch paperwork, natural factory lighting, realistic production detail, no visible logos, no readable confidential documents, wide horizontal composition.*
2. Why the audit matters to private-label buyers
A private-label buyer owns the product promise even when another company designs, sources, assembles, or tests the appliance. Its brand is on the product, packaging, instructions, online listing, and often the warranty route. A useful audit asks whether the supplier’s *everyday operating system* can support that promise at repeat order, not whether one showroom sample works.
Small appliances make that question consequential. One SKU may combine mains power, heat, moving parts, plastics, metal, electronics, chargers, batteries, wireless functions, food-contact components, or water exposure. A change in a cord supplier, thermal protector, resin grade, screw torque, heating element, software version, label artwork, or packaging may affect safety, function, durability, or market-access evidence. Requirements vary by product and country; a test report for a similar unit is not automatically sufficient.
An audit reduces four connected uncertainties:
- Capability: Does the site actually make this appliance class, or merely source and relabel it? Identify in-house versus outsourced moulding, PCB assembly, final assembly, testing, packaging, and ageing.
- Consistency: Does the factory link the approved bill of materials (BOM), work instructions, first-off approval, inspection points, nonconforming-product control, and release records? ISO’s quality-management principles stress process approach, improvement, evidence-based decision-making, and relationship management—helpful audit lenses even when ISO 9001 certification is not a buyer requirement.[10]
- Compliance: Can the supplier provide controlled inputs to the technical file, including product identification, critical materials, risk information, labels, instructions, and tests? EU technical documentation generally needs to be retained for 10 years unless relevant legislation specifies otherwise.[2]
- Commercial execution: Can it prevent late redesigns, unapproved substitutions, weak packaging, and repeat defects before they consume time and margin?
The correct audit depth is risk-based. A simple corded product can merit a different programme from a heated, connected, battery-containing appliance. Consider product risk, novelty, supplier history, sales channel, order value, and the consequences of a nonconformity. A universal score threshold is rarely as reliable as a clear risk and release plan.
3. Scope and definitions: factory audit versus product approval
A factory audit assesses a manufacturing location’s management system, process control, competence, supplier management, traceability, and corrective-action discipline. It asks whether the organisation can consistently make a defined product. A first-order, SKU-focused on-site audit usually reveals more than a generic supplier questionnaire.
A product evaluation assesses the particular appliance: its construction, materials, labels, instructions, foreseeable use and misuse, performance claims, and test results. Product safety is specific to the item and market. IEC 60335-1 is a general safety standard for household and similar electrical appliances, but relevant particular requirements and national differences must be checked for the product and destination.[11]
A pre-production inspection verifies that components, artwork, tooling, and early units match the approved baseline. An in-process inspection checks control while production runs. A pre-shipment inspection samples finished goods against agreed criteria. Each complements the audit; none replaces the others.
A conformity assessment evaluates whether a product meets applicable legal requirements. EU guidance says manufacturers must conduct risk analysis and ensure compliance before product placement; depending on the legislation, the work may be self-assessed or involve a notified body.[3] A test report is evidence for the sample, version, method, and conditions described in it. It is not a universal passport for every plug, power rating, component selection, factory, or later revision.
A good corrective action states the nonconformity, immediate containment, root cause, action, accountable owner, due date, evidence, and effectiveness check. Define what constitutes a critical finding before the audit. Potentially serious safety risks, falsified or irreconcilable evidence, or uncontrolled critical substitutions should block release until adequately resolved and verified.
Finally, keep roles distinct: legal manufacturer, brand owner, importer, authorised representative where relevant, and factory. A contract can allocate tasks, but it does not necessarily change statutory responsibility. Confirm roles before approving artwork, documentation, or shipment.
4. Evaluation framework: people, process, product and proof
Use four connected lenses—people, process, product, and proof—to stop a factory audit becoming a tour plus a certificate review. Tie every question to the actual SKU.
People: authority, competence, and escalation
Start with the organisation chart, then test it. Who can stop the line? Who approves a new component source, work-instruction revision, or deviation? Who owns regulatory records, calibration, incoming inspection, final release, and customer complaints? Ask several role holders to explain the same process. Inconsistent answers can expose a procedure that is not embedded in practice.
Review training for safety-critical stations such as wiring, crimping, soldering, high-potential testing, grounding-continuity checks, torque-controlled assembly, functional testing, and final inspection. Sample records across shifts. Training should be station-specific, current after instruction changes, and understandable to the operator. On the line, check that the latest visual instruction is in use and that an operator can describe a fail condition.
Ask what happens if someone detects a safety or quality issue. A credible answer includes quarantine, line stop, lot identification, disposition, investigation, and escalation. Review a closed complaint or nonconformity record to see whether the supplier verified that its action worked.
Process: control the flow, not only the final test
Walk one SKU through receiving, incoming inspection, storage, kitting, assembly, in-process test, ageing where used, final inspection, packing, finished-goods storage, and loading. Compare the actual route with the process map. Look for mixed materials, unlabelled containers, uncontrolled rework, components outside defined storage, or cartons that cannot be linked to a lot.
For each critical part, request the specification, approved supplier, incoming criteria, a recent purchase lot, inspection result, and the link to the finished-product BOM. Critical parts may include cords and plugs, thermal devices, fuses, heating elements, batteries, chargers, switches, PCBs, motors, plastics near heat, fasteners, and food-contact components. The list must come from the product risk assessment and test plan, not a copied checklist.
Check prevention points before an error becomes difficult to detect. End-of-line functional testing may not catch wrong polarity, poor insulation routing, incorrect torque, or incorrect firmware. For relevant fixtures, examine pass/fail limits, failed-unit locks, verification frequency, retest rules, version control, and links between results and the applicable lot or serial number.
Failed units, suspect parts, returns, and rework should be visibly segregated and status-labelled. Verify who can authorise rework and how reworked units are re-inspected. A rejected-parts pile beside an active line is meaningful evidence, even if a polished final-inspection form exists.
Product: configuration control from sample to carton
Select a physical line unit and compare it with the approved sample, BOM, drawings, control plan, artwork, and instructions. Check model number, rating, plug, label, languages, accessories, cord, colour/material designation, relevant firmware revision, and carton configuration. These are not merely cosmetic details where they affect safety evidence or market destination.
Review change control. The supplier should identify a design, material, source, tool, process, software, test, or site change; assess its effect; obtain required approval; and trigger revalidation or retesting where needed. CPSC guidance makes the related point that a material change capable of affecting compliance may require retesting, while the manufacturer or importer remains responsible for certification.[6]
Proof: dated, traceable, model-specific evidence
Sample documents; do not just list them. Select a recent production lot, then retrieve incoming records, first-off approval, in-process data, final-test data, packing record, and release. Next, take an incoming critical component and trace it forward to finished units. If this cannot be done in both directions, qualify the supplier’s traceability claim.
Verify test and measuring equipment identification, status, acceptance criteria, calibration or verification, and treatment of an out-of-tolerance device. A calibration sticker alone is not enough: the method, range, and accuracy must suit the measurement. For safety-related fixtures, determine who controls programs and how changes are authorised.
AI image suggestion 2 — Traceability evidence
- Purpose: Visualise the link between components, process controls, and finished-goods release.
- Placement: After the “Proof” subsection.
- Caption: Effective traceability lets a buyer move from a packed unit to its process and component records.
- Alt text: Labelled appliance components, a barcode scanner, and quality records on a factory workstation.
- English generation prompt: *High-detail realistic photograph of an organised small-appliance quality-control workstation, unbranded heating component, power cord, barcode labels, handheld scanner, and generic inspection record with no readable text, clean industrial lighting, shallow depth of field, horizontal editorial image.*
5. Compliance and risk: validate evidence by market
Begin with a market-and-SKU compliance matrix. Include destination, model and variants, electrical rating, intended use, applicable legislation, relevant standards or methods, required markings, language needs, documentation owner, responsible economic operator, and evidence status. Have qualified regulatory and legal resources confirm the matrix. This is a sourcing checklist, not a legal determination.
For the EEA, do not ask only, “Do you have CE?” Ask which EU rules apply, what risks were assessed, which standards or technical solutions support conformity, which exact model and configuration the evidence covers, and who will sign the EU declaration of conformity. EU guidance says technical documentation should include product identification, facilities involved, conformity procedure, applicable rules, standards, risk assessment, critical components/materials, test evidence, label, and instructions.[2] For products under multiple EU laws, map each function to the relevant rule and standard.[2]
The General Product Safety Regulation (GPSR) applies from 13 December 2024 and complements sector-specific rules for risks that they do not address. It strengthens lifecycle risk assessment and requires a responsible economic operator in the EU for each covered product.[4] Audit whether the factory can supply correct traceability, labels, instructions, incident data, and change records, while separately confirming the buyer’s and EU operator’s duties.
For electrical and electronic equipment in scope, RoHS restricts ten substances and applies to products with an electrical or electronic component unless an exclusion applies.[5] Review how declarations and material evidence are controlled, how any relevant exemption is managed, and how an unapproved material substitution is prevented. Consider WEEE separately with local advisors and producer-responsibility schemes; the EU identifies household appliances as WEEE and notes the environmental and health concerns caused by poorly managed e-waste.[12]
For the United States, first determine which CPSC rules apply. For general-use products subject to CPSC rules, the manufacturer or importer must issue a written General Certificate of Conformity (GCC) based on product testing or a reasonable testing programme; CPSC says the importer issues the GCC for products made overseas.[6] CPSC also states that an eFiling requirement for certificates of compliance begins for most regulated consumer-product imports on 8 July 2026.[6] Confirm current scope and entry requirements before shipment.
U.S. electrical acceptance can also be influenced by retailers, insurers, local authorities, workplace rules, and product category. OSHA’s NRTL programme recognises private organisations, within their scopes, to certify certain products to relevant safety standards. An NRTL mark signifies that the NRTL tested and certified the product to one or more appropriate standards.[7] Confirm the standard, body scope, model coverage, factory follow-up, and mark-control conditions rather than treating a mark as universal approval.
Wireless or digitally controlled products create further questions. FCC guidance distinguishes certification from Supplier’s Declaration of Conformity (SDoC): the route depends on the RF function, intentional radiators normally require certification, and unintentional digital circuitry may follow SDoC. The SDoC responsible party must be located in the United States.[8] Audit firmware, RF-module, antenna, enclosure, and label-artwork change controls accordingly.
A CB Test Certificate and report can be valuable supporting evidence because the IECEE CB Scheme provides a mutual-acceptance system for electrical/electronic test reports and certificates.[9] It does not remove the need to check target-market rules, national differences, current product configuration, or any national certification and labelling requirements.
6. Decision table: score evidence, risk and next action
A decision table makes the audit repeatable. Rate each area for observed control, objective evidence, and SKU/market relevance. A numerical score can help compare sites, but strong housekeeping should never offset a critical safety or evidence-integrity concern.
| Audit area | Good evidence | High-risk signal | Buyer action |
|---|---|---|---|
| Identity and scope | Legal entity, site, processes, subcontractors, and SKU ownership are clear | Key process location or control owner is unclear | Verify site/subcontractors; defer approval if identity is unresolved |
| Configuration | BOM, drawings, sample, artwork, and line unit agree | Unapproved cord, component, rating, firmware, or label | Hold configuration; assess impact and revalidate as required |
| Critical components | Approved sources, specifications, incoming checks, lot records | Missing records, mixed lots, or “equivalent” unassessed parts | Quarantine affected lots; requalify component and source |
| In-process controls | Current instructions, trained operators, verified fixtures, defined limits | Operators rely on memory; failures can bypass control | Add controls, train, pilot, and re-audit as appropriate |
| Traceability and release | Lot link, inspection/test records, authorised release | Records cannot link to product or appear completed after the fact | Do not ship; investigate integrity and restore only verified evidence |
| Compliance file | Model-specific risk, evidence, labels, instructions, declarations | Generic or mismatched reports; unsupported mark | Obtain competent review and correct before market placement |
| Corrective action | Containment, root cause, owner/date, evidence, effectiveness | Vague promise or repeated finding | Keep approval conditional and verify closure |
Classify the result as approve, conditional approve, defer, or reject. Conditional approval should name the SKU, time limit, inspection intensity, non-negotiable closures, and the evidence required for full approval. Avoid “passed with minor findings” where evidence was insufficient or the scoring method was undefined.
7. Sourcing and quality workflow: from brief to shipment
An audit works best inside a controlled sourcing workflow, scaled to product and supplier risk.
1. Freeze the buyer brief. Record intended users and environment, performance and durability expectations, target markets, ratings and plugs, accessories, finish, claims, packaging, language needs, sales channel, and forecast. Define what cannot change without written approval.
2. Prequalify the supplier. Request legal entity and site details, product-family experience, process and subcontractor maps, organisation chart, relevant certificates, product documents, sample traceability records, and critical test-equipment list. Certificates are leads to verify, not a pass.
3. Plan the audit. Define the SKU, market matrix, critical components, audit criteria, sampling, interview roles, confidentiality rules, and requested documents. Retain the right to select live records rather than reviewing only curated material.
4. Audit and report facts. Walk the process, record document identifier, revision, lot, date, station, and role interviewed. Write observable conditions, not assumptions about intent. “Cord lot X lacked the specified test result” is stronger than “supplier quality is poor.”
5. Agree corrective actions. Require containment, root cause, preventive action, owner, date, evidence, and effectiveness verification. For compliance-sensitive gaps, assess stock already made, in transit, and placed on the market.
6. Approve the production baseline. Align the golden sample, controlled BOM and drawings, artwork, carton, defect classification, inspection plan, test plan, retention samples where agreed, and escalation contacts. The technical evidence must describe this same configuration.
7. Monitor and release deliberately. Use agreed pre-production and in-process checks. Before release, reconcile inspection and test data, quantity, carton markings, lot codes, and documents with the approved baseline. Logistics timing should never become shipment approval.
8. Learn after launch. Trend returns, defects, complaints, service data, and safety signals by lot. Review them with the supplier and feed the findings into change control, corrective actions, and the next audit.
AI image suggestion 3 — Controlled workflow
- Purpose: Show that audit findings feed a repeatable sourcing process.
- Placement: At the end of this workflow section.
- Caption: Supplier approval, pilot production, inspection, and release should operate as one controlled workflow.
- Alt text: Workflow from product specification through audit, pilot assembly, quality inspection, packaging, and shipment readiness.
- English generation prompt: *Clean editorial infographic, horizontal 16:9, six connected stages for a small home appliance private-label workflow: product brief, factory audit, approved components, pilot assembly, quality inspection, packed shipment; modern blue and neutral palette, simple factory and document icons, English placeholder labels only, no brand logos, high readability.*
8. Buyer question checklist
Ask for a live demonstration and sample records, rather than accepting yes/no answers.
Site and ownership
- [ ] What legal entity operates this site, and which processes for this SKU are in-house or outsourced?
- [ ] Can the factory show approved subcontractors, qualification criteria, and controls for outsourced work?
- [ ] Who owns tooling, product data, artwork, and purchase specifications?
- [ ] Has the proposed site, subcontractor, or product family changed since quotation?
Product and engineering
- [ ] Can the team retrieve the current BOM, drawings, critical-component list, revision history, and golden sample?
- [ ] How are changes to material, source, tool, process, firmware, or label assessed and approved?
- [ ] Which changes require buyer approval, a test review, or new evidence?
- [ ] Are voltage versions, plugs, accessories, languages, and wireless variants separately controlled?
Materials, production, and traceability
- [ ] Which components are safety- or compliance-critical, and what acceptance criteria apply?
- [ ] Can today’s line material be traced to supplier, purchase lot, incoming result, and approved status?
- [ ] Are current work instructions understood at each station, and is first-off approval recorded?
- [ ] Are electrical, functional, mechanical, and visual tests appropriate, controlled, and recorded at the agreed traceability level?
- [ ] Can a packed carton be traced back to final test, work order, line, date, and critical-component lots?
- [ ] Are failed and reworked units quarantined, authorised, and retested under a documented rule?
Quality, market evidence, and release
- [ ] Can the supplier show a closed corrective action with root cause and an effectiveness check?
- [ ] Are gauges, testers, and fixtures suitably calibrated or verified, with controlled programs where relevant?
- [ ] Which markets and exact variants does each report, certificate, declaration, or label support?
- [ ] Does the technical file map rules, standards, risks, materials, labels, and instructions to the SKU?
- [ ] Before shipment, who reconciles configuration, final records, carton marks, quantity, and export documents?
9. Common audit mistakes and how to correct them
Auditing the building, not the product. Clean floors and attractive displays are weak proxies for control. Correct it: follow one SKU and lot from receipt through release, comparing it to the approved configuration.
Accepting a certificate or report at face value. It may cover another model, component set, rating, test condition, or standard edition. Correct it: reconcile its scope to the current BOM, model, variant, destination, and revision.
Treating CE, CB, or an NRTL mark as a blanket passport. They serve different purposes and scopes. Correct it: verify the market path, product evidence, and conditions of use for each.[1][7][9]
Ignoring subcontractors. A controlled final-assembly site can depend on uncontrolled moulding, PCB, cord, or test operations elsewhere. Correct it: map external processes, approved sources, specifications, incoming controls, and escalation rights.
Looking only at final inspection. Final testing cannot reliably detect every latent safety or configuration error. Correct it: audit prevention, including approved materials, line clearance, fixture settings, training, process verification, and change control.
Confusing a quality-system certificate with product compliance. A management-system certificate does not prove that a particular appliance meets market requirements. Correct it: audit the system and separately evaluate SKU-specific evidence.
Accepting vague corrective actions. “Improve training” offers no containment or proof. Correct it: require an affected-lot decision, root cause, owner, due date, revised control, training record, and effectiveness result.
Auditing once and assuming permanence. Capability shifts with turnover, shortages, new tooling, production pressure, or supplier change. Correct it: use surveillance triggered by risk, change, performance, and complaints rather than the calendar alone.
10. FAQ: five buyer questions
1. Is an ISO 9001 certificate enough to approve a small appliance factory?
No. It can be relevant evidence about the scope shown on the certificate, but it is not product approval. It does not verify your SKU, supply chain, test evidence, or day-to-day factory performance. Audit SKU-specific controls and records as well.
2. Can a remote audit replace an on-site audit?
It can support early qualification, follow-up, or lower-risk surveillance. It is weaker for observing material flow, segregation, fixture use, operator practice, and unprompted record retrieval. For a new or higher-risk appliance, use an on-site audit where practicable, or combine remote review with independent inspections and targeted evidence checks.
3. What should make a buyer stop production or shipment?
Escalate a plausible serious safety risk, evidence-integrity concern, uncontrolled critical substitution, mismatch between product and compliance evidence, inability to trace affected goods, or a required market document that is missing or inaccurate. Agree stop/release authority and contract remedies before production; obtain market-specific technical and legal advice when needed.
4. Does a CB report mean an appliance can be sold in Europe and North America?
No. The CB Scheme facilitates mutual acceptance of relevant safety reports and certificates, helping move toward “one product, one test, one mark, where applicable.”[9] Market access still depends on applicable law, national differences, current configuration, other regulatory topics, local certification/listing conditions, labels, documents, and responsible-party arrangements.
5. How often should an approved supplier be re-audited?
There is no universal interval. Re-audit when risk or change warrants it: a new product category, critical design/material/process change, new site or subcontractor, repeat defects, serious complaint, unusual production pressure, or weak closure of corrective actions. Stable suppliers can receive lighter surveillance; higher-risk products can justify more frequent oversight.
11. Conclusion: make the audit a controlled decision—and talk to UZYVO
A small appliance factory audit checklist should test repeatable control, not collect reassuring paperwork. The most valuable audit traces an approved SKU through people, parts, process steps, product configuration, and proof. It establishes whether the factory can detect a deviation, contain it, correct it, and document the outcome.
Before your next sourcing decision, prepare a market-and-SKU matrix, define critical components and non-negotiable release criteria, and require complete evidence for any material gap. Where obligations differ by destination, appliance type, electrical configuration, or connected feature, validate current requirements with qualified regulatory, testing, certification, customs, and legal resources.
For an OEM/ODM sourcing brief, an evidence-led factory-audit plan, or a product-quality workflow for your private-label programme, contact UZYVO by email: info@uzyvo.com.
References
- European Commission — CE marking
- Your Europe — Preparing technical documentation
- Your Europe — Conformity assessment
- European Commission — EU General Product Safety Regulation
- European Commission — RoHS Directive
- U.S. Consumer Product Safety Commission — General Use Products: Certification and Testing
- U.S. Occupational Safety and Health Administration — Nationally Recognized Testing Laboratory Program
- Federal Communications Commission — Equipment Authorization Procedures
- IECEE — CB Scheme
- ISO — Quality management principles
- IECEE — IEC 60335-1:2020
- European Commission — Waste from Electrical and Electronic Equipment
AI Image Recommendations
*These are publication-planning prompts only. No new AI images have been generated or added to the website.*
1. Factory audit walkthrough
Purpose: Establish the practical B2B sourcing context at the opening of this guide.
Insertion point: After the introduction.
English caption: Buyer auditor examining appliance production controls and traceability records.
ALT text: Buyer auditor examining appliance production controls and traceability records in a controlled small-appliance manufacturing environment.
AI image-generation prompt: Photorealistic premium B2B manufacturing photograph of an appliance assembly station, calibration records, incoming parts, and a quality-control board without readable text, clean modern Shenzhen-style OEM setting, natural daylight, neutral professional clothing, realistic materials and safe working practices, no trademarks, no readable text, no certification marks, no logos, no visible brand names, 16:9 landscape, documentary sourcing-guide aesthetic.
2. Sample and evidence control
Purpose: Show how a buyer connects the physical product to a controlled requirement and review record.
Insertion point: Beside the sourcing and quality workflow section.
English caption: A controlled product review links the approved sample to the documented buyer requirements.
ALT text: Buyer and quality engineer reviewing an unbranded small appliance sample with a controlled specification sheet.
AI image-generation prompt: High-detail photorealistic factory quality-review scene, buyer and quality engineer examining an unbranded small home appliance sample on a clean workbench with a generic specification sheet, calipers, color chips, packaging components and a sealed reference sample, no readable documents, no logos, no trademarks, no fake test certificates, soft neutral lighting, 3:2 landscape, credible B2B documentation style.
3. Pre-shipment verification
Purpose: Reinforce that shipment checks confirm product identity, packaging, and traceability before release.
Insertion point: Before the conclusion or buyer FAQ.
English caption: Pre-shipment verification checks finished goods against the agreed product and packaging baseline.
ALT text: Inspector checking unbranded small appliance cartons and finished units at a factory shipping area.
AI image-generation prompt: Photorealistic export-quality-control scene in a small-home-appliance factory, inspector checking unbranded finished appliances, instruction leaflets, accessory sets, date-code labels without readable numbers, and closed retail cartons at a clean shipping area, realistic pallet and carton handling, no logos, no readable text, no brand marks, 16:9 landscape, professional B2B factory photography.
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com