Target Keywords: small appliance container loading plan; small appliance container utilization; small appliance moisture protection; small appliance desiccant use; small appliance export carton markings; small appliance barcode verification; small appliance GS1 barcode packaging
Direct answer: A durable distribution-control plan starts before loading: freeze the sellable configuration and carton specification, calculate a feasible load from measured dimensions and mass, protect only the moisture risks actually present, control marking and barcode artwork from approved data, then verify the packed container, documents and scan results against the purchase order. The final configuration, transport route, destination-market requirements and supporting evidence determine what is appropriate—not a generic packing recipe.
Small appliances can arrive with the product intact yet still fail the receiving process. A retailer may not scan a case, a distribution centre may not recognise the barcode, a carton may be too damp to handle confidently, or a container may be released with an unresolved loading discrepancy. These failures span engineering, production, procurement, freight forwarding and receiving. They are best treated as one controlled handoff rather than as separate packing, labelling and logistics tasks.
This guide is for brand owners, importers and sourcing teams buying OEM/ODM small appliances. It focuses on container utilisation, moisture exposure and identification controls—not on choosing a parcel, retail or fulfilment-channel packaging-test protocol. For that distinct test-selection question, see UZYVO’s ISTA packaging-test guide for small appliances. Here, the practical objective is a traceable shipment that can be loaded, identified and received consistently.
1. Define the distribution failure you are trying to prevent
Begin the small appliance container loading plan with a short failure statement, because “avoid shipping damage” is too broad to manage. The statement should identify the item family, sales configuration, carton level, transport mode, destination and receiving channel. For example: *prevent mixed case labels and unstable unused voids during sea-container transport of the approved appliance-and-accessory retail pack to a named distribution centre.* This becomes the anchor for artwork, packing instructions and acceptance checks.
The IMO/ILO/UNECE CTU Code is a useful baseline for this work. It addresses loading and securing cargo in containers throughout an intermodal chain and identifies inadequate securing, overloading and incorrect content declarations as poor packing practices associated with incidents.[1] It is guidance rather than a substitute for a carrier instruction, contract requirement or destination rule. Still, its systems view is valuable: a container is not merely a volume calculation.
Separate failures into four controllable groups:
| Control group | Typical observable failure | Buyer-controlled question | Evidence to retain |
|---|---|---|---|
| Load geometry and stability | Overhang, voids, crush-prone stack or uncontrolled mixed SKU | Does the released loading drawing match the actual carton and pallet? | Approved loading instruction, photographs and pack list |
| Environment | Wet, stained, soft or corroded presentation on arrival | What exposure is credible for this route and product configuration? | Packaging specification, moisture-control decision and inspection record |
| Identification | Unscannable, duplicated or mismatched case identity | Do data, artwork and printed symbols agree with the order? | Master data approval, verification report and sample labels |
| Handover and documentation | Incorrect mass, seal, count or destination data | Who checks each item, when, and against which record? | Loading checklist, VGM submission record and shipping documents |
Controls make a failure mode observable; they do not eliminate all claims. Add controls for the final appliance configuration, such as batteries, glass, plug variants or market-specific markings, and obtain qualified review where needed.
2. Turn carton data into a feasible loading pattern
Small appliance container utilization is not the same as maximising cubic fill. It is the deliberate use of usable space while preserving safe distribution handling, correct identification and a documented gross-mass process. A highly dense pattern that cannot be secured, counted, received or reworked may create more operational risk than a lower-density pattern.
Ask the factory for controlled inputs from the approved production configuration, not estimates copied from a quotation. At a minimum, capture outer-carton length, width and height; gross case mass; inner count; pallet footprint and height if palletised; permitted orientation; stacking constraints; any required dunnage or separation; and SKU/plug/colour segregation. Check that these values agree across the carton drawing, packing list, quotation and label artwork. A change in insert, cable, accessory count or carton board can change both the physical pattern and the retail identity.
Use dimensions to compare permitted orientations, then issue a load drawing with SKU sequence, expected count, label-facing sides and restraint positions. State prohibited conditions, including undocumented substitutions and unsupported gaps. Confirm the actual container’s condition and dimensions with the logistics provider; a nominal container name is not a released specification.
| Planning question | Useful calculation or observation | Decision implication |
|---|---|---|
| How many cases fit geometrically? | Whole-case count by each permitted orientation | Starting point only; exclude unusable spaces and prohibited orientation |
| Is mass distribution sensible? | Compare planned zones and total packed mass with approved limits | Revise pattern or consult the carrier/forwarder before loading |
| Can the receiver identify units? | Check label-facing sides and mixed-SKU boundaries | Add visible identifiers or change the load sequence |
| Can the load be secured? | Map restraint, blocking and void-management positions | Release a material-and-method instruction, not a generic note |
| Does actual loading match plan? | Count, photograph and reconcile before seal | Hold and document deviations before handover |
The verified gross mass (VGM) is a separate control, not a theoretical extension of the load plan. Under SOLAS VGM requirements, the shipper is responsible for providing the verified weight in shipping documents in time for stowage planning, and VGM is a condition for loading a packed container onto a ship covered by the rules.[2] The IMO describes two methods: weighing the packed container, or weighing all packages and cargo items—including pallets, dunnage and securing material—and adding container tare, using a certified method approved by the competent authority where packing was completed.[2] Agree in writing who is the named shipper, who prepares the record and how the value is transmitted.
Image recommendation 1 — released load-plan view
- Purpose and insertion point: Place after this module to make the planning inputs visible before readers move to moisture controls.
- Caption: “Illustrative top-down container layout showing case orientation, SKU zones, restraint points and label-facing sides.”
- ALT text: “Top-down diagram of an appliance-carton container load with labelled SKU zones and securing points.”
- AI image prompt: “Technical editorial illustration, top-down cutaway of a shipping container loaded with plain unbranded small-appliance export cartons, clear labelled zones for two SKUs, arrows showing loading sequence, visible restraint and void-management points, neutral blue and kraft palette, no logos, no numerical capacity claims, clean B2B buyer-guide style.”
3. Assess moisture exposure before specifying a remedy
Small appliance moisture protection should be a risk decision based on product sensitivity, packaging system, route, dwell time, season, handling conditions and destination—not a default promise that every container needs the same consumable. Moisture can matter to paper-based cartons, metal surfaces, electrical assemblies, printed materials, adhesives and a retailer’s acceptance experience. But the appropriate protection must be confirmed against the final materials and distribution conditions.
Map where water or humidity could enter the system. Consider ambient humidity during manufacturing and loading, wet goods or pallets, rain exposure during transfers, container condition, temperature changes during transport, port or warehouse dwell, and the destination’s receiving environment. Inspect whether cartons and pallets are dry before loading; adding moisture-control materials does not correct wet packaging or an unsuitable container. Document the container condition at handover, including obvious holes, odour, standing water, unusual contamination or damaged door seals, and escalate observations through the forwarder or agreed process.
Small appliance desiccant use is a specification decision, not a marketing claim. Define the approved material, placement, installation method, documentation and receiving instruction. Do not set a universal RFQ quantity. Review any proposed desiccant, indicator or liner with relevant suppliers using the actual pack and route; its suitability needs evidence for that system.
| Observed condition or route factor | Sensible control question | Example action that requires validation |
|---|---|---|
| Cartons or pallets show moisture before loading | Is the source isolated and are affected units suitable to ship? | Quarantine, replace, dry only where the packaging specification permits, and record disposition |
| Seasonal humidity or long dwell is anticipated | Which product and packaging components are moisture-sensitive? | Evaluate a barrier, desiccant or process change with the relevant suppliers |
| Container condition is questionable | Can the carrier/forwarder provide an acceptable unit? | Reject or escalate before loading; record condition and decision |
| Receiving team reports recurring damp presentation | Is the issue origin handling, transit exposure, destination storage or a combination? | Trace lot, route, container and condition records before changing materials |
For wood pallets, crates or dunnage, market access may add a separate control. ISPM 15 concerns phytosanitary measures for raw-wood packaging material, including dunnage, while excluding processed wood such as plywood.[5] In the United States, APHIS says imported or transiting wood packaging material must be pest-free, debarked, heat-treated or fumigated, and marked with an ISPM 15 logo; noncompliant material may not be allowed to enter.[6] Requirements and enforcement differ by destination, so confirm the import-market rule and the actual type of wood packaging used. This is not evidence that an appliance itself meets any product requirement.
4. Specify physical packing and securing as a controlled work instruction
A buyer-approved packing instruction should tell the packing team what to do, what evidence to create and when to stop. “Load safely” is not a checkable instruction. Use the final carton drawing and a sample of the actual selling configuration to verify that case labels, orientation arrows, handle openings, appliance accessories and protective inserts remain as approved after normal packing operations.
The work instruction can be organised as a sequence:
- Verify the released SKU, carton revision, quantity and destination label data before loading.
- Inspect container cleanliness, dryness, structural condition and suitability; document exceptions before cargo enters.
- Load in the released orientation and SKU sequence, keeping cartons within defined footprint and stacking constraints.
- Install only the approved blocking, bracing, restraint, liner, dunnage or other materials using the defined method.
- Reconcile carton count, pallet count where applicable, label visibility, final load condition and seal record before release.
The CTU Code covers packers, receivers and unpackers across the intermodal chain.[1] Include receiving feedback: a repeated shifted zone requires a cross-functional instruction review, not only a claim discussion.
Do not invent “pass” thresholds: restraint depends on carton strength, mass, void geometry, container, route and configuration. Control any new material or pattern against the approved reference. Photographs support the record but do not prove every unseen condition or destination requirement.
5. Make export-carton markings unambiguous and market-specific
Small appliance export carton markings have several jobs: help handlers identify the shipment, help receivers match it to an order and, where specified, present handling or destination information. They should be controlled separately from the retail-pack artwork because the carton can carry shipping information that should not be mistaken for consumer-facing claims.
Create one artwork master that distinguishes fixed data from variable data. Fixed data may include brand, model, case count, country-of-origin wording where contractually or legally required, symbols approved for the route, carton dimensions or gross/net mass only when verified. Variable data may include PO number, destination, lot, production date, ship-to code, SKU, pallet number or routing field. Define the format, source system, owner and approval step for each. A handwritten correction on a carton may be legitimate only if your receiving customer accepts it; otherwise it creates a mismatch between physical and electronic records.
| Marking element | Primary purpose | Buyer approval question |
|---|---|---|
| Model/SKU and description | Case-level identity | Does it distinguish variants that could be mixed at receiving? |
| Quantity / inner-pack statement | Count reconciliation | Does it match the released packing specification? |
| PO, destination or routing field | Routing and customer reconciliation | Is the exact field format supplied and approved by the customer? |
| Handling/orientation symbols | Physical handling communication | Are they applicable to the final carton and recognisable for the intended channel? |
| Lot or production trace field | Traceability | Is the coding convention defined and reproducible in the documents? |
| Barcode and human-readable text | Automated and manual identification | Do the encoded data and printed text match the authoritative master data? |
An Incoterms® rule is not a complete quality plan. It allocates costs, risks and obligations, including shipping-related responsibilities.[7] The contract and purchase order should still specify artwork revision, marking approval, inspection rights and duties. Obtain qualified destination-market review for specific marking obligations.
6. Control barcode data, print quality and receiving scans
Barcode failures frequently start with data governance, not with the printer. Small appliance barcode verification should begin by identifying the barcode’s business purpose: retail trade item, outer case, logistics unit, customer-specific routing label or internal warehouse label. Each purpose may need different data, symbology, placement and acceptance rules. Keep the owner of the number allocation clear; do not create or reuse a code because it “looks similar” to another SKU.
GS1 identifies its General Specifications as the core standards document describing how GS1 barcodes and identification keys should be used.[3] For logistical units, the GS1 Logistic Label guideline states that a unique Serial Shipping Container Code (SSCC) is the mandatory element, and scanning it can link physical movement to electronic business messages.[4] An outer case with a GTIN barcode, meanwhile, is not automatically a GS1 Logistic Label when it has no SSCC.[4] That distinction prevents a common error: expecting a retail or case code to perform pallet-level traceability without the agreed logistic-unit identity.
A practical small appliance GS1 barcode packaging control sheet should name the number owner, authorised data source, intended packaging hierarchy, symbology, encoded string, human-readable interpretation, size/placement artwork, printer process and receiving party’s acceptance requirement. Current GS1 specifications should be consulted for the intended application; GS1’s site identifies version 26.0, published January 2026, as the current General Specifications version at the time of writing.[3]
| Gate | What to compare | Evidence / escalation |
|---|---|---|
| Master-data release | SKU, variant, GTIN/other identifier, case count and customer fields | Approved data record; hold conflicting records |
| Pre-production artwork | Encoded data, human-readable text, placement and revision | Artwork approval against master data |
| First-off print | Scanner read and visual content against authorised record | Retain sample and verification result; correct settings before run |
| In-process control | Sampled code readability and variable-data accuracy | Record checks by lot/shift as agreed |
| Pre-shipment reconciliation | Case, pallet/logistics-unit and shipment records | Resolve duplicate, missing or mismatched identities before release |
Verification is more demanding than reading one convenient sample with a mobile or warehouse scanner. Agree any formal verification method, code level, sampling plan, report and disposition. The final customer specification controls; readable but wrong data is still a failure.
Need a cross-functional review of carton, label and factory handoff controls? Share your product configuration, destination and receiving requirements with UZYVO’s OEM/ODM team at info@uzyvo.com. We can help structure the questions and documents for your sourcing process; final compliance still depends on the configuration and destination-market review.
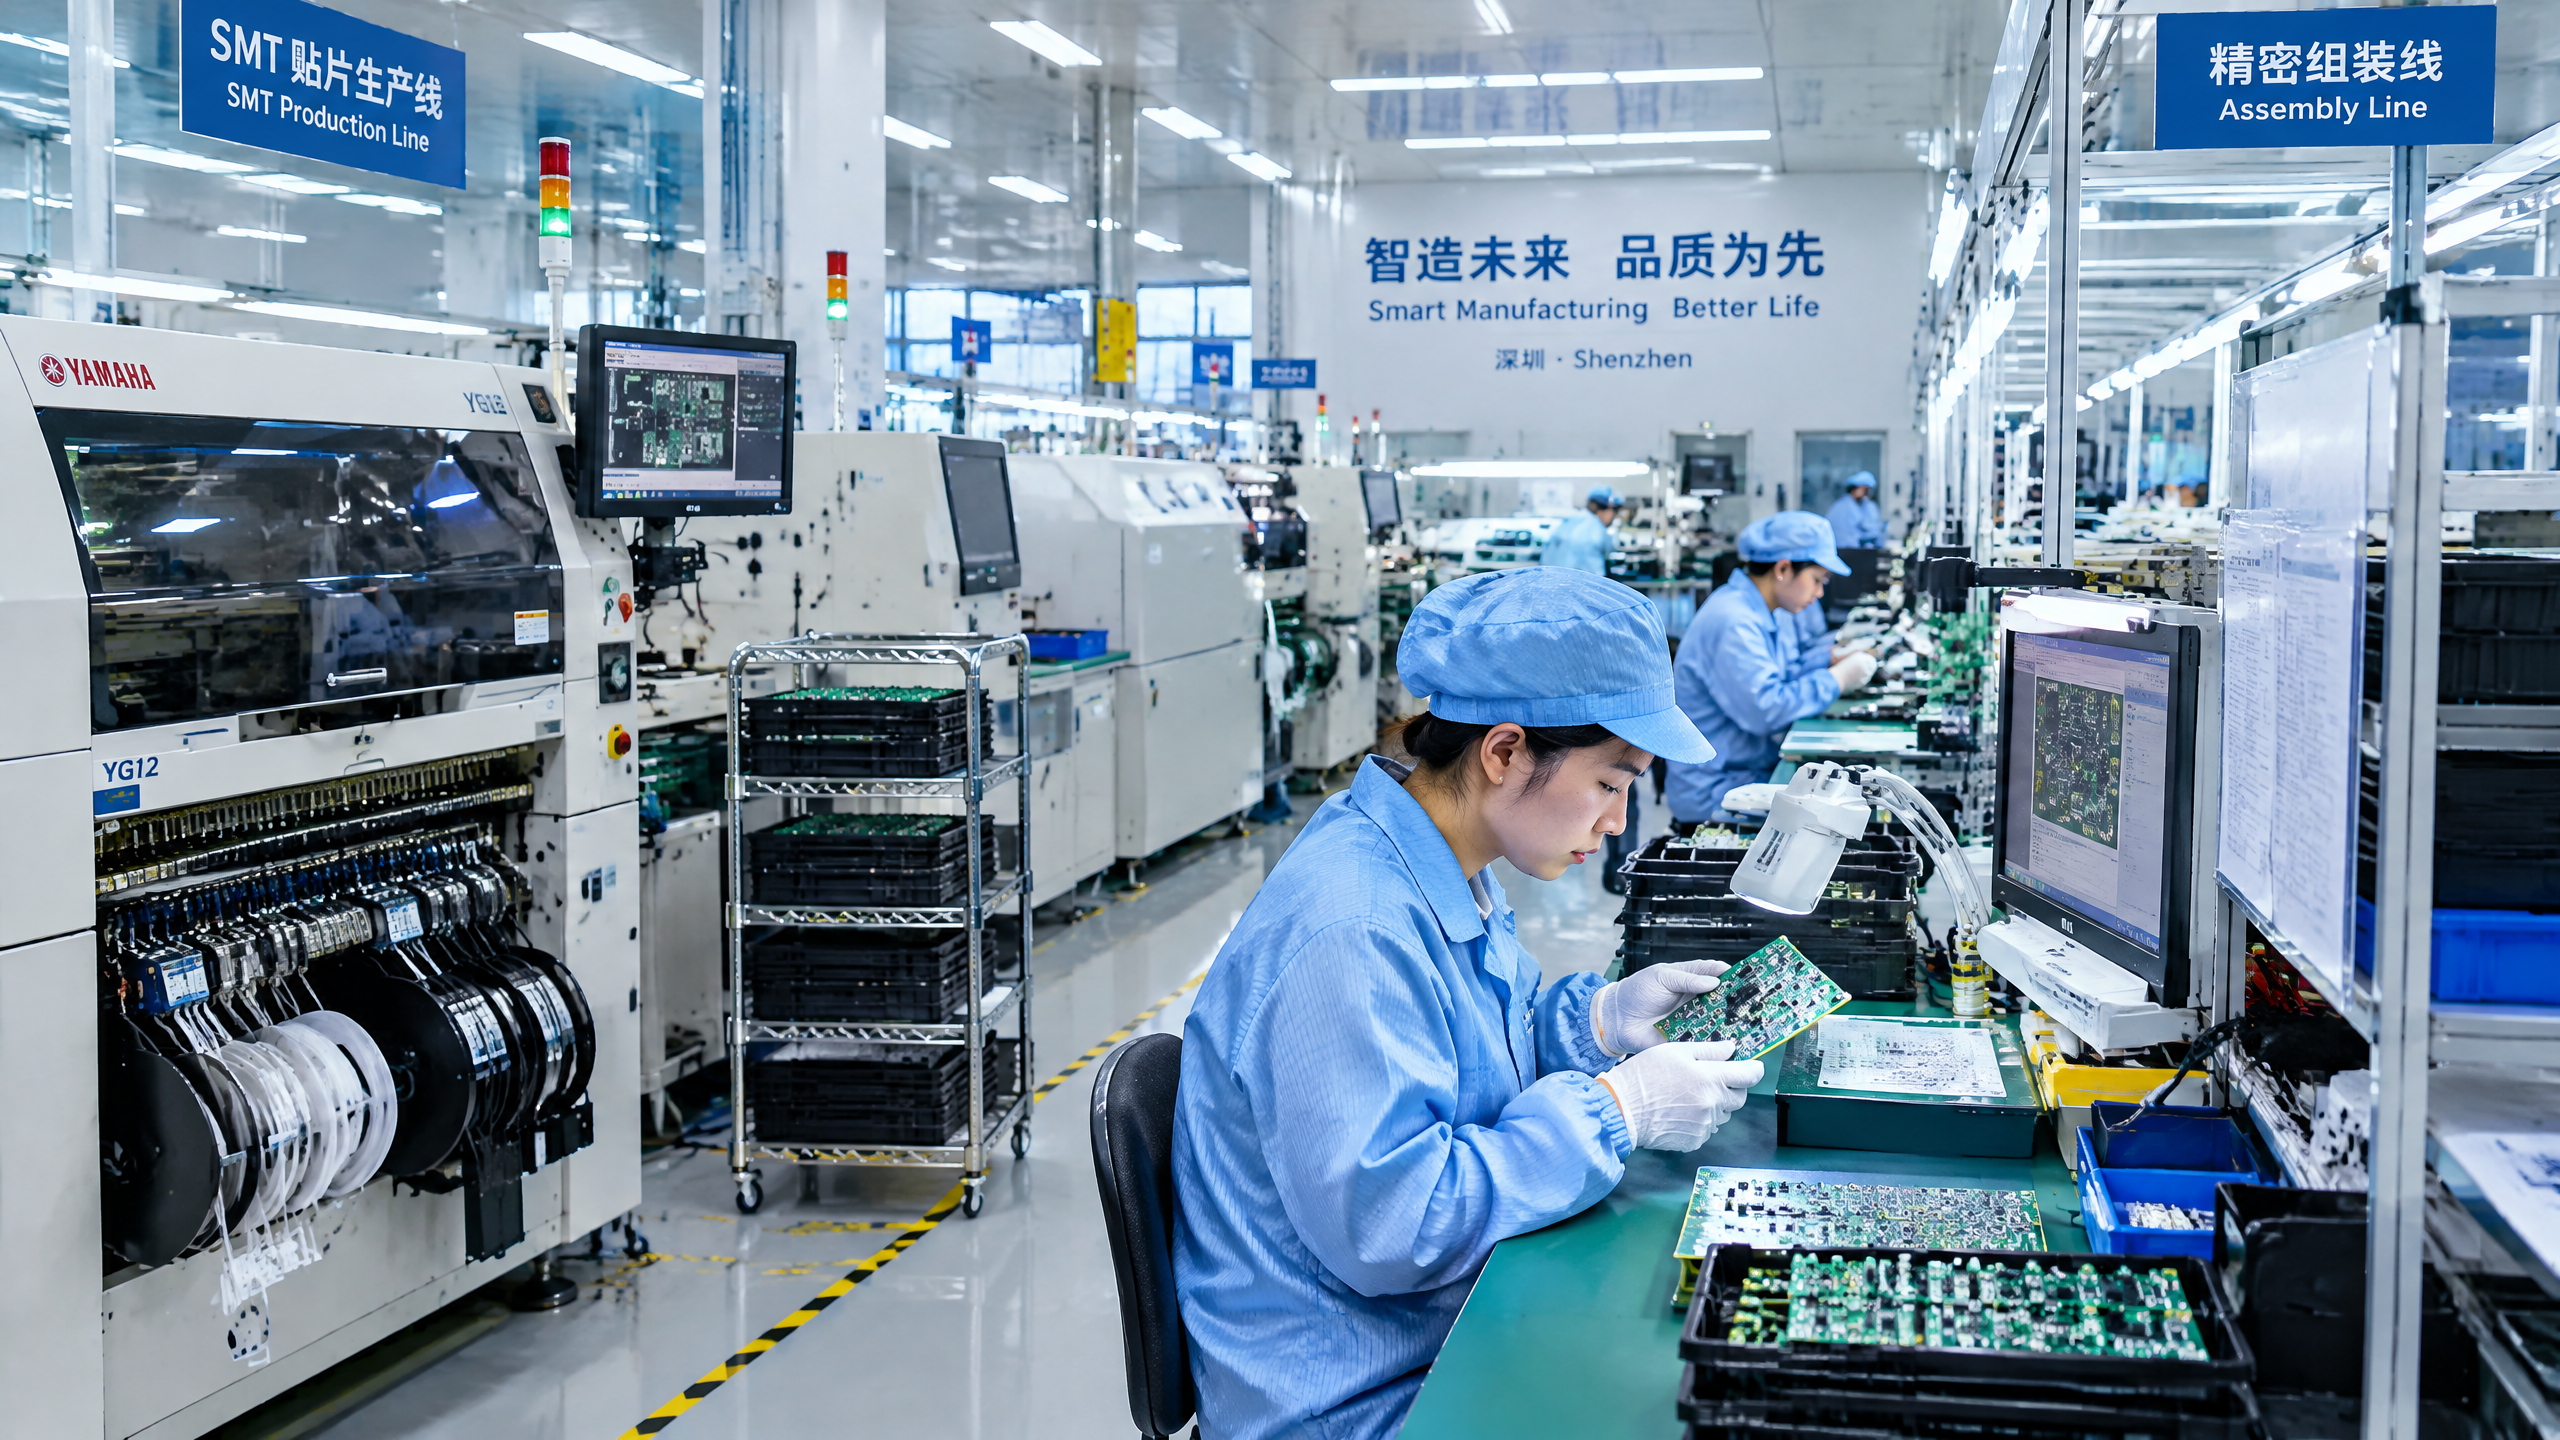
Image recommendation 2 — carton identification checkpoint
- Purpose and insertion point: Place after this module to show the distinction between retail-case information and a logistic-unit label without claiming a particular customer format.
- Caption: “Illustrative packing-station check of carton artwork, human-readable data and a scannable logistics label.”
- ALT text: “Quality operator scanning an unbranded small-appliance export carton label at a packing station.”
- AI image prompt: “Realistic editorial photo illustration of a quality operator at a clean appliance packing station scanning a plain unbranded export carton, visible but unreadable generic barcode and label blocks, laptop with neutral checklist, no company logos, no claims of certification, soft warehouse lighting, B2B sourcing article style.”
7. Build a release gate that links factory, forwarder and buyer
A useful release gate converts many documents into a small number of yes/no decisions. Assign one owner for compiling the file, but do not force that person to certify matters outside their knowledge. For example, the factory may confirm actual carton count and artwork revision; the forwarder may confirm booking and document requirements; the buyer may approve the commercial data and any deviation. The shipper named in the carriage document needs clear responsibility for VGM submission under the applicable process.[2]
| Release item | Check before seal or dispatch | Responsible role should be agreed in advance |
|---|---|---|
| Product/configuration | Model, plug, colour, accessories, manuals and carton revision match released order | Factory and buyer |
| Load | Count, pattern, restraint/void controls and visible condition match instruction | Factory / loading supervisor |
| Moisture decision | Actual packaging and any approved materials match the route-specific plan | Factory with buyer approval as applicable |
| Identity | Carton labels and any logistic-unit labels match approved master data | Factory / label owner |
| Shipping data | Seal, container number, packing list, VGM process and destination references reconcile | Shipper / forwarder / buyer as allocated |
| Exceptions | Photos, description, disposition and approver are recorded | Named deviation owner |
The purchase order should state failure disposition: hold, relabel, repack, replace, split quantity or record a concession. Do not silently correct identity data after loading and shipping records exist; a controlled exception is more traceable than a workaround.
Use a single shipment identifier to tie together the release checklist, photos, packing list, seal record, barcode verification evidence and post-arrival feedback. Retain records long enough to investigate the commercial and quality lifecycle established in your agreements. The appropriate retention period is contractual and market-specific; do not assume a universal legal rule.
8. Inspect at the right points and use receiving feedback
Inspect where correction remains possible. Origin inspection can check cartons, artwork, variable data, count, sequence and visible securing, but does not prove unseen transit conditions or future market acceptance. Agree sampling, criteria, scope, report and cost in advance.
At receiving, ask the warehouse or customer to capture a small standard data set: seal condition, container condition on opening, obvious moisture signs, count discrepancy, label scan result, SKU/lot identity and photographs where a discrepancy exists. This turns anecdotal feedback into an input for corrective action. If the same supplier, route or artwork revision repeatedly appears, compare the records rather than assuming the cause.
There is a useful division of work with the separate packaging-test topic. A test programme may help demonstrate performance of a specified package under a defined test sequence; container control confirms that the approved package was actually configured, identified and loaded as released. Neither removes the need for the other when risk warrants both. Do not claim a package has passed a named test unless the actual final configuration, method, laboratory/report and acceptance criteria support that statement.
Receiving feedback may also reveal a commercial-interface failure: a customer expected a pallet label but received only a case barcode; a ship-to reference was missing; or a cross-dock flow needed SSCC data that was never agreed. These are not printer “defects” alone. Revisit the order master data, customer routing guide, label hierarchy and pre-shipment scan check.
9. Use change control to prevent recurrence and hidden substitution
Distribution controls weaken when a familiar product is treated as unchanged. Changes in carton board, insert geometry, inner quantity, plug, accessory, label stock, print technology, pallet source, loading site, route, warehouse or customer can alter the risk picture. The buyer should require advance notification and approval criteria for changes that affect the released packing, marking or loading plan.
A concise change request should answer: what is changing; which SKUs, orders and dates are affected; why; which drawings, artwork, bill of materials and work instructions change; what evidence was reviewed; what receiving or regulatory impact was considered; and who approved it. Require a revised revision identifier. A new carton size with an old loading drawing, or a new barcode with an old master-data mapping, is a predictable source of distribution failure.
When investigating an issue, distinguish containment from root-cause correction. Containment protects the next shipment—such as holding a label batch or requiring an additional count check. Root-cause correction changes the governing data, instruction, training or material control so the condition does not recur. Verify effectiveness with a later shipment record or receiving outcome rather than declaring success because a corrective-action form was closed.
Image recommendation 3 — receiving-side reconciliation
- Purpose and insertion point: Place after this module to reinforce that distribution control continues through destination receiving.
- Caption: “Illustrative receiving check reconciling carton identity, shipment record and container-opening condition.”
- ALT text: “Warehouse receiver scanning an appliance carton while checking a shipment record beside an opened container.”
- AI image prompt: “Professional editorial warehouse scene at destination receiving: worker in generic safety vest scans an unbranded small-appliance carton, open shipping container in background, clipboard with generic checklist, cartons dry and intact but no performance claim, no logos or readable proprietary data, documentary B2B photography style.”
10. Buyer FAQ: decisions that should be agreed before booking
Does every container of appliances need desiccant?
No universal answer is reliable. Decide small appliance desiccant use from the final product and packaging materials, credible route and dwell conditions, container condition, destination and supporting evidence. First prevent loading wet or unsuitable packaging. If a moisture-control product is proposed, document its approved placement, relevant material information, installation method and receiving instructions. Consult the packaging supplier, forwarder and destination requirements where applicable rather than copying a quantity from another SKU.
Is an outer-case barcode the same as a logistics label?
Not necessarily. GS1 notes that cartons and outer cases often carry a barcode encoding a GTIN, but labels without an SSCC are not GS1 Logistic Labels.[4] Agree what unit needs to be identified: consumer item, case, pallet or another logistics unit. Then confirm the exact data, code format, placement, electronic-message relationship and receiving scan requirement with the customer.
Can a container loading plan replace packaging testing?
No. They address different decisions. This guide controls execution of a released load: dimensions, mass process, securing, moisture decision and identification. A packaging-test programme evaluates a defined package under a selected method. The appropriate combination depends on the final appliance, packaging, route, channel and buyer/customer requirements. See the linked ISTA packaging-test guidance for its separate test-selection scope.
Who is responsible for carton marking under Incoterms® 2020?
The answer depends on the selected rule and the parties’ contract. Incoterms® allocate particular costs, risks and obligations, but they do not replace the purchase-order specification or identify all product and document requirements.[7] State the rule and named place precisely, then allocate artwork approval, variable-data supply, printing, inspection, VGM process, forwarder handover and any destination-specific review in the contract documents. Seek qualified advice for the transaction and market involved.
11. Conclusion: make distribution controls visible before shipment
The strongest shipment plan is not the one with the most materials or the tightest possible fill. It is the one that makes the final product configuration, carton revision, load pattern, moisture decision, marking data and scan results visible to the people who must act on them. Start with measured, approved inputs; plan utilisation around stability and receiving as well as volume; treat moisture controls as route- and configuration-specific; and distinguish retail/case identification from logistics-unit traceability.
Before the next booking, ask the factory to assemble the controlled carton drawing, packing specification, loading instruction, marking artwork, barcode master-data approval, verification evidence, VGM responsibility, release checklist and exception route. Use receiving data to close the loop, and control changes before a revised carton or label enters production. For factory process context, review UZYVO’s factory capabilities and the buyer-facing FAQ.
Ready to align an OEM/ODM shipment-control pack with your product and market? Email info@uzyvo.com with the appliance type, final configuration, destination, channel and receiving requirements. UZYVO can help you organise a practical sourcing conversation; final applicability must be confirmed for the final configuration and destination market.
References
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com