Selecting an OEM small appliance manufacturer is a product-risk decision. The supplier must repeatedly turn a specification into safe, conforming, consistent goods under your brand; a convincing sample alone does not prove control of components, changes, records, or corrective actions.
This framework is for European and North American private-label buyers. It is sourcing guidance, not legal, customs, or certification advice. Requirements differ by product, market, sales channel, claims, and economic operator.
1. Concise answer
Choose an OEM small appliance manufacturer by testing fit, proof, control, and accountability—not by price, a generic certificate, or a sample.
- Fit: Does the supplier have relevant engineering and manufacturing experience for this product architecture and target market?
- Proof: Are its claims supported by current, product-specific test evidence, process records, and an auditable site?
- Control: Can it lock the approved design and bill of materials (BOM), qualify critical inputs, prevent unapproved changes, and trace finished goods to inspections and components?
- Accountability: Are product ownership, commercial scope, quality responsibilities, documentation ownership, and escalation rules clear before tooling or mass production?
Start with a written product-and-market brief, use the same weighted scorecard for every candidate, and make nomination conditional on closing material gaps. Treat safety and compliance as release gates rather than negotiable add-ons.
For the EU, CE marking is a manufacturer declaration that a product meets applicable requirements, not a general government approval or indication of origin.[1] US and Canadian obligations vary by item and jurisdiction. Ask: “What evidence supports this configuration in each market, and how will production remain aligned?”
2. Why the choice matters to private-label buyers
With private label, your brand goes on the product. A blender, kettle, hair dryer, fan, heater, vacuum, or grooming device can involve mechanical hazards, electrical insulation, overheating, materials, instructions, packaging, software, and radio functions. Failure can cause returns, retailer disruption, rework, or withdrawal.
Tooling, plug variants, carton performance, incoterms, lead times, and component substitutions affect total cost. A low ex-works price can be outweighed by late testing, redesign, or field failures.
Market-access roles cannot be outsourced by assumption. Under EU GPSR, manufacturers must meet general safety requirements, conduct internal risk analysis, and prepare technical documentation. An own-brand party may be treated as the manufacturer in defined circumstances.[3] Map the manufacturer, importer, EU responsible person where required, distributor, and marketplace seller.
In the United States, requirements remain product-specific. CPSC notes that certain household electrical products and construction characteristics can present substantial hazards, while its guidance does not replace obligations under applicable law and standards.[6] A connected appliance also needs an FCC assessment: intentional transmitters generally require Certification, while equipment containing only digital circuitry may use the Supplier’s Declaration of Conformity (SDoC) route.[5]
Buyer principle: A sample, a test report, and a quality system are different forms of evidence. Require all three, then verify that they cover the same approved product configuration.
AI image suggestion 1 — Factory due-diligence scene
- Purpose: Show an audit from incoming parts to final release.
- Placement: After this section, before the scope-and-definitions module.
- Caption: “A credible supplier audit follows the product and its records through the factory.”
- Alt text: “Buyer and quality engineer reviewing a small appliance assembly line and inspection records.”
- English generation prompt: “Photorealistic editorial image of a European private-label buyer and an Asian factory quality engineer reviewing a countertop small-appliance assembly line, visible work instructions, test station, labelled component bins, natural industrial lighting, realistic documentary style, no brand logos, no readable proprietary data.”
3. Scope and definitions: OEM, ODM, and the configuration being bought
An OEM arrangement generally means manufacturing to the buyer’s specification. An ODM arrangement begins with a supplier-developed design that the buyer adapts. A new heating module, mould, firmware, connector, or safety feature can turn an ODM adaptation into a new project.
The commercial label is less important than the configuration. Do not evaluate “a kettle” or “a cordless vacuum.” Evaluate the precise combination of:
- model, markets, channels, and languages;
- rated voltage, frequency, plug, power range, and architecture;
- materials, contact parts, motor, heater, charger, electronics, firmware, and connectivity;
- accessories, claims, labels, manuals, and packaging; and
- BOM, drawings, software revision, golden sample, test plan, and change-control baseline.
This prevents a frequent error: accepting evidence for a look-alike model. A report has decision value only when its description, ratings, critical components, construction, standard edition, deviations, and destination align with the planned product. For a product family, ask which variants are included and why.
The EU Low Voltage Directive (LVD) covers electrical equipment within 50–1,000 V AC and 75–1,500 V DC, including household appliances.[2] A product can also engage product-safety, radio, chemicals, energy, labelling, or language requirements. CE marking is compulsory only where legislation requires it and must not be applied outside that scope.[1] Build a market-specific applicability matrix rather than treating “CE” as a stand-alone test.
For EU electrical and electronic equipment, RoHS restricts hazardous substances; equipment with an electrical or electronic component must comply unless specifically excluded.[4] WEEE, food-contact, battery, chemical, and energy rules may also matter. North American requirements vary too. The OEM can supply facts, but the buyer should identify who makes the final market determination.
Define quality separately from compliance. Compliance asks whether the product meets applicable requirements; quality asks whether every unit achieves the promised function, finish, reliability, and packaging standard. A plausible technical file cannot prevent returns from leaks, scratches, inconsistent controls, or confusing instructions.
4. The evaluation framework: eight evidence-based dimensions
Use one scorecard for every candidate. Score against evidence, identify the source, and distinguish “demonstrated” from “claimed.” A weighted score must never outweigh a hard stop such as unsupported safety evidence, unclear ownership, or refusal to permit an audit.
1) Product and engineering fit
Ask how the supplier converts a product requirement document into drawings, BOMs, prototypes, validation, and production instructions. Seek experience in the actual architecture, not merely a similar outer shape. Review hazards, foreseeable misuse, tolerances, serviceability, and manufacturability.
Confirm control of moulds, electronics, firmware, and critical subassemblies. Ask how safety-critical parts are identified, changes trigger re-evaluation, and custom tooling, artwork, and product data are owned.
2) Legal entity and commercial integrity
Confirm the contracting entity, site, payment beneficiary, and scope of work. Reconcile names on the quotation, bank instructions, export documents, audit, and test reports. The U.S. International Trade Administration recommends careful partner selection and continued due diligence to reduce problems, loss, and liability.[10]
Require a detailed quotation covering model scope, incoterm, tooling, tests, packaging, spares, validity, and exclusions. Clarify rights to designs, tooling, documentation, test data, and firmware. Use qualified legal advice for contracts, IP, sanctions, customs, and disputes.
3) Compliance competence and document integrity
A capable supplier begins with the product and markets, not a generic certificate folder. Ask it to map applicable requirements, tests, risk analysis, labels, instructions, documentation, and traceability. Independently confirm the route with appropriate advisers, laboratories, certification bodies, retailers, or authorities.
For every report, check the issuer, laboratory and accreditation scope, report number, date, product description, ratings, clauses tested, critical components, deviations, and applicant. Ask whether post-test changes occurred. ILAC directories can help locate laboratories accredited for a particular test or inspection.[8]
The IECEE CB Scheme can support electrical-product evaluation through mutual acceptance of CB reports and certificates among participating national certification bodies.[7] It is not automatic acceptance in every market. Confirm national differences, local marks, surveillance, or additional tests.
4) Supply-chain control and responsible sourcing
Map critical inputs: heaters, motors, chargers, batteries, cords, plugs, controls, PCBs, plastics, coatings, contact parts, and packaging. Identify single sources, approved alternates, incoming inspection, qualification, and counterfeit controls. Require advance notice of material, sub-supplier, process, site, or component changes.
For US imports, traceability is also a trade-risk issue. CBP enforces the UFLPA rebuttable presumption for goods made wholly or in part in the Xinjiang Uyghur Autonomous Region or by a UFLPA Entity List entity, and it publishes importer guidance.[9] This is fact-specific, not a category-only exercise. Maintain a risk-based record of supply-chain due diligence and seek current professional advice where appropriate.
5) Manufacturing process and capacity planning
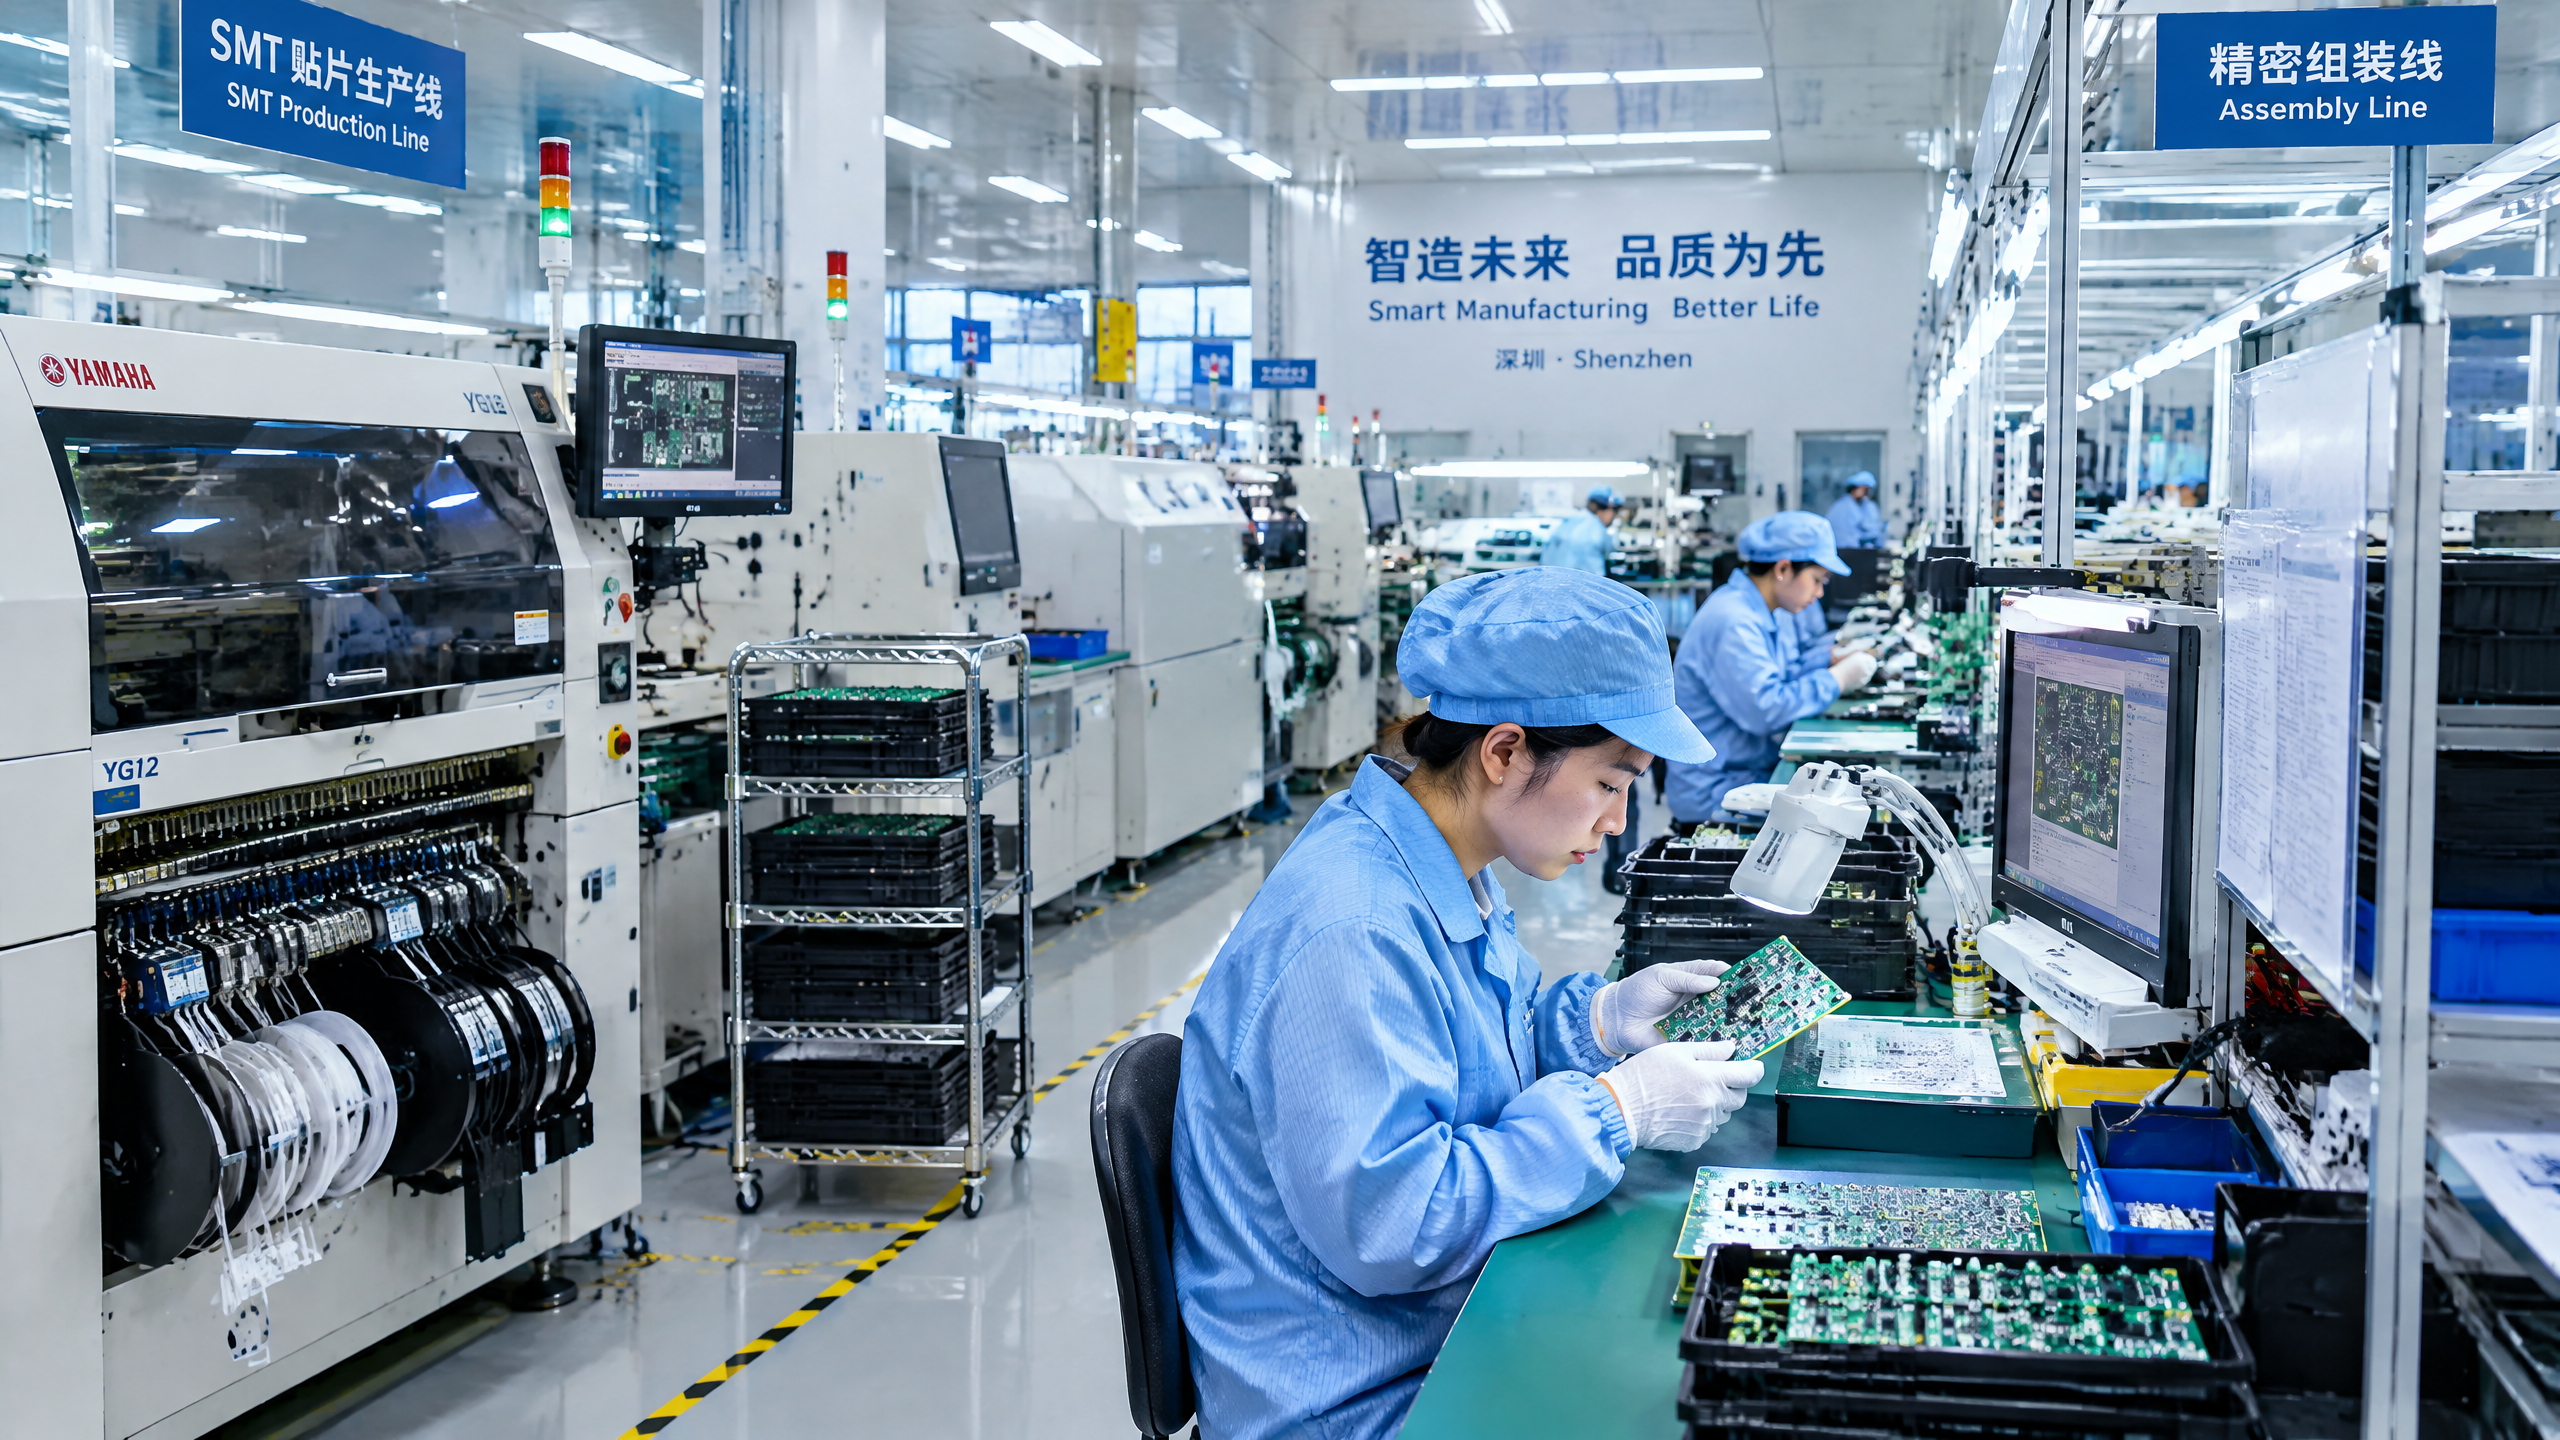
Observe the proposed route from receiving through assembly, functional testing, final inspection, packing, storage, and shipment. Look for controlled work instructions, trained operators, fixtures, error-proofing, maintenance, calibration, segregation of rejected goods, and environmental controls relevant to the appliance.
Do not rely on an unsupported monthly-capacity claim. Ask which lines, shifts, yield, critical-part lead times, competing programmes, and peak-season limits underpin the plan. Require a capacity model with dependencies, triggers, owners, and contingencies.
6) Quality-management effectiveness
Audit the loop rather than the logo. Review incoming, in-process, and final inspection criteria; non-conformance records; corrective and preventive action (CAPA); calibration; and internal-audit follow-up. Ask to see how a failed test is contained, who approves disposition, how rework is controlled, and how corrective-action effectiveness is checked.
Set measurable acceptance criteria before production: functionality, cosmetic limits, tolerances, relevant leakage or temperature parameters, cycle tests, lot coding, carton checks, and sampling. For AQL or another plan, name the method, inspection level, defect classification, lot rule, and disposition.
7) Programme management and communication
Assess the people who will execute the work. Can they maintain revision control, provide clear written change notices, flag risks early, and coordinate engineering, procurement, quality, packaging, and logistics? Require a milestone plan covering samples, pilot builds, validation, production release, inspection, booking, and shipment, with one accountable owner and an escalation route.
Written minutes, revised drawings, signed sample approvals, and documented deviations are production controls. Require an engineering-change order (ECO) that assesses the effect of every material change on safety, compliance, cost, tooling, lead time, packaging, and existing inventory.
8) Service, resilience, and after-launch support
Ask what happens if a component is discontinued, a retailer reports a defect cluster, or a field return needs investigation. Review retention samples, spare parts, complaint intake, failure analysis, repairability where relevant, and cooperation on corrective action or withdrawal. The OEM should be able to reproduce the shipped configuration and retrieve the relevant lot records.
A credible partner explains how it detects a signal, contains stock, identifies root cause, verifies action, and communicates evidence. Put those duties in the quality agreement.
5. Compliance and risk: make evidence a release gate
Manage compliance as a living evidence package. Before final design, list each destination, channel, electrical variant, claim, and technical feature. For each, record the owner, rule source, required test or document, timing, sample, cost, and final approver. Revisit the matrix whenever the product, component, site, country, or claim changes.
For EU household appliances in scope, the LVD provides a central electrical-safety framework. Only references to harmonised standards published in the Official Journal give presumption of conformity with its safety objectives.[2] The Commission also notes that the manufacturer determines conformity under the LVD; the directive does not require notified-body assessment for these products.[2] That is not a reason to accept unsupported declarations. It is a reason to review the underlying risk analysis, standards, test evidence, manufacturing consistency, and technical documentation carefully.
GPSR requires internal risk analysis and technical documentation containing the information needed to demonstrate safety, with information proportionate to product complexity and risks.[3] Turn this into programme discipline: identify hazards and foreseeable use, specify mitigations, assign verification methods, record results, and communicate residual risks in instructions and warnings.
For electronics, link RoHS evidence to the approved BOM rather than accepting a generic letter. The Commission identifies ten restricted substances and notes that exemptions may apply and evolve.[4] Track declarations, material data, tests where justified by risk, and any exemption assessment by component number and revision. For US products, assess CPSC, state, customer, electrical-safety, labelling, and FCC obligations as relevant. FCC says the responsible party for SDoC must be in the United States and must provide test reports and other compliance information when requested.[5]
Use five controlled release folders:
- Design inputs: PRD, drawings, BOM, claims, critical parts, risk assessment, and standards matrix.
- Verification evidence: product-matched reports, sample configurations, construction photos, and results against acceptance criteria.
- Market documents: declarations, labels, instructions, product identifiers, and required operator information.
- Manufacturing evidence: golden sample, control plan, work instructions, calibration, traceability, and change log.
- Shipment evidence: lot or serial records, final-inspection outcome, pack-out verification, and non-conformance closure.
Every release item needs a named owner and pass/fail decision. An ambiguous report, untranslated warning, or unassessed substitute component means the product is not released. Keep records versioned by model and revision, with continuing buyer access.
AI image suggestion 2 — Compliance evidence map
- Purpose: Explain that compliance is connected product evidence, not a single certificate.
- Placement: After the release-folder checklist in this section.
- Caption: “Compliance evidence remains linked to the approved configuration and production records.”
- Alt text: “Small appliance, bill of materials, test report, risk register and shipment records connected in a documentation map.”
- English generation prompt: “Clean editorial infographic of a generic countertop appliance connected to a risk analysis, bill of materials, accredited laboratory test report, product label, assembly control plan and shipping carton; navy, warm gray and subtle orange; no logos, no invented certification marks, professional B2B sourcing style.”
6. Decision table: compare suppliers before negotiating price
The following scorecard is a starting point. Adjust weights for your product risk: connected, heated, battery-powered, or liquid-handling appliances may justify more emphasis on engineering, compliance, and traceability. A high weighted score never overrides a hard-stop finding.
| Dimension | What to verify | Example evidence | Suggested weight | Hard-stop example |
|---|---|---|---|---|
| Product and engineering fit | Relevant process and control of critical parts | Design review, BOM control, prototype plan | 15% | Cannot explain safety-critical design or change path |
| Compliance readiness | Market route and product-matched evidence | Applicability matrix, reports, file index | 20% | Evidence is unrelated or unverifiable |
| Quality-system effectiveness | Prevention, inspection, CAPA, calibration, traceability | Control plan, records, CAPA example | 18% | No reliable lot traceability or containment |
| Supply-chain control | Critical supplier qualification and change control | Approved vendors, incoming controls, change log | 12% | Opaque or unapproved critical substitution |
| Manufacturing execution | Lines, fixtures, maintenance, capacity planning | Line walk, work instructions, capacity model | 12% | Proposed process cannot be demonstrated |
| Commercial and IP clarity | Scope, tooling/data rights, price basis, terms | Detailed quotation, draft agreement | 10% | Contracting entity or ownership unclear |
| Programme management | Revisions, milestones, escalation | Project plan, ECO procedure | 7% | No accountable owner or change system |
| After-sales resilience | Failure analysis, records, corrective-action support | Complaint workflow, retention-sample plan | 6% | No field-quality investigation process |
Score from 1 to 5, multiply by the weight, and record the evidence and confidence level behind each score. A “5” should be independently verified and product-relevant; a “3” may be documented but unvalidated for your exact model; a “1” is unsupported or inadequate. Conduct a two-stage award: shortlist through documentary review, then validate the leader with an audit, sample build, evidence review, and corrective-action plan.
Compare total landed and lifecycle cost only after normalising scope. Include configuration, packaging, incoterm, tooling, test cost, inspection, freight assumptions, duties and taxes where applicable, warranty provision, rework risk, and spares. If one quote includes a defined, evaluated controller and another names an unspecified alternative, those prices are not comparable.
7. Sourcing and quality workflow: from brief to post-launch control
A reliable workflow builds evidence in the order decisions are made. Reconstructing evidence after a failed inspection is slow and expensive.
- Build the brief. Define user need, markets, volume range, variants, claims, quality level, and launch window. Attach a PRD, drawings or benchmarks, packaging brief, and known requirements.
- Pre-qualify suppliers. Request entity data, relevant experience, process map, quality documentation, initial compliance matrix, and commercial questionnaire using the same format for every candidate.
- Audit and review technically. Follow the production route, interview engineering, purchasing, production, quality, and project staff, and review a real CAPA and engineering change. A tour without records is not due diligence.
- Freeze the validation plan. Before tooling and pilot, agree sample definition, tests, reports, critical suppliers, pilot objectives, deviations, and change criteria. Test production-intent samples where possible.
- Approve the manufacturing baseline. Lock drawings, BOM, labels, packaging, firmware, work instructions, control plan, golden sample, and inspection criteria. Require written approval and impact assessment for any “equivalent” component proposal.
- Control production and shipment. Use suitable incoming, in-process, and final checks. Verify the product, carton marks, manuals, plug/voltage variant, accessories, and lot or serial code against agreed criteria.
- Monitor field performance. Set return-reason codes, complaint escalation, sample retrieval, CAPA timing, and supplier reviews. Trend issues by lot, component revision, market, and date.
The quality agreement should define release authority, change-notification thresholds, audit and inspection rights, non-conforming material, rework, traceability, records access, CAPA, confidentiality, and recall cooperation. Ask qualified counsel to tailor the agreement to the transaction and jurisdictions.
AI image suggestion 3 — Controlled production workflow
- Purpose: Visualise how an approved design becomes a traceable shipment and feedback loop.
- Placement: After the workflow steps in this section.
- Caption: “Controlled launch connects product approval, inspection, release, and field feedback.”
- Alt text: “Horizontal workflow from appliance specification and prototype through testing, production inspection, shipment and feedback.”
- English generation prompt: “Sophisticated flat-vector B2B workflow infographic with six stages: product specification, prototype sample, laboratory testing, controlled assembly, final inspection, shipment and feedback loop; generic small kitchen appliance icons; dark blue, white and subtle orange, spacious European industrial-design aesthetic, no logos or certification marks, English labels only.”
8. Buyer question checklist for supplier meetings and audits
Use these questions in meetings and on the factory floor. Ask for a document, record, or live demonstration after every answer.
Product and engineering
- Which current products use a comparable heating, motor, battery, liquid, or connectivity architecture?
- Who owns each drawing, mould, PCB layout, firmware element, and tooling item? What rights do we receive?
- Which parts are safety- or performance-critical, and how are they approved and controlled?
- What design reviews, prototype stages, and validation gates apply to this model?
- What counts as a change, and who approves it?
Compliance and documents
- Which markets and channels does this configuration target, and what assumptions support the applicability matrix?
- Which evidence is model-specific, and which is only component or platform evidence?
- May we verify reports with the issuing laboratory or certification body?
- What are the report dates, standards, ratings, sample descriptions, deviations, and critical components?
- Who will retain technical documentation, reports, declarations, and production records?
- What labels, languages, warnings, operator details, and online-listing data are required by market?
Factory, quality, and supply chain
- Can we trace one lot from incoming parts to packed cartons and inspect the records?
- How are incoming, work-in-process, finished, rework, and rejected goods identified and segregated?
- Can you show a recent CAPA for a comparable defect and demonstrate how its effectiveness was checked?
- How do you calibrate test equipment and prevent use after a missed calibration date?
- Which parts are single-sourced? What is the contingency plan?
- How are supplier, material, site, process, and firmware changes assessed and communicated?
- Can you complete a mock traceability exercise from carton code to critical component lots and inspection results?
Commercial execution and support
- What does the quote include and exclude, line by line?
- What is the launch critical path, including buyer decisions and purchased-part lead times?
- Who can stop shipment, approve a deviation, or escalate a field problem?
- How will the OEM support failure analysis, spares, corrective action, or a market withdrawal?
Record gaps as before nomination, before tooling, before production, or post-launch improvement. Missing safety evidence or uncertain ownership should never be deferred beyond award.
9. Common mistakes—and better buyer behaviours
Selecting on unit price first. A low quote may omit tooling, testing, defined components, packaging, or inspection. Better: use a structured request for quotation and reconcile every difference before price comparison.
Treating CE or a certificate scan as universal approval. CE is a manufacturer declaration, while voluntary certificates may not be recognised evidence for EU market-surveillance or customs checks.[1][2] Better: verify the market route and the product-specific evidence behind it.
Approving a manual sample without locking configuration. A sample can differ from production in parts, settings, workmanship, or packaging. Better: approve a golden sample together with the BOM, drawings, critical components, and change rule.
Auditing the reception area instead of the process. Wall certificates do not show whether rejects are segregated or tests are calibrated. Better: follow the product flow and inspect records, observations, and CAPA closure.
Asking for “all certificates.” This invites document dumping and obscures what is missing. Better: begin with features, markets, and claims, then build an applicability matrix with named deliverables.
Allowing informal substitutions. A different thermostat, resin, charger, cable, adhesive, radio module, or firmware can affect safety, function, or compliance. Better: require advance approval and a documented impact assessment.
Forgetting the digital product. An app, wireless module, remote control, or update can affect radio compliance, cybersecurity, privacy, service, and version control. Better: assign hardware, firmware, app, cloud, and data responsibilities in the release plan.
Treating the purchase order as the whole contract. It may leave data, tooling, traceability, field investigation, and recall cooperation unclear. Better: align a product specification, commercial agreement, and quality agreement.
Stopping due diligence after the first shipment. Components, capacity, personnel, and regulations change. Better: keep supplier scorecards, periodic evidence review, change logs, and field-performance monitoring.
10. FAQ: five buyer questions about choosing an OEM small appliance manufacturer
1. Is an OEM manufacturer better than an ODM manufacturer?
Neither is inherently better. OEM can provide more control when you bring a developed specification; ODM can reduce development time when a platform genuinely fits. Decide based on configuration control, differentiation, validation impact, and rights to tooling, IP, and product data—not the label alone.
2. What certifications should I ask for?
Ask first for a product-and-market applicability assessment, then request evidence relevant to that exact configuration. Depending on the item and destination, this may include reports, declarations, technical-file inputs, component evidence, labels, instructions, and manufacturing records. Do not assume one document covers every market, plug, power rating, radio function, or future revision. Confirm current requirements with qualified specialists and relevant official or third-party bodies.
3. Can a third-party test report replace a factory audit?
No. A report evaluates the stated sample and scope; an audit assesses whether the supplier can manufacture that configuration consistently and control change. Both are valuable but answer different questions. Verify report authenticity and scope, use relevant accredited laboratories where appropriate, and audit the controls that keep shipped goods aligned with the tested sample.
4. When should inspections take place?
Plan them before the purchase order. Depending on risk and maturity, use pre-production review, first article, during-production inspection, pre-shipment inspection, and occasional post-arrival checks. Tie each to defined criteria, sampling, decision authority, and a process for failed results. Inspection complements supplier process control; it cannot replace it.
5. Who is responsible if a private-label appliance has a safety issue?
Responsibility depends on the product, facts, contracts, and destination law. It may involve the manufacturer, importer, brand owner, responsible person, distributor, or marketplace seller. Map roles before launch, obtain jurisdiction-specific legal and compliance advice, and make sure your contract supports rapid access to traceability and corrective-action evidence.
11. Conclusion: select the partner, then govern the product
The right OEM small appliance manufacturer can show how a product requirement becomes a controlled shipment: market-specific evidence, an approved configuration, qualified components, trained production, measurable inspection, traceability, and a disciplined field response. The buyer’s task is to demand evidence early, compare candidates consistently, and keep governance active after launch.
Use this framework to shortlist, audit, validate the exact product, and award only when critical gaps are closed. Because obligations vary by appliance and market, keep current regulatory confirmation, legal review, and product-specific evidence inside the launch plan.
UZYVO welcomes structured OEM/ODM discussions with private-label buyers sourcing for European and North American markets. Share your product brief, target markets, configuration requirements, and requested evidence package. Email [info@uzyvo.com](mailto:info@uzyvo.com).
References
- European Commission — CE marking
- European Commission — Low Voltage Directive
- Regulation (EU) 2023/988 on general product safety
- European Commission — RoHS Directive
- Federal Communications Commission — Equipment Authorization Procedures
- U.S. Consumer Product Safety Commission — Household Electrical Products
- IECEE — CB Scheme
- ILAC — Mutual Recognition Arrangement and Signatories
- U.S. Customs and Border Protection — Uyghur Forced Labor Prevention Act
- International Trade Administration — Perform Due Diligence
AI Image Recommendations
*These are publication-planning prompts only. No new AI images have been generated or added to the website.*
1. OEM supplier due diligence
Purpose: Establish the practical B2B sourcing context at the opening of this guide.
Insertion point: After the introduction.
English caption: Private-label buyer reviewing oem controls with factory engineers.
ALT text: Private-label buyer reviewing oem controls with factory engineers in a controlled small-appliance manufacturing environment.
AI image-generation prompt: Photorealistic premium B2B manufacturing photograph of a structured supplier-audit review with an appliance sample, process map, and neutral quality records, clean modern Shenzhen-style OEM setting, natural daylight, neutral professional clothing, realistic materials and safe working practices, no trademarks, no readable text, no certification marks, no logos, no visible brand names, 16:9 landscape, documentary sourcing-guide aesthetic.
2. Sample and evidence control
Purpose: Show how a buyer connects the physical product to a controlled requirement and review record.
Insertion point: Beside the sourcing and quality workflow section.
English caption: A controlled product review links the approved sample to the documented buyer requirements.
ALT text: Buyer and quality engineer reviewing an unbranded small appliance sample with a controlled specification sheet.
AI image-generation prompt: High-detail photorealistic factory quality-review scene, buyer and quality engineer examining an unbranded small home appliance sample on a clean workbench with a generic specification sheet, calipers, color chips, packaging components and a sealed reference sample, no readable documents, no logos, no trademarks, no fake test certificates, soft neutral lighting, 3:2 landscape, credible B2B documentation style.
3. Pre-shipment verification
Purpose: Reinforce that shipment checks confirm product identity, packaging, and traceability before release.
Insertion point: Before the conclusion or buyer FAQ.
English caption: Pre-shipment verification checks finished goods against the agreed product and packaging baseline.
ALT text: Inspector checking unbranded small appliance cartons and finished units at a factory shipping area.
AI image-generation prompt: Photorealistic export-quality-control scene in a small-home-appliance factory, inspector checking unbranded finished appliances, instruction leaflets, accessory sets, date-code labels without readable numbers, and closed retail cartons at a clean shipping area, realistic pallet and carton handling, no logos, no readable text, no brand marks, 16:9 landscape, professional B2B factory photography.
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com