Target Keywords: small appliance test record; small appliance serial number traceability; small appliance lot traceability; small appliance production line audit; small appliance quality escalation matrix; small appliance corrective action request; small appliance root cause analysis
Direct answer: A useful appliance quality-data system links the exact finished unit or defined lot to its controlled configuration, incoming materials, assembly and test evidence, shipment allocation, and any complaint or nonconformity. It then gives named people authority to contain product, investigate the cause, implement a corrective action, and verify whether that action worked. The right identifier level, records, audit depth, and escalation route depend on the final product configuration, safety relevance, supply chain, evidence available, and destination market; qualified review is needed where regulatory obligations may apply.
A passed inspection report is not, by itself, a quality-control system. When a retailer reports intermittent heating, a warehouse finds a rating-label mismatch, or a customer complaint suggests a possible safety concern, the commercial question becomes immediate: which units are affected, where are they, what changed, and who can stop further distribution? If documents cannot connect those questions, data has been collected without becoming decision-ready.
This buyer guide is for private-label brands, importers, and procurement teams sourcing small appliances through OEM/ODM arrangements. It covers lot and serial traceability, production-line audit evidence, and corrective-action governance. It deliberately does not recreate a guide to negotiating component-substitution clauses. For contractual controls that prevent unapproved changes, see Preventing Surprise Component Substitutions. Here, the emphasis is on using records already generated through production to contain a problem and learn from it.
1. Define the decision that traceability must support
Traceability is not the act of printing a code. It is the ability to retrieve a defined answer to a defined question. Before selecting a label format or demanding more spreadsheets, establish the scenarios the buyer needs to manage: release of a production lot, a customer-return investigation, a component alert, a missing test record, a stock quarantine, or a market-safety escalation.
The EU General Product Safety Regulation (GPSR) requires manufacturers to ensure products bear a type, batch, serial number, or other identification element, subject to practical placement alternatives. It also requires procedures for series-produced products to remain in conformity and, in applicable circumstances, corrective measures for dangerous products [1]. Those provisions do not prescribe one universal database for every appliance. They underline why an identifier has commercial value only when it points to retrievable, current evidence.
For each product family, define the traceable object, required precision, events to record, source-system owner, and expected evidence for an internal trace exercise.
GS1 frames end-to-end traceability around identifying, capturing, and sharing information across the “who, what, when, where and why” of lifecycle events. Its guidance distinguishes critical tracking events from the data elements describing them and notes that systems need to support upstream and downstream queries [2]. A small-appliance buyer need not adopt every GS1 technology to apply this discipline. The useful principle is to agree on the event and the evidence before collecting fields.
| Buyer decision | Question the records must answer | Minimum useful linkage |
|---|---|---|
| Hold an open production run | Which work orders and packed units may share the suspected condition? | Work order, line/date or lot, test status, stock location |
| Investigate a field complaint | What configuration and build evidence applies to the returned unit? | Unit or lot ID, model revision, complaint record, production and test record |
| Assess a component alert | Which finished lots used the affected incoming material? | Supplier/component lot, issue-to-line record, finished-lot mapping |
| Stop a channel release | Which shipments and customers received affected inventory? | Finished lot or serial range, carton/pallet and shipment allocation |
An identifier is a retrieval key, not proof of safety, conformity, or cause. Conclusions still depend on the final configuration, actual records, technical investigation, and destination-market obligations.
2. Select serial, lot, and configuration identifiers that fit the appliance
Small appliance serial number traceability distinguishes an individual finished unit and retrieves its configuration and relevant build history. It can suit repairable products or programs where warranty and returned-unit analysis need unit-level resolution. The identifier must be readable and consistently captured by customer service, warehouses, and repair partners.
Small appliance lot traceability can be more proportionate for high-volume, low-value products if a well-defined lot links every included unit to the same controlled build and production context. A lot definition must be unambiguous. “March production” is usually too broad. A work order, line, shift, date window, and final-configuration revision may be more meaningful, but only if the factory can demonstrate that the included units actually share that history.
Neither approach is automatically superior; compare the containment need with record capability.
| Design choice | Serial-number model | Lot-based model | Buyer control to require |
|---|---|---|---|
| Retrieval precision | Potentially identifies one finished unit | Identifies a defined population | Written identifier specification and lookup demonstration |
| Data volume | Higher; each unit needs a record or association | Lower; one record covers a defined group | Retention and access owner agreed before production |
| Field-service use | Can support unit-specific repair history | May require extra product attributes | Service team can read and record the identifier |
| Containment scope | May allow narrower review when records are complete | Scope follows the validity of the lot boundary | Drill validates the actual scope, not the intended scope |
| Misuse risk | Duplicate, unreadable, or unlinked serials create false confidence | Over-broad or poorly defined lots create over-containment | Reconciliation of labels, database, and shipment data |
Treat model, revision, electrical variant, firmware where relevant, packaging revision, and destination-market artwork as configuration attributes. A serial or lot should lead to an approved configuration record; otherwise the system cannot distinguish evidence for different builds.
The GPSR’s identification and technical-documentation provisions apply according to the product and legal scope, and other rules may be relevant to a particular appliance [1]. For that reason, final marking, record-retention, and market-access decisions should be reviewed against the exact finished configuration and destination market—not copied from a similar SKU.
3. Build the small appliance test record around evidence, not a tick box
A small appliance test record identifies what was checked, against which controlled specification, on which product or sample, by whom or what process, with what result, and what happened on failure. A signature alone is not evidence.
Separate four layers of evidence:
- Release criteria: the approved specification, work instruction, drawing, limit, sample, or acceptance rule used at that operation.
- Execution evidence: the result, sample quantity or unit/lot identity, date/time where meaningful, operator or system identifier, and equipment reference.
- Exception evidence: the nonconformity number, disposition, rework or retest basis, approver, and affected scope.
- Change context: the current product revision, controlled process revision, component or supplier change reference, and effective date.
The exact test plan varies by product architecture and applicable standards. Do not assume that a named test or report for another model covers the final model. Require the process document, record version, equipment status, and unit/lot-to-result link; this supports documentary integrity, not a regulatory conclusion.
| Record element | What a buyer should ask to see | Why it matters during investigation |
|---|---|---|
| Product identity | Model, revision, electrical version, and unit or lot reference | Prevents a result being applied to a different build |
| Test reference | Controlled work instruction and revision | Shows what method and criterion were in effect |
| Result and disposition | Actual result/status and a link to any exception | Reveals whether failure was contained or merely overwritten |
| Equipment/process reference | Asset ID, calibration/verification status as applicable | Helps assess whether the measurement route was controlled |
| Approval trail | Named role, date, and release condition | Establishes who accepted the batch and on what basis |
Do not permit “pass” to be the only durable field for a critical control. Retain a measurable result or auditable system link where practical; for attribute checks, retain the sampling rule, acceptance decision, inspector/system reference, and nonconformity link. Records should be controlled and retrievable without relying on one employee’s files.
4. Turn the production line audit into a repeatable evidence review
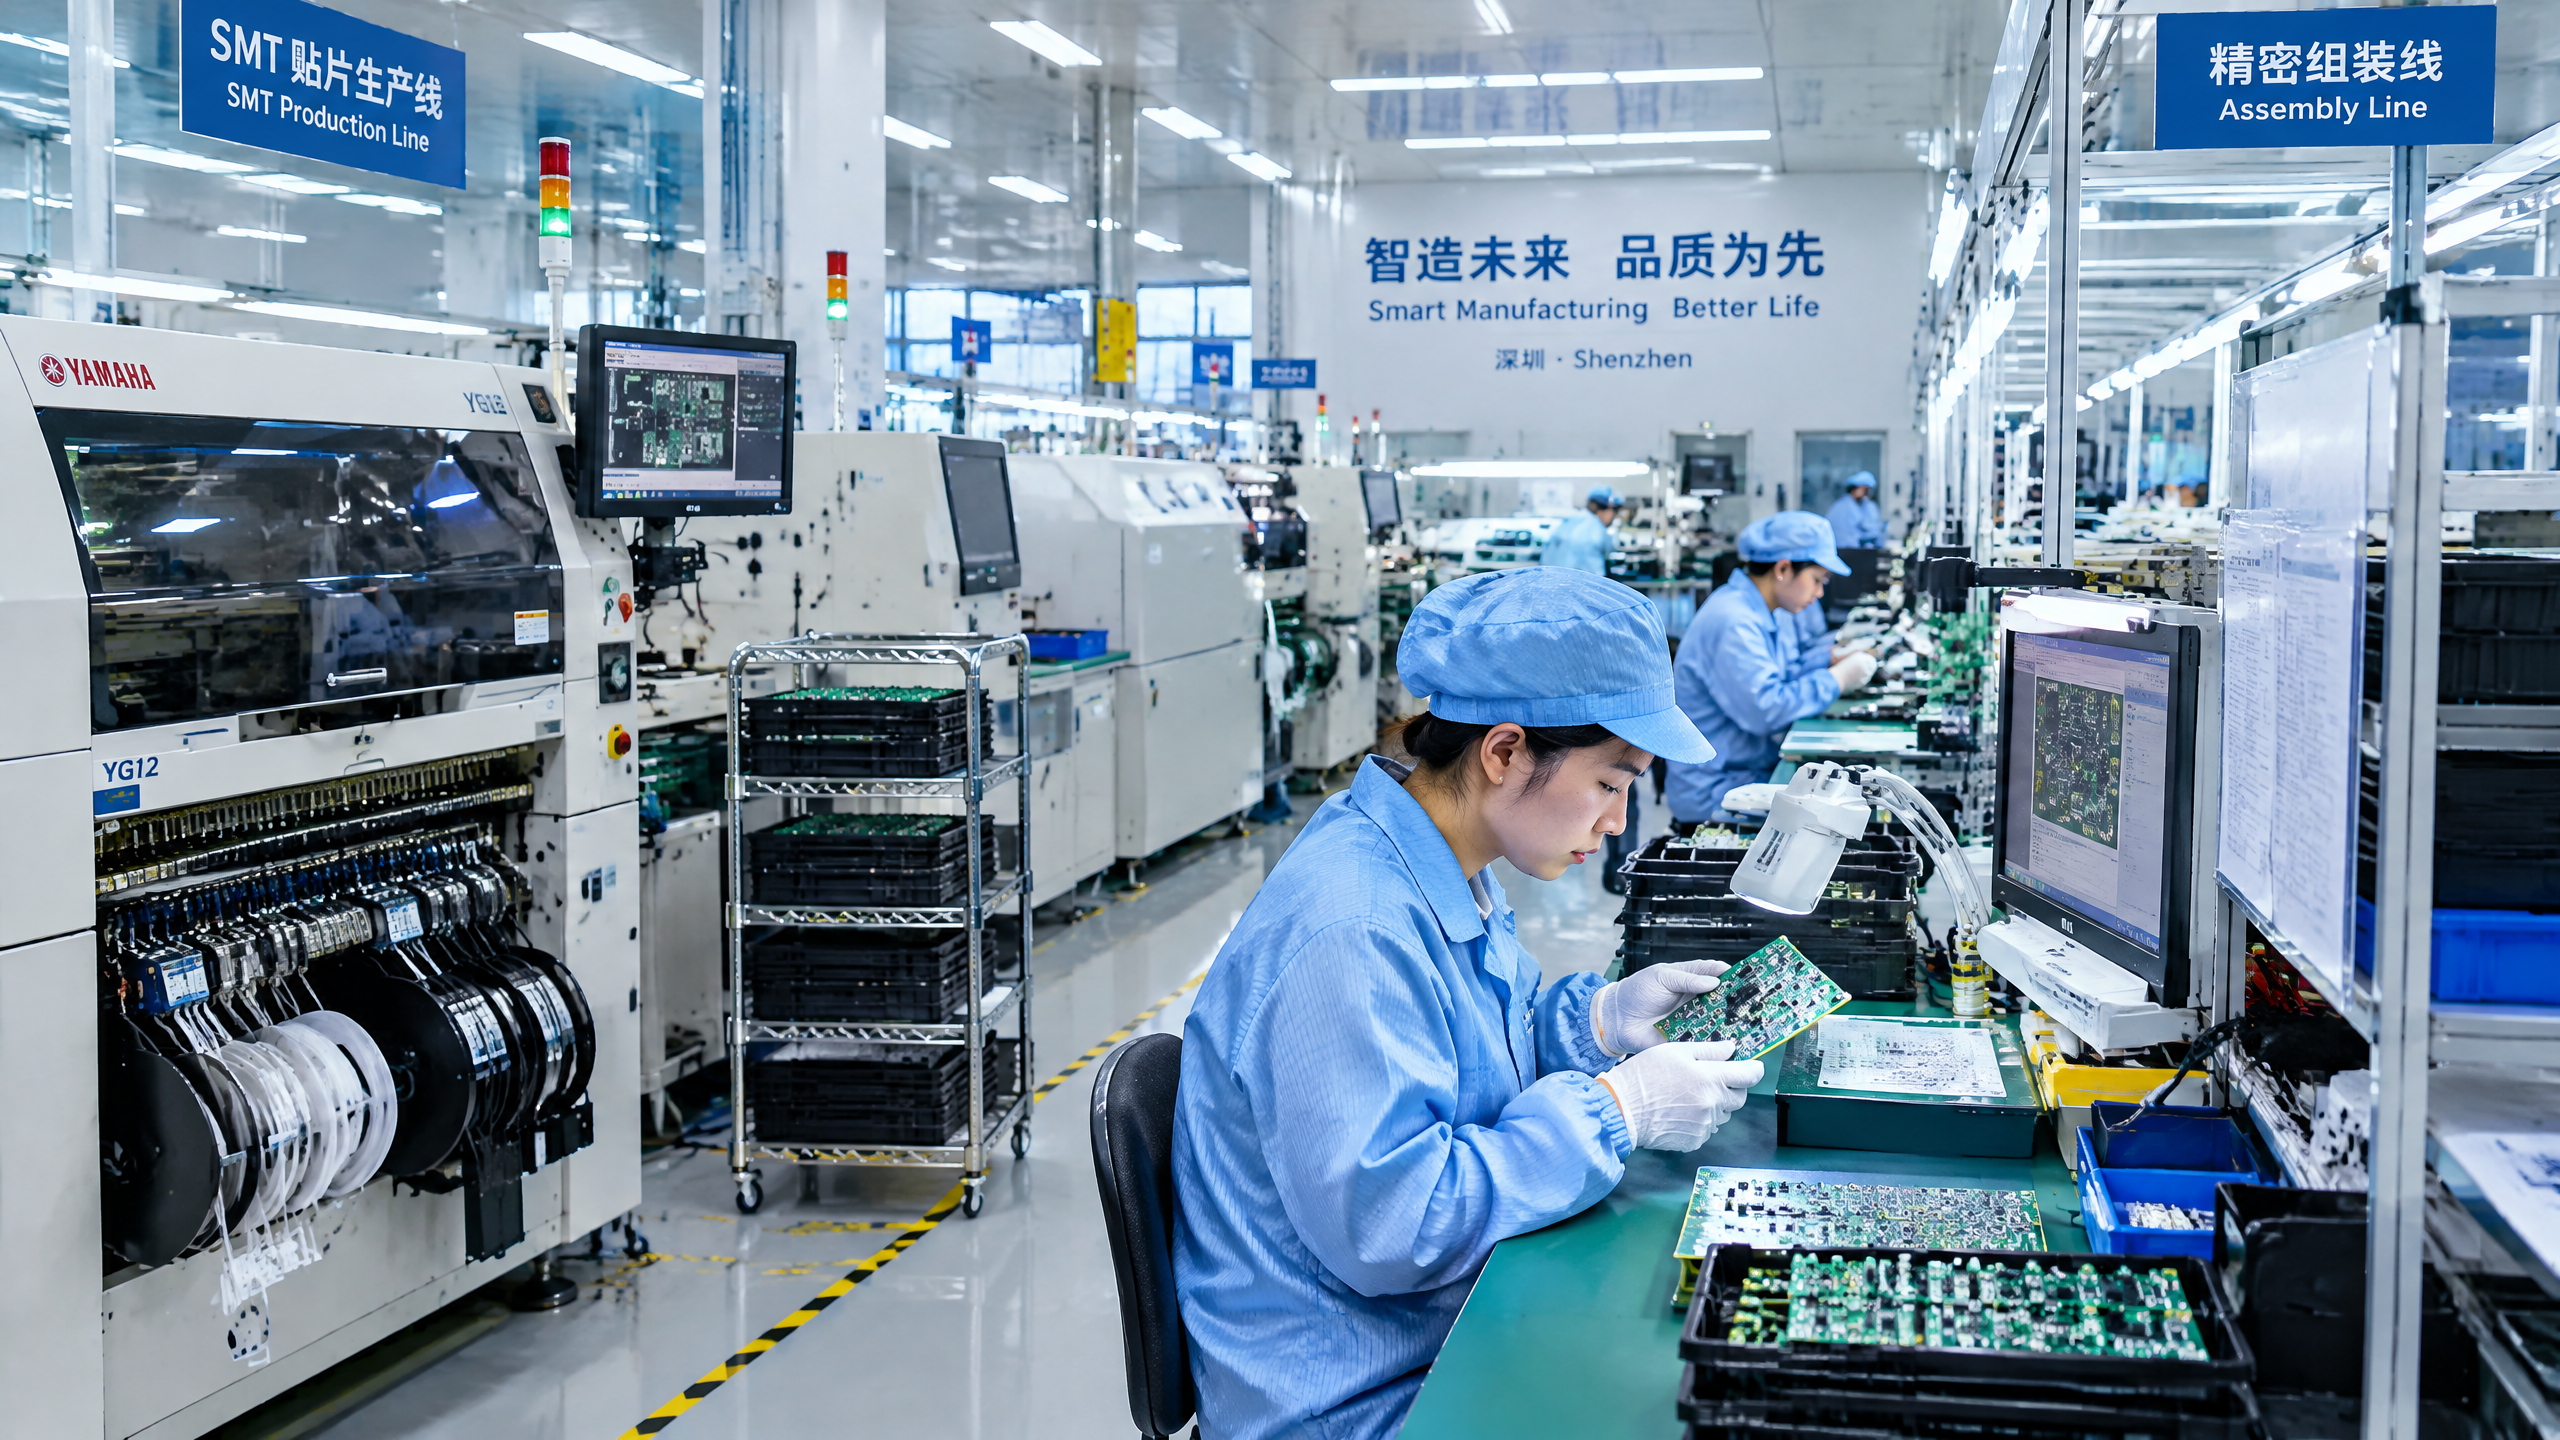
A small appliance production line audit is most useful when it tests whether the controlled process is actually being followed during the visit, rather than scoring the factory’s appearance. ISO 19011 provides guidance on audit principles, managing audit programs, conducting management-system audits, and auditor competence; it is guidance, not certification in itself [3]. A buyer may use that orientation to design a focused second-party line audit without representing that the audit certifies a product or factory.
Plan the audit around risks and evidence trails. Select a running SKU or completed lot and trace it from approved documents through materials, line controls, test records, packaging, and release. Record facts separately from conclusions.
| Audit area | Evidence to examine | Constructive audit question |
|---|---|---|
| Controlled build | Current BOM, work instruction, sample, line display | Does the line have the current approved version and can operators identify it? |
| Incoming-to-line link | Incoming labels, issue records, segregation practice | Can the supplier connect relevant material lots to the work order? |
| In-process controls | Test stations, records, defect handling, rework route | What happens physically and digitally when a unit fails? |
| Identification and packing | Product label, carton code, packaging artwork, packing record | Can a packed unit be linked to its controlled configuration and production scope? |
| Release and shipment | Final inspection, release authority, dispatch allocation | Who can block release and how are affected units separated? |
Do not rely on photographs alone. Ask the auditee to retrieve a selected record during the normal workflow and reconcile it to a physical sample where reasonable. Record time, person, source system, document revision, and limitations. Document nonconformities as requirement, objective evidence, scope, containment, owner, and due date—not as an untested root-cause theory.
For an overview of how buyer brief, sample approval, and production controls can be coordinated, review UZYVO’s OEM / ODM workflow. The workflow does not replace an audit plan or destination-specific review.
5. Create an escalation matrix that gives data a route to action
A small appliance quality escalation matrix decides what happens when facts are incomplete, contradictory, or potentially significant. It prevents two damaging responses: treating every cosmetic issue as a crisis, or allowing a credible safety or traceability signal to wait for a routine weekly meeting.
Design the matrix around severity, reach, and uncertainty: potential consequence, affected products/channels/markets, and gaps in identification, test evidence, or configuration history. These are response prompts, not a legal conclusion or pre-set recall decision.
| Trigger example | Immediate control | Accountable decision role | Required next record |
|---|---|---|---|
| Isolated cosmetic defect within agreed acceptance criteria | Log trend; no automatic hold | Quality lead | Inspection/trend record |
| Repeated functional failure in a defined lot | Quarantine identified stock and stop release pending review | Factory quality owner with buyer quality lead | Nonconformity and lot-scope check |
| Missing or conflicting critical test/identity evidence | Hold affected scope until record integrity is resolved | Buyer/factory release authority | Evidence-gap assessment and disposition |
| Field complaint that may indicate a product-safety issue | Preserve unit/data; initiate urgent cross-functional triage | Brand product-safety/commercial owner | Incident log, traceability query, advice record |
| Authority, retailer, or component-supplier alert | Activate contact tree and controlled containment | Named market and technical leads | Event chronology and response decisions |
Name primary and backup people, decision rights, response targets, and external-advice triggers. State the action behind each severity level: whether the factory may rework, ship, or dispose of held goods, and who can pause listings or notify distributors.
Where products are sold in the United States, CPSC states that manufacturers, importers, distributors, and retailers have a duty to immediately report certain defect, risk, and noncompliance information; its guidance says a company must report within 24 hours of obtaining reportable information and encourages reporting even while investigation continues in appropriate cases [5]. The same guidance states that reporting does not automatically mean a corrective action is necessary [5]. This illustrates why an internal matrix must flag issues early rather than try to resolve legal or risk questions through a delayed factory discussion. EU and other market routes differ; seek qualified advice for the specific facts and destination.
Need to connect a production record, audit finding, and shipment hold into one buyer-controlled workflow? Discuss the supplier-side evidence route with UZYVO’s factory-capabilities team, or email info@uzyvo.com. UZYVO can support sourcing and production collaboration; market-specific legal and certification determinations require appropriately qualified review.
6. Issue a corrective action request that can be closed, not just answered
A small appliance corrective action request (CAR) addresses a documented nonconformity or adverse trend. It is not generic supplier feedback or a substitute for immediate containment. It preserves a shared factual record and separates correction of current product from action on the underlying cause.
A high-quality CAR contains the following sections:
- unique ID, issue date, requester, supplier contact, and related purchase order or product family;
- factual problem statement, including the requirement and objective evidence;
- affected product identity, known lots/serials, locations, and uncertainty boundaries;
- immediate containment: stock hold, sort, re-inspection, shipment control, or other action actually taken;
- investigation plan and cause-analysis method;
- proposed correction and corrective action, owner, due date, and needed change approvals;
- effectiveness-verification method, review date, and closure authority; and
- attachments or links to photos, records, returned units, audit observations, and test evidence.
A CAR should state what is not known. “Finished-lot scope pending reconciliation” is better than assuming every shipment, or one unit, is affected. Operator retraining may be a correction but does not by itself show that the process cause was removed.
ISO 9001:2026 describes a quality-management framework that includes documented information, operational control, performance evaluation, and continual improvement [4]. It does not mean an ISO certificate guarantees that a supplier’s particular response is adequate. Buyers should assess the response against the affected final configuration, records, and agreed requirements.
7. Conduct root-cause analysis before selecting a lasting remedy
Small appliance root cause analysis should explain why the observed condition escaped the controls that were meant to prevent or detect it. “Operator error,” “supplier issue,” or “carelessness” is rarely an actionable root cause on its own. Those statements may identify the last visible event but not the system condition that allowed recurrence.
Choose a method that suits the evidence: five whys for a bounded issue, fishbone for cross-functional factors, or a fault tree for paths to a defined failure. Test the explanation against records and physical evidence. Preserve representative units before destructive analysis where needed.
| Investigation question | Evidence that may help | Weak conclusion to avoid |
|---|---|---|
| Did the product meet the controlled build? | BOM revision, photos, label, component and assembly records | “It looked normal on the line” |
| When did the condition first appear? | Lot, shift, test, inspection, shipment, and complaint chronology | “It started after the customer complained” |
| Why did the planned control not detect it? | Work instruction, test method, limits, equipment, sampling and failure disposition | “Inspection should have caught it” |
| What changes coincide with the event? | Change logs, material receipts, tool maintenance, process and staffing records | “There were no changes” without checking records |
| What scope could share the cause? | Traceability query, line usage, shipment allocation, return data | “Only this unit is affected” without a scope basis |
Separate root cause, contributing factors, and containment limitation in the report. A cause might concern an unclear work instruction; a contributing factor could be a poorly designed fixture; a containment limitation might be missing unit-to-shipment data. Each needs a different action. This separation prevents the CAPA from ending with a single corrective measure that leaves a known evidence gap unresolved.
Do not let the wish for a rapid closeout override evidence quality. For a potential safety or regulatory matter, obtain appropriate technical, legal, and destination-market advice while containment and records retrieval proceed. Investigation conclusions are product- and fact-specific.
8. Implement CAPA through controlled changes and effectiveness checks
CAPA means corrective and preventive action in common quality language, but the buyer should define the terms used in its own process. At minimum, distinguish: correction (fixing the detected unit or paperwork), corrective action (addressing the cause of a detected nonconformity), and preventive or risk-reduction action (reducing the chance of a potential issue). Do not allow a supplier to call a CAR “closed” merely because rework has been completed.
Every action should identify the affected process/document, revised control, training, effective date, approval, and whether it changes product configuration or evidence requirements. A change affecting safety, function, claims, marking, or market documentation may need technical and market review before shipment.
| CAPA stage | Buyer evidence to request | Closure test |
|---|---|---|
| Contain | Held-stock list, shipment status, lot/serial scope and interim control | Affected product cannot be released unintentionally |
| Diagnose | Investigation record, supporting data, stated cause and uncertainties | Explanation matches the observed facts and scope |
| Implement | Revised controlled document, process record, approval/training evidence | Change is in use on the specified effective date |
| Verify | Follow-up audit, targeted record sample, trend review, or defined retest | Pre-agreed effectiveness criterion is met or gap remains open |
| Learn | Supplier/brand risk review and recurrence controls | Similar process or SKU exposure has been considered |
Effectiveness verification is not a future-performance guarantee. Define sample, period, owner, and result; if evidence is insufficient, extend the check or reopen the action.
9. Connect factory records to shipment, returns, and market response
Connect production history to carton, pallet, container or shipment allocation, destination, importer/distributor, warehouse, retailer, and direct-to-consumer channel. Define data-sharing, privacy, and retrieval responsibilities.
The GS1 Global Traceability Standard describes an end-to-end model that spans transformation, transport, distribution, maintenance, and disposal, and says participants should be able at minimum to trace back to direct suppliers and forward to direct recipients [2]. For a buyer, a practical “one-up, one-down” drill is an achievable starting point: select a finished identifier, retrieve its relevant upstream evidence, and identify the direct downstream shipment recipients. Then test whether that result is usable for the actual channel mix.
For EU consumer products within scope, GPSR treats product traceability as fundamental to effective market surveillance and corrective measures [1]. The European Commission says Safety Gate enables information on measures against dangerous non-food products to circulate quickly among national product-safety authorities [6]. Do not infer from those systems that any particular issue requires an alert, withdrawal, or recall; those are fact-, risk-, and jurisdiction-dependent decisions. The buyer’s responsibility here is readiness to retrieve accurate data and to preserve a defensible chronology.
Use a hypothetical event in a tabletop exercise with the brand, supplier, importer, warehouse, customer-service owner, and channel contacts as appropriate. Reconcile records and totals, document missing links, and create CAPAs. The output is an improvement log, not a readiness declaration.
Image recommendations
- Insertion point: After Module 2.
Purpose: Show the link between product identifier, carton, and record. Caption: “A traceability system works when product, package, and production records can be reconciled.” ALT text: “Engineer scanning an appliance serial label beside carton and production record.” AI image prompt: “Photorealistic appliance quality station with unbranded product, neutral carton label, scanner, and generic production record; no logos or personal data.”
- Insertion point: Beside Module 4 audit table.
Purpose: Show an evidence-based line audit. Caption: “A line audit compares the controlled build with the process and records in use.” ALT text: “Quality auditor reviewing assembly controls beside an appliance production line.” AI image prompt: “Photorealistic factory audit: auditor in PPE checks work instruction, parts bins, and neutral appliance assembly line; no logos or certification claims.”
- Insertion point: Before Module 8 CAPA table.
Purpose: Visualize cross-functional corrective-action review. Caption: “Containment, evidence review, and effectiveness checks need clear ownership across the supply chain.” ALT text: “Team reviewing corrective-action workflow with appliance sample and records.” AI image prompt: “Photorealistic procurement, quality, and engineering meeting reviewing a generic corrective-action flowchart with unbranded appliance and folders; no company names.”
10. Use buyer checklists and FAQs to test the operating model
Before approving a supplier, revised platform, or release, test the operating model against a real SKU. Identify the information, authority, and actions available if an issue arises.
| Buyer checkpoint | Approval question |
|---|---|
| Product identity | Can the team distinguish model, revision, electrical variant, packaging/label revision, and relevant destination? |
| Identifier logic | Is each unit or lot tied to a documented, non-overlapping production scope? |
| Test evidence | Can the buyer retrieve the applicable small appliance test record and any linked exception/disposition? |
| Audit evidence | Has a recent line audit tested current documents, physical practice, and records rather than only facilities? |
| Escalation | Are stop-ship, hold, listing-pause, and external-advice decisions assigned to named roles? |
| CAPA | Does each action have containment, cause, controlled implementation, and effectiveness verification? |
| Distribution | Can the finished lot or serial range be reconciled to shipments, stock, and direct downstream recipients? |
| Change and market review | Does a material change trigger review of final configuration and destination-market evidence before release? |
Buyer FAQs
Is a serial number always better than a lot code for a small appliance? No. It helps only when records, customer-service capture, and shipment links remain complete. A tightly defined lot can be practical. Select the level that supports containment and after-sales decisions, then prove it through a trace exercise. Account for final configuration, sales route, and destination-market requirements [1][2].
Can a final inspection report serve as the complete small appliance test record? Usually not. The evidence route may also need controlled specifications, in-process controls, exceptions, rework/retest evidence, release authorization, and product/lot identity. Do not treat an inspection report for another model or revision as proof for the current SKU.
What should trigger a corrective action request instead of routine supplier feedback? A CAR is appropriate when a documented nonconformity, trend, evidence gap, or audit finding needs containment, investigation, action, and verified closure. Escalate potential safety, regulatory, or broad-distribution issues; internal classification is not qualified advice.
Does closing a CAPA mean the buyer has proved that the problem cannot recur? No. Closure means agreed actions and an effectiveness check were completed; it is not a future-outcome guarantee. Retain evidence, monitor trends, and reopen if facts challenge the cause, scope, or conclusion.
Who owns the records when the brand uses an OEM/ODM supplier? Allocate custody, access, retention, confidentiality, and retrieval in the contract and operating model; statutory duties may still attach to market actors. The brand needs decision evidence while the supplier maintains controlled source records. UZYVO’s FAQ and factory-capabilities overview can frame sourcing discussions, not replace legal review.
11. Make quality data a controlled decision asset
Traceability, audits, and CAPA deliver value when they shorten the path from signal to proportionate action. The operating system connects final configuration to identifier, identifier to test and line evidence, evidence to shipment/channel data, and an issue to containment, investigation, approval, and effectiveness checks.
Set identifier precision, critical records, audit sampling, escalation authority, and closure standard before mass production. Rehearse retrieval using actual records and revise as SKU, supplier, channel, or market changes. This turns a small appliance test record, small appliance production line audit, and small appliance quality escalation matrix into decision tools rather than static files.
Ready to structure traceability, audit evidence, and CAPA ownership for an appliance program? Email UZYVO at info@uzyvo.com with the product type, target markets, and current project stage. We can discuss an OEM/ODM production-evidence workflow. Retain appropriately qualified advisers for market-specific legal, certification, safety, and regulatory determinations.
References
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com