Target Keywords: small appliance contract manufacturer; small appliance manufacturing partner; small appliance trading company vs manufacturer; small appliance factory capability; private label appliance supplier; custom appliance manufacturer; kitchen appliance OEM supplier
Direct answer: Do not classify a supplier from its website, product catalogue, price, or the word “factory” in its name. Ask the legal entity to map its role for the exact model and destination market, then reconcile that statement with the production site, bill of materials (BOM), sample records, test documentation, purchase-order flow, export paperwork, and change-control authority. A trading company can be a workable route when its role and controls are explicit; a direct manufacturer is credible only when it can evidence control of the proposed configuration and the production process.
The real question is who controls product risk after the purchase order? A buyer may contract with a plant owner, a contract assembler, a group exporter, or a trader managing independent factories. Each can be legitimate when its claimed role, contractual accountability, evidence, and operating controls align.
This guide addresses business-model verification and direct-manufacturing evidence, not general supplier selection. Requirements depend on the final configuration and destination market; obtain qualified legal, customs, testing, and regulatory advice where needed.
1. Define the question before asking “factory or trader?”
In sourcing, “manufacturer” can mean the site operator, the party controlling design and production, or the party treated as manufacturer for market access. These roles need not be held by one entity. A supplier may assemble a kettle using purchased modules, a group exporter may quote while a sister company produces, and a trader may coordinate an established plant. None is inherently disqualifying.
Start with a precise classification statement for the proposed SKU: model number, voltage/frequency, plug, destination, private-label artwork, accessories, packaging, and intended launch channel. Ask the supplier to select and explain one role below, naming every legal entity and site involved.
| Operating model | What it may mean | Evidence a buyer should request | Buyer control to clarify |
|---|---|---|---|
| Direct manufacturing entity | The contracting entity operates the proposed production site or directly controls production there. | Site registration, site address, process map, production records, equipment and personnel evidence. | Who approves process, supplier, BOM, and line changes? |
| Group export/contracting entity | A related company contracts or exports while an identified group site manufactures. | Group relationship, contract flow, manufacturing-site identity, document signatories. | Which entity is liable for quality, records, and corrective action? |
| Contract manufacturer | The entity produces to a defined buyer or brand specification, possibly using supplied or sourced components. | Controlled BOM, work instructions, traceability, incoming controls, change records. | Who owns design decisions and critical-source approval? |
| Trading or sourcing company | The entity coordinates one or more third-party plants and may provide commercial or technical services. | Disclosed factory list, signed production authority, inspection plan, supply-chain map. | Can it compel records, approve changes, and provide remedy? |
The phrase small appliance trading company vs manufacturer therefore describes a verification task, not a quality ranking. A transparent intermediary with defined authority can be safer than an opaque “factory.” Conversely, a plant visit is not sufficient if the visited site is not the one that will build the buyer’s configuration.
2. Map the legal entities and the product flow
Before reviewing machinery or samples, make a one-page entity-and-flow map. It should include the quoting entity, contracting party, payment beneficiary, design owner, tooling owner, production-site operator, test-report applicant, exporter of record where relevant, inspection provider, and post-sale escalation owner. Record registered names in local and Roman characters, addresses, registration numbers where available, and the names shown on invoices and bank instructions.
The purpose is reconciliation, not suspicion. A legitimate group structure can explain differences between the quotation header and export documents. The concern is an unexplained difference, a shifting payment beneficiary, or a supplier that will not identify the actual production site. Ask the candidate to explain discrepancies in writing and retain the explanation with the supplier file.
For EU product rules, the commercial word “manufacturer” is not decisive. The European Commission’s Blue Guide describes the manufacturer as the person responsible for designing or manufacturing a product and placing it on the market under its own name or trademark; it also explains that a party having a product made under its own name can bear manufacturer responsibilities.[1] The Commission similarly notes that an importer or distributor marketing under its own name takes on those responsibilities.[2] Those principles do not decide every product’s obligations, but they show why a private-label buyer should map brand and market roles separately from factory ownership.
In the supplier interview, establish who signs and invoices; who operates the site; whether an exporter is affiliated or independent; who approves components, firmware, and artwork; who holds retrievable lot records; and which entity can require site corrective action.
Do not treat business registration documents as proof of small appliance factory capability. They identify an entity, not its current ability to manufacture a particular appliance consistently. They are one link in an evidence chain.
3. Request a role declaration tied to the exact configuration
Request a short, signed role declaration naming every expected factory and material subcontractor, activities by location, and accountable engineering, quality, documentation, and change contacts. It must state whether the supplier operates the site, is a group entity, a contract manufacturer, or an intermediary.
Reject generic “manufacturer” language. Ask the supplier to map the route from receipt to shipment and distinguish, for example, housing moulding, PCB programming, heater or motor installation, testing, and packing. A kitchen appliance OEM supplier should explain what it performs, what it outsources, and how it controls each interface. Test the declaration with current work instructions, test-station records, calibration status, source approval, and a lot-traceability example. Failure to identify the real site or responsibility boundary is a material risk.
Control principle: Verify the route that will make your approved configuration, not a showroom model, a historical production line, or a certificate-holder’s unrelated product family.
NIST defines conformity assessment broadly as demonstrating that specified requirements are fulfilled, and lists tools that can include supplier declarations, sampling and testing, inspection, certification, and management-system assessment.[3] For buyers, that is a helpful reminder that no one artefact proves every part of a supplier claim. Combine representations, records, observation, and independent checks in proportion to the risk.
4. Test direct-manufacturing claims on site or remotely
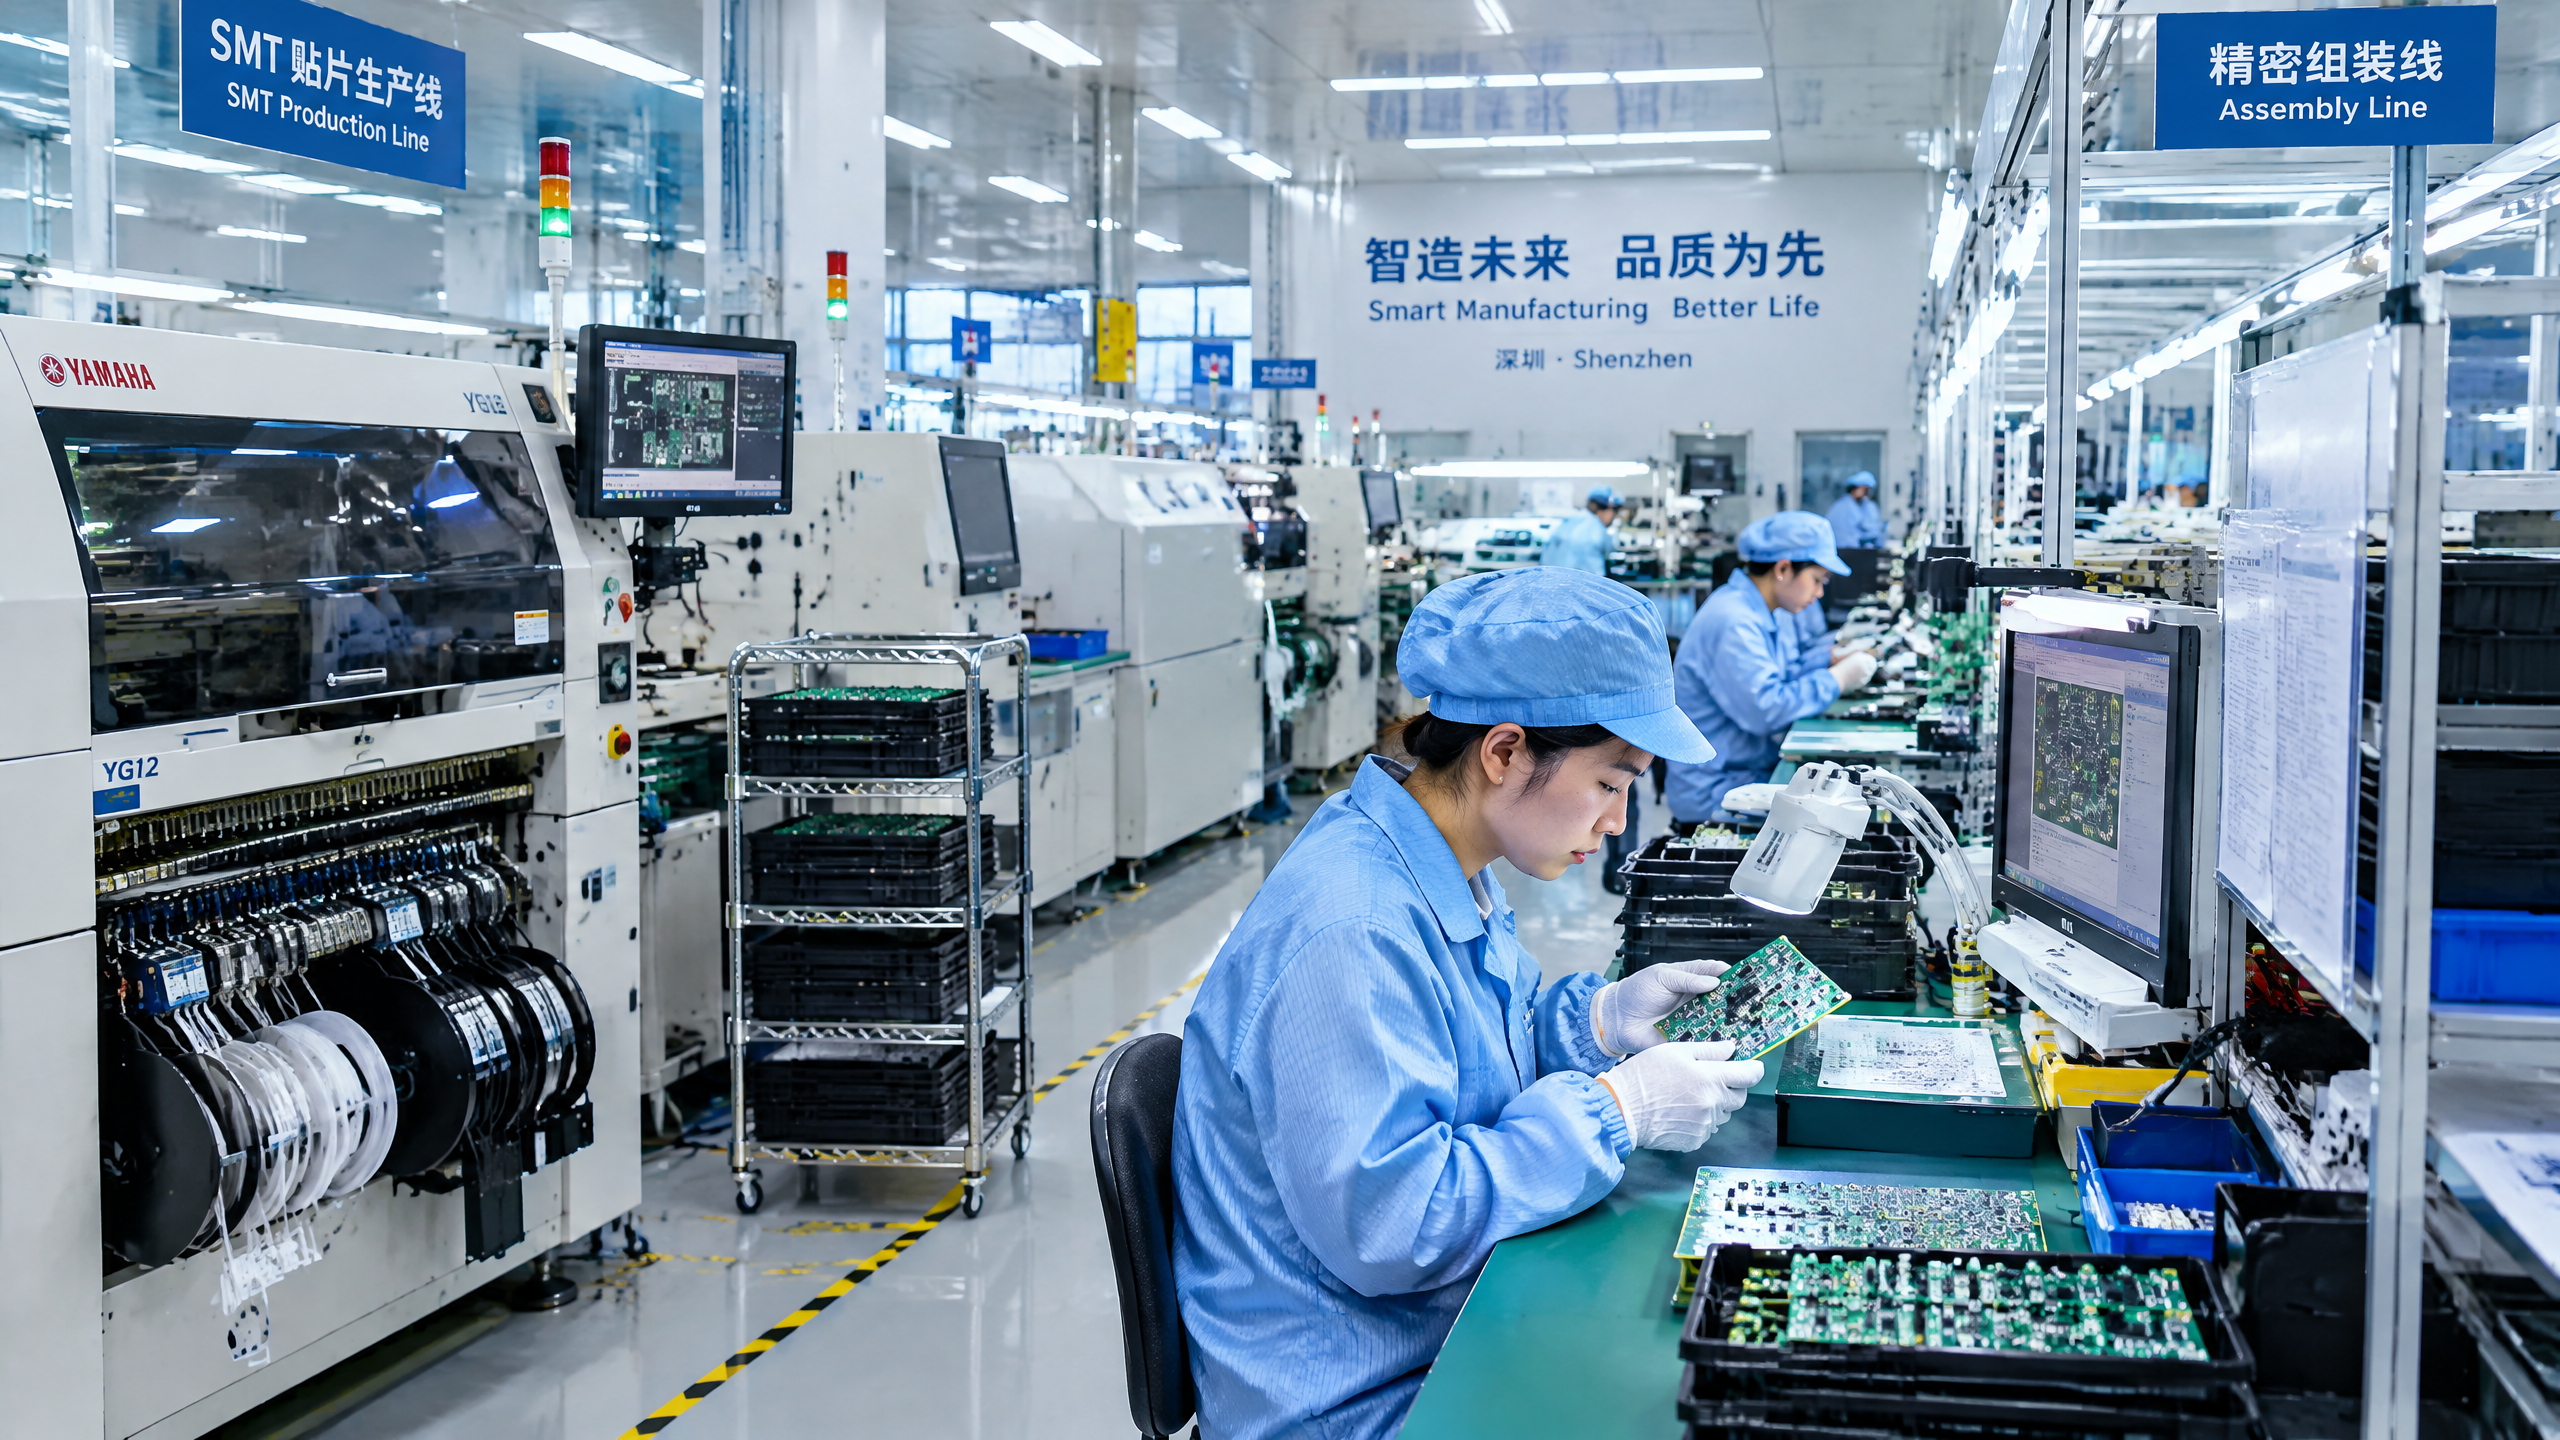
A site visit, properly scoped remote audit, or qualified third-party inspection can test whether the claimed production route is present and controlled. The objective is not to count machines or photograph a line; it is to follow the buyer’s intended product and compare what is observed against the declaration.
Before the review, send a focused agenda: the specified model or comparable architecture; expected process steps; critical parts; production status; traceability sample; change-control record; quality records; and any required documentation. If the final model is not running, inspect demonstrably comparable operations and label the limitation. Do not imply that a visit certifies future output.
| Verification point | Questions to ask | Evidence with higher decision value | Warning sign requiring explanation |
|---|---|---|---|
| Physical production route | Which operations occur here for this architecture? | Controlled flow, defined stations, work instructions matched to product. | The site cannot identify the requested model’s route. |
| Critical inputs | Where do heaters, motors, PCBs, cords, chargers, and safety-critical plastics originate? | Approved-source list, receiving checks, batch/lot link. | Parts are present without source or acceptance records. |
| Process control | What stops an incorrect part or setting reaching final assembly? | Fixtures, parameter records, error-proofing, disposition records. | Verbal assurances with no records or clear ownership. |
| Test and release | Which units or samples are tested, to what criteria, and who releases? | Dated test records, calibrated-equipment status, nonconformance flow. | A test station exists but output is not traceable. |
| Packing and shipment | How is approved artwork, manuals, and carton version controlled? | Revision-controlled packing specification and lot identity. | Finished goods mix with rejected or unlabelled stock. |
Photos and live video support, but do not prove, a claim. Select a lot record and trace it to incoming components and shipment or inspection records. Audit reports should identify the observed configuration, limitations, evidence reviewed, and corrective-action owner; they do not certify future production or universal market compliance.
Mid-article CTA: turn supplier claims into an evidence request
If you are mapping a direct factory, group exporter, or intermediary for a private-label project, email UZYVO’s team with the product category, target markets, configuration, and current supplier documents. We can help structure a configuration-led OEM/ODM discussion; final suitability remains subject to the agreed product, evidence, and destination-market review. You can also see the OEM/ODM workflow before building your evidence request.
5. Separate production control from a certificate folder
Certificates, test reports, and audit reports each answer a limited question. A management-system certificate does not prove that its scope covers the proposed site or controls; a test report may cover only a sample; and an inspection report describes only its sampled lot.
Verify issuer, entity, site, scope, dates, identifier, product description, ratings, standard edition, deviations, and SKU relevance. IAF CertSearch is a useful starting point for checking accredited certificates, but it does not replace scope review.[4] The IECEE CB Scheme supports mutual acceptance of relevant electrical and electronic test reports and certificates, yet a CB document is not blanket market approval for a private-label variant.[5] Compare the final configuration and destination market with qualified reviewers. Maintain a document index linking each claim to a controlled design revision.
6. Trace configuration control from sample to shipment
Evaluate a custom appliance manufacturer by its ability to control changes, not its willingness to add a logo or colour. Customisation can change materials, ratings, software, tooling, labels, instructions, and supporting evidence.
Before release, create a controlled configuration pack: variants and markets, drawings, BOM revision, critical-component specifications, artwork, instructions, packaging, approved sample, test plan, acceptance criteria, and approvers. Define changes requiring written approval.
| Change event | Why it can matter | Evidence or decision gate |
|---|---|---|
| Alternative motor, heater, charger, cord, PCB, or plastic | Can affect fit, performance, safety, and test applicability. | Engineering review, product-specific evidence assessment, written approval or rejection. |
| Production-site or line transfer | Can change process control, tooling, personnel, and traceability. | Site disclosure, process comparison, revised validation or inspection plan as appropriate. |
| Artwork, label, plug, or instruction update | Can affect market information, ratings, and user safety communication. | Market-specific review and revision-controlled artwork approval. |
| Firmware or connected-feature change | Can alter function, radio behaviour, privacy, or instructions. | Configuration record and applicable technical/market review. |
Under the EU Low Voltage Directive, for electrical equipment within its scope, manufacturers must prepare technical documentation, carry out the relevant conformity assessment, draw up the EU declaration of conformity and affix CE marking when conformity is demonstrated; they must also have procedures so series production remains in conformity.[6] The Directive also sets importer checks in its own scope, including verifying documentation and markings before placing equipment on the market.[6] Those are legal requirements with scope and product-specific conditions, not a contract template. They reinforce the commercial value of traceable design, document, and series-production controls.
Contractually define undocumented change as a nonconformance, with escalation, containment, evidence update, and remedy. Contract allocation should be reviewed for the relevant configuration and jurisdiction.
7. Evaluate the intermediary as an operating system, not a label
A private label appliance supplier that trades or sources may add value through coordination, inspection, consolidation, or export handling. It is not the factory if it does not operate the site.
Convert its role into controls: an approved factory list, approval rules for substitution, access to relevant records and sites, a defined inspection/release process, and one escalation owner. Confirm it can obtain original reports, component declarations, nonconformance data, and corrective-action evidence.
| If the intermediary says… | Ask this follow-up | Control worth documenting |
|---|---|---|
| “We have our own partner factory.” | Is it related, exclusive, or simply a current vendor? | Factory identity; production authorization; substitution prohibition. |
| “We handle quality.” | Who writes criteria, performs checks, and may stop shipment? | Inspection scope, release authority, report ownership, corrective-action timing. |
| “The factory has certificates.” | Which named site and scope cover this product route? | Source documents and independent verification route. |
| “We can develop your design.” | Who owns drawings, tooling, firmware, and test data? | IP, tooling, access, and change-control clauses. |
This does not mean every buyer must contract directly with a plant. It means the contracting route should match the desired visibility and remedy. For an explanation of how a product brief, samples, and production release can connect, see UZYVO’s factory capabilities. The evaluation should remain configuration-led rather than relying on a supplier category alone.
8. Use documents that cross-check one another
The strongest evidence is consistency across operational records: plant identity, product-specific BOM, purchase and production records, inspection report, carton marking, and export documents. Ask for records from a buyer-selected lot rather than relying on website language.
Build a cross-check matrix for the nomination file:
| Record | What it should corroborate | Reconcile against |
|---|---|---|
| Quotation and contract | Contracting scope, model, terms, accountable entity. | Invoice, payment beneficiary, purchase order. |
| Site and process map | Site identity and work actually performed. | Audit observation, production log, disclosed subcontractors. |
| BOM and drawings | Approved configuration and critical parts. | Sample, test record, incoming inspection, change log. |
| Test/inspection records | What was tested or inspected and for which lot. | Acceptance criteria, calibration evidence, shipment release. |
| Packing specification | Packaging, label, manual, and traceability version. | Finished-goods audit, artwork approval, export cartons. |
| Test or certification evidence | Product/variant, standards, applicant, laboratory, and limitations. | Current design revision, market applicability assessment. |
For regulated U.S. general-use consumer products, CPSC states that written certification must be based on testing or a reasonable testing programme and that the importer issues the GCC for overseas production.[7] This market-specific example shows why the responsible party needs configuration-relevant evidence. Require legible, dated, attributable records; where verification is impossible, record the item as unverified.
9. Score the business model with hard stops
A scorecard supports consistent comparison, but a commercial score cannot overcome a fundamental evidence gap. Separate scored considerations from release gates, with sourcing, engineering, quality, and market-access owners agreeing the weighting.
| Dimension | Illustrative evidence | Example decision treatment |
|---|---|---|
| Entity and role transparency | Signed role declaration; reconciled legal names and sites. | Hard stop if actual producer cannot be identified. |
| Configuration control | Controlled BOM, sample baseline, change process. | Hard stop if critical changes can occur without notice. |
| Direct manufacturing evidence | Product-relevant site/process review and traceability. | Score according to relevance and completeness. |
| Intermediary operating control | Factory authorization, records access, release authority. | Hard stop if intermediary cannot provide agreed visibility. |
| Documentation integrity | Verifiable, SKU-relevant source files and limitations. | Hard stop where required evidence is absent or misrepresented. |
| Commercial and programme fit | Communication, forecast process, contract terms, service model. | Scored; do not use to offset safety or legality concerns. |
Decide explicitly: approve, conditionally approve with defined closure, retain with extra intermediary controls, or do not proceed. Each condition needs an owner, evidence, due date, and re-verification. Once the production role is verified, use the OEM small-appliance manufacturer due-diligence framework for wider capability and control review.
10. Plan for exceptions, substitutions, and disputes
A factory, component, process, or responsible entity can change during a programme. The issue is not change itself but undisclosed substitution. Require advance written notice describing the reason, affected configuration and evidence, stock impact, validation needed, approver, and shipment status.
Retain the approved sample and revision pack. Align inspection to them, while recognising that sampling does not replace production control or regulatory assessment. Escalate through containment, root-cause analysis, corrective action, disposition, and evidence update. If a conformity-assessment body is relevant, verify its competence; the Commission’s NANDO listings identify notified bodies and their notified tasks.[8] Third-party involvement is not automatically required for every appliance or market.
11. Run the decision as a 30-day evidence sprint
Adapt this sequence to product maturity, evidence availability, and target market.
Days 1–5: freeze configuration and markets; collect the role declaration, entity map, factory list, and document index. Days 6–12: reconcile contract party, payment, site, BOM, sample, and test-document applicants. Days 13–20: trace a selected model or comparable route through receipt, assembly, testing, packing, and lot records. Days 21–25: have qualified people assess technical evidence and market roles for the final configuration. Days 26–30: put access, identity, change, inspection, remedy, and escalation controls into the release conditions or contract.
The outcome is a sourcing record showing who produces what, where, under whose control, and how variation will be governed—not a promise that change will never occur.
Buyer FAQs
Can a trading company be the right supplier for a private-label appliance?
Yes—if its role is explicit and it can deliver the access, records, factory disclosure, change control, and remedy the programme needs. Do not call it the manufacturer unless it operates or demonstrably controls the relevant production route. The right contracting choice depends on the final configuration, destination market, and the responsibilities the buyer intends to retain.
What is the quickest way to test a factory claim?
Ask for a signed role declaration and a buyer-selected lot trace. Reconcile the named entity and site with a controlled BOM, work instructions, input records, test or inspection record, packing specification, and shipment record. A visit or remote review adds value when it follows that evidence chain rather than merely viewing a production floor.
Is a test report enough to prove that the supplier manufactures the appliance?
No. A report may support a product assessment only for the configuration it describes. It generally does not establish who produced a later lot, whether the claimed site was used, or whether components and processes remained unchanged. Check the report applicant, product description, revision, critical components, date, and relation to the final configuration and destination market.
Conclusion: buy visibility and control, not a label
The useful distinction is whether the buyer can verify the production route and establish accountability for the exact configuration. A direct plant should evidence relevant manufacturing and change control; a group exporter should disclose its relationship; and a trader should disclose its factory network and provide matching access, authority, and records.
Test every claim against named entities, declared site, controlled configuration, traceable records, relevant documentation, and enforceable change rules. Revisit the evidence when the configuration, plant, component source, or destination market changes. That is a better basis for selecting a small appliance manufacturing partner than a catalogue claim.
Ready to turn a supplier claim into a configuration-led evidence request? Contact UZYVO by email with your category, target market, anticipated customization, and supplier structure. You may also review the buyer FAQ for OEM/ODM, sampling, quality, and shipping questions.
AI Image Recommendations
- Supplier-role evidence map
- Purpose: Make the entity, factory, and documentation relationships understandable at a glance.
- Insertion point: After Module 2.
- Caption: “Map the contracting entity, production site, and evidence owner before comparing quotations.”
- ALT text: “Diagram showing a brand, trading company, contract manufacturer, component suppliers, and document trail.”
- English AI image prompt: “Clean editorial B2B infographic, global small-appliance supply chain verification map: private-label brand, transparent trading company, contract manufacturing plant, component suppliers, inspection checkpoint, document folder trail; neutral blue and charcoal palette, clear generic labels, no logos, no numerical performance claims, professional procurement presentation style.”
- Configuration traceability review
- Purpose: Show that credible manufacturing proof joins components, records, and a finished appliance rather than relying on a building exterior.
- Insertion point: After Module 6.
- Caption: “Configuration control links the approved BOM, production record, test result, and finished lot.”
- ALT text: “Quality engineer comparing appliance components, a controlled bill of materials, and a finished countertop appliance.”
- English AI image prompt: “Photorealistic documentary editorial scene in a small-home-appliance factory: quality engineer with unbranded countertop appliance, component bins with generic lot labels, paper and tablet BOM records, functional-test station in background, natural industrial lighting, no brand logos, no readable confidential data, realistic manufacturing environment.”
- Buyer-factory verification meeting
- Purpose: Support the 30-day evidence-sprint checklist with a collaborative, technical procurement visual.
- Insertion point: Before the conclusion.
- Caption: “A productive verification review tests records and responsibilities against the proposed product route.”
- ALT text: “Procurement buyer and factory engineering team reviewing a supplier verification checklist in a meeting room.”
- English AI image prompt: “Professional editorial photo of diverse procurement buyer, factory engineer, and quality manager reviewing an unbranded supplier verification checklist and process map at a meeting table beside a small appliance prototype, credible technical atmosphere, no logos, no visible company names, balanced natural lighting.”
References
Put the buyer guide into a practical sourcing path.
Bring this framework into your next product brief.
Share your target market, appliance category, annual volume, and launch window. We will discuss a practical sample, documentation, and production path for the final configuration.
Email info@uzyvo.com